With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Sugar powder conveying is a critical process in the food and chemical industries, where efficient and reliable transport of granular sugar is essential for maintaining production efficiency and product quality. The principles behind sugar powder conveying involve understanding the physical properties of sugar, such as its particle size, moisture content, and flow characteristics, as well as the mechanical forces required to move the material through pipelines or other conveying equipment. At Shandong HeadPowder Engineering Co., Ltd., we specialize in designing and manufacturing advanced sugar powder conveying solutions tailored to the unique demands of the sugar processing sector.
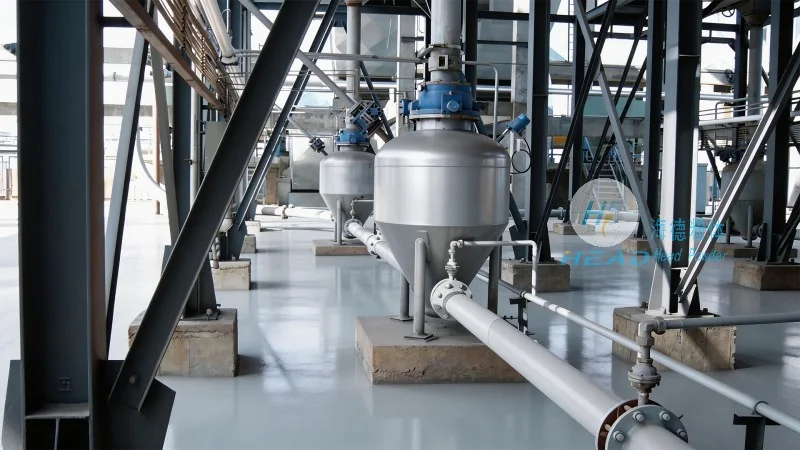
The fundamental principle of sugar powder conveying is to create a consistent flow of material by overcoming the forces of gravity and friction. This is typically achieved through positive displacement methods, such as rotary airlock valves, pneumatic conveying systems, or mechanical screw conveyors. In pneumatic conveying, for example, air is used to create a pressure differential that propels the sugar particles through a pipeline. The design of the conveying system must account for factors like the sugar's bulk density, which can vary based on moisture levels and particle size, as well as the required conveying distance and throughput. Our engineers at HeadPowder leverage decades of experience to optimize these parameters, ensuring that the system operates with minimal energy consumption and maximum efficiency.
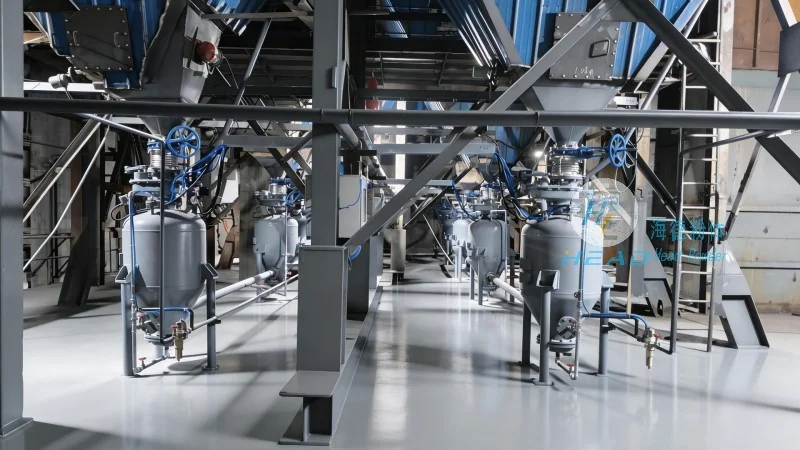
The working scene characteristics of sugar powder conveying systems vary significantly based on the application and scale of the operation. For large-scale sugar refineries, continuous high-capacity conveying is essential to maintain a steady supply of raw material to the processing units. In such scenarios, systems may include multiple stages of conveying, such as initial bulk handling via bucket elevators or belt conveyors, followed by pneumatic transport to storage silos or processing lines. The characteristics of the working environment, including temperature and humidity, also play a role in the choice of conveying method. For instance, in tropical climates where sugar may have higher moisture content, systems may incorporate drying or conditioning steps before conveying to prevent caking or blockages. Additionally, the need for hygienic and food-grade equipment is paramount in the food industry, requiring materials like stainless steel and sealed components to prevent contamination. HeadPowder's solutions are designed to meet these stringent requirements, ensuring compliance with industry standards and regulations.
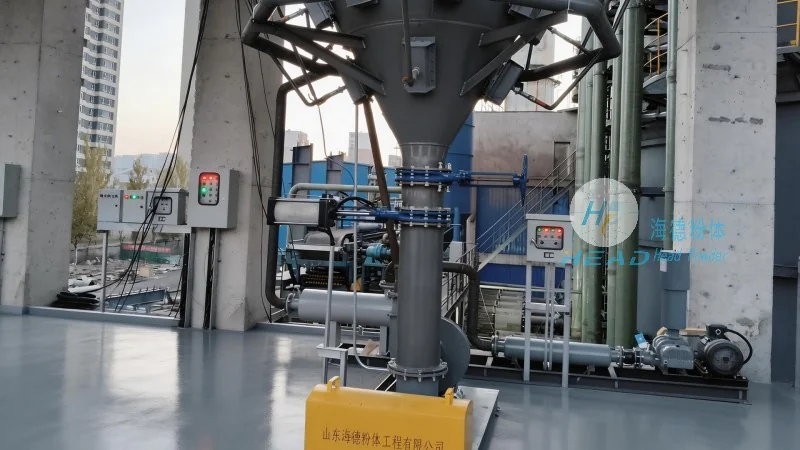
HeadPowder Engineering Co., Ltd. offers a range of advanced sugar powder conveying systems that incorporate cutting-edge technology and robust engineering. Our products are engineered to handle the unique challenges of sugar powder, including its tendency to form agglomerates or clog equipment. Key features include: self-cleaning rotary airlock valves that prevent material buildup and ensure smooth flow; high-efficiency pneumatic conveying lines optimized for low pressure and energy consumption; and modular design that allows for easy integration into existing production lines. Each system is customized to the client's specific requirements, taking into account factors like the type of sugar (e.g., white sugar, brown sugar, or raw sugar), the desired conveying capacity, and the distance between source and destination. Our team of experts works closely with clients to develop solutions that not only meet current needs but also provide scalability for future expansion.
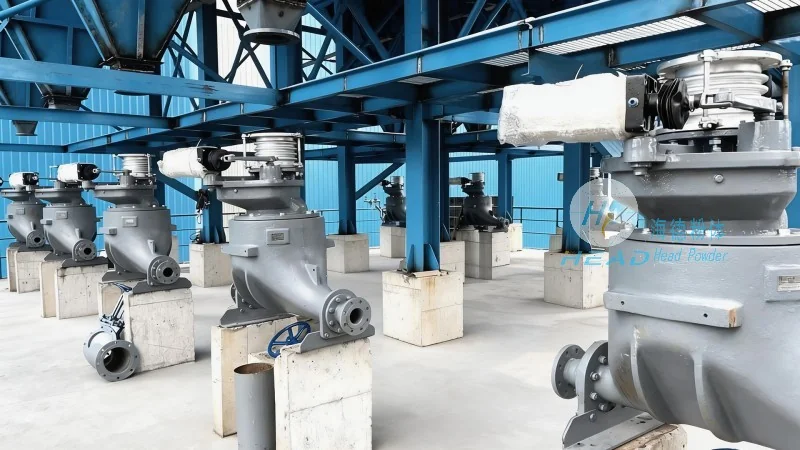
HeadPowder's sugar powder conveying systems have been successfully implemented in various industrial settings across China and beyond. For example, a major sugar refinery in Shandong Province utilized our pneumatic conveying system to transport raw sugar from storage silos to the refining plant, achieving a 20% reduction in energy consumption compared to traditional methods. Another client, a food processing company, implemented our mechanical screw conveyor system to handle brown sugar for candy production, improving product consistency and reducing downtime due to clogging. These case studies highlight the effectiveness of our solutions in addressing real-world challenges and enhancing operational efficiency. By focusing on the specific needs of each application, we ensure that our clients achieve optimal performance and reliability in their sugar powder conveying processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top