With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider of industrial material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. This article delves into the fundamental principles of sintered ash pneumatic conveying systems and explores the key characteristics of their operational environments. By understanding these aspects, industries can optimize material transport processes, enhance efficiency, and ensure compliance with safety and environmental standards.
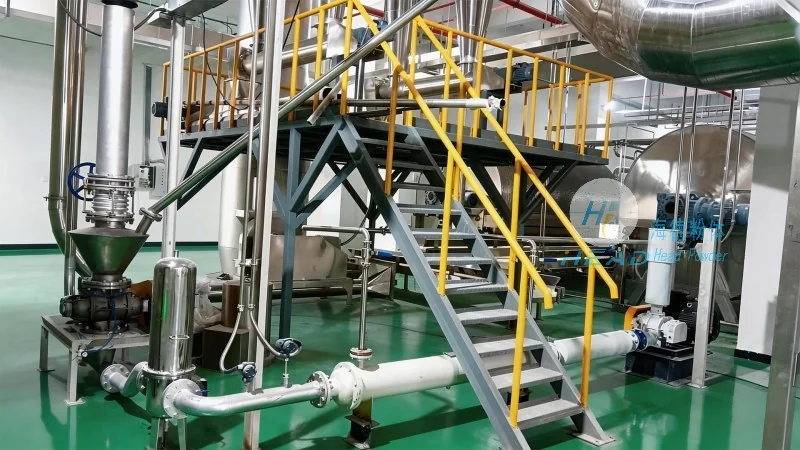
Sintered ash, a byproduct of the sintering process in steel production, requires efficient and reliable transport methods to move it from production sites to disposal or recycling facilities. Pneumatic conveying systems offer a versatile solution for handling such materials, leveraging compressed air or gas to transport powders and fine particles through pipelines. The sintered ash pneumatic conveying system, in particular, is engineered to address the unique challenges posed by this material, including its abrasive nature, dust generation, and varying particle sizes.
The core principle of pneumatic conveying involves the use of a pressure differential to move material through a closed system. In the case of sintered ash systems, the process typically starts with the material being fed into a hopper or feeder. From there, it is introduced into a pipeline where compressed air is introduced at a controlled rate. The air and material mixture travels through the pipeline, with the air providing the necessary force to transport the ash particles. The system may use either positive pressure (where air is pushed through the system) or negative pressure (where air is drawn out), depending on the specific application and layout. The design of the system, including the type of air nozzles, pipeline diameter, and velocity, is critical to ensuring efficient and low-pressure drop transport. HeadPowder's expertise lies in optimizing these parameters to minimize energy consumption and maximize material throughput.
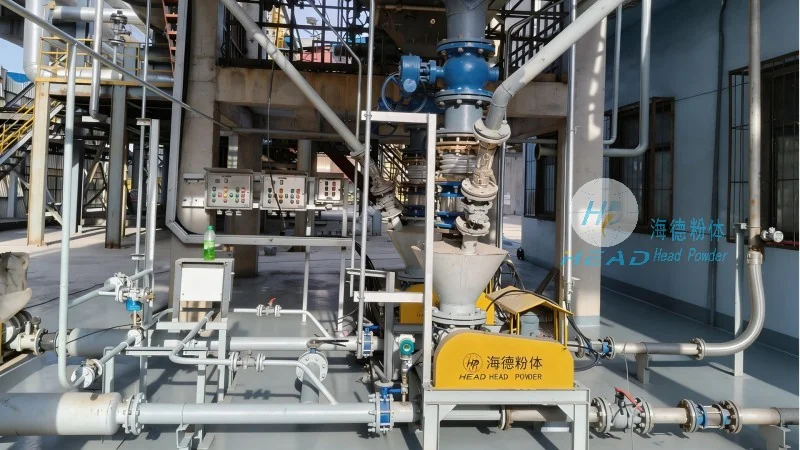
A sintered ash pneumatic conveying system comprises several essential components that work in tandem to ensure smooth operation. These include: (1) Hoppers and feeders, which store and meter the sintered ash into the system; (2) Air compressors or vacuum pumps, which generate the necessary pressure or vacuum; (3) Conveying pipelines, which transport the material; (4) Control valves and regulators, which manage air flow and pressure; (5) Filters and dust collectors, which capture and remove fine particles to prevent contamination and maintain air quality; and (6) Discharge units, which deliver the material to its final destination. Each component is carefully selected and integrated to meet the specific requirements of the sintered ash material and the operational environment.
The operational environment of a sintered ash pneumatic conveying system is typically found in industrial settings, such as steel mills, power plants, and waste management facilities. These environments are characterized by high material volumes, demanding operational conditions, and the need for robust, reliable equipment. The system is designed to handle large quantities of sintered ash, often at high flow rates, while maintaining consistent performance. The working scene also includes considerations for space constraints, as the system may need to navigate complex layouts within industrial facilities. Additionally, the system must be compatible with existing infrastructure, such as existing pipelines or buildings, to minimize installation costs and downtime. HeadPowder's systems are tailored to these specific working environments, ensuring seamless integration and optimal performance.
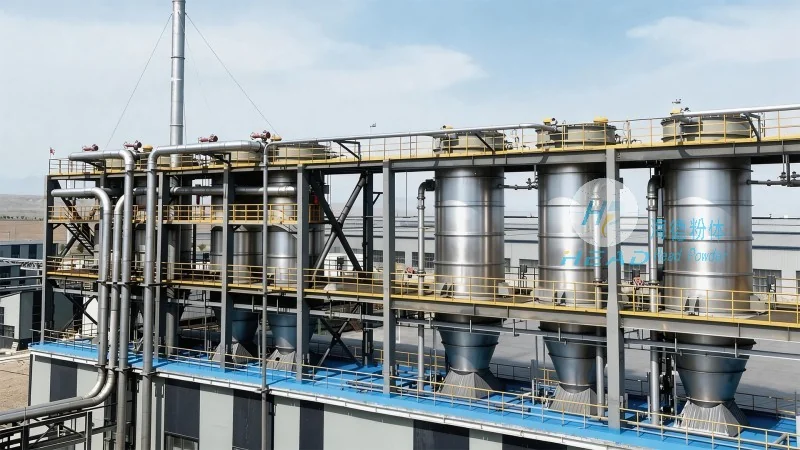
Implementing a sintered ash pneumatic conveying system offers numerous advantages for industrial operations. These include: (1) Reduced labor costs, as automated systems minimize the need for manual handling; (2) Improved safety, as the enclosed system prevents dust exposure and reduces the risk of accidents; (3) Enhanced efficiency, with continuous material flow and minimal downtime; (4) Lower energy consumption compared to traditional methods like belt conveyors; and (5) Environmental benefits, as the system helps control dust emissions and reduces the risk of material spillage. These advantages make sintered ash pneumatic conveying systems a preferred choice for industries seeking to optimize their material handling processes.
Understanding the principles and characteristics of sintered ash pneumatic conveying systems is crucial for industries seeking to enhance their material handling capabilities. HeadPowder, with its expertise in engineering and manufacturing, provides comprehensive solutions tailored to the unique needs of sintered ash transport. By leveraging advanced technology and careful system design, HeadPowder's systems ensure efficient, reliable, and safe transport of sintered ash, contributing to improved operational performance and environmental compliance. For industries in China, particularly in the Shandong region, HeadPowder offers a trusted partner in optimizing their material handling processes, supporting their growth and sustainability goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top