With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Quantitative weighing pneumatic conveying systems represent a sophisticated technology in material handling, combining the principles of pneumatic transport with precise weight measurement capabilities. These systems are designed to transport bulk materials efficiently while ensuring accurate and controlled dosing, making them indispensable in various industrial applications.
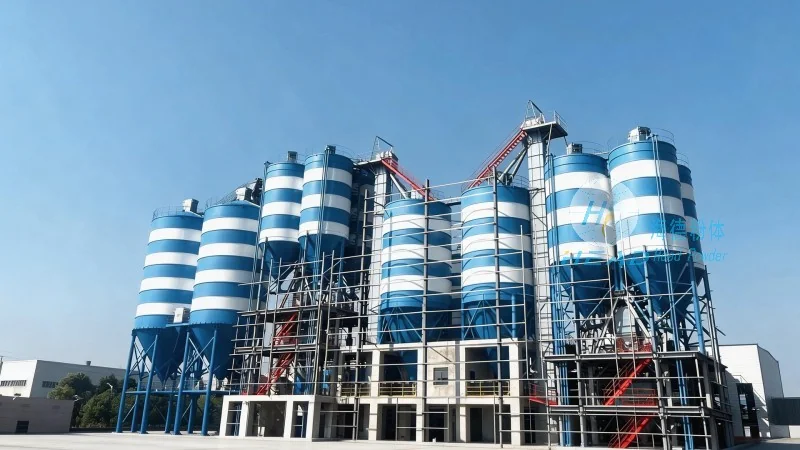
The core principle of quantitative weighing pneumatic conveying systems revolves around the use of air as the conveying medium to transport bulk materials from one location to another. The system typically operates by creating a pressure differential, often through a blower or fan, which generates airflow to move the material through a pipeline. Simultaneously, a weighing hopper or scale is integrated into the system to measure the mass of the material being conveyed in real-time. This integration allows for precise control over the quantity of material being transported, ensuring consistent and accurate dosing. The system can be categorized into two main types: positive pressure and negative pressure systems, each with distinct operational characteristics and applications.
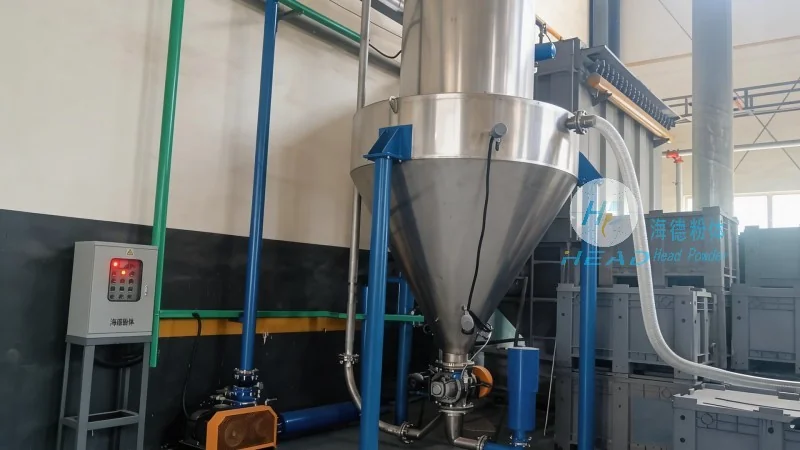
The working scene characteristics of quantitative weighing pneumatic conveying systems are highly adaptable to diverse industrial environments. They are commonly employed in sectors such as chemical processing, food and beverage manufacturing, pharmaceutical production, and mining, where the handling of powders, granules, or fine particles requires both efficiency and precision. In chemical plants, these systems are used to transport raw materials like powders and granules to reactors or storage tanks, ensuring that the exact amount of material is delivered for chemical reactions. In food processing facilities, the systems are crucial for handling ingredients like flour, sugar, and spices, maintaining hygiene standards and preventing contamination while delivering precise quantities for product formulation. The adaptability of these systems also makes them suitable for applications in the pharmaceutical industry, where the handling of active pharmaceutical ingredients (APIs) and excipients demands strict control over material flow and dosage. Additionally, in mining operations, quantitative weighing pneumatic conveying systems are utilized to transport ore or other mineral powders from processing plants to storage or shipping facilities, optimizing material handling processes and reducing operational costs.
Quantitative weighing pneumatic conveying systems offer several key features and advantages that make them preferred solutions in industrial material handling. One of the primary advantages is the ability to achieve high material throughput while maintaining precise control over the quantity of material being conveyed. This is particularly beneficial in processes where consistent dosing is critical, such as in batching operations or continuous production lines. The systems also provide flexibility in terms of material handling, as they can transport a wide range of materials, including powders, granules, and fine particles, without the need for additional equipment like conveyors or elevators. Another significant advantage is the reduced risk of material contamination and degradation, as the enclosed pipeline system minimizes exposure to external factors. Furthermore, these systems are energy-efficient compared to traditional mechanical conveying methods, as they utilize air as the primary power source, reducing operational costs and environmental impact. The integration of weighing technology ensures real-time monitoring and control, allowing operators to adjust the system parameters dynamically based on production requirements.
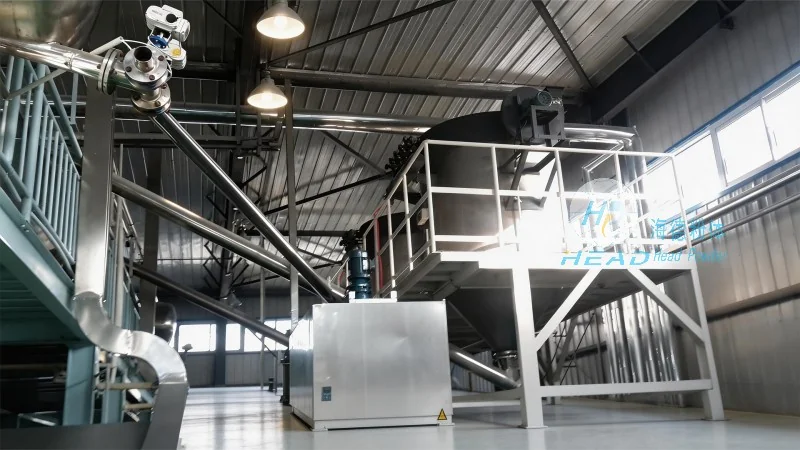
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of quantitative weighing pneumatic conveying systems and related industrial equipment. With a strong commitment to innovation and quality, the company specializes in designing, manufacturing, and installing advanced material handling solutions tailored to the specific needs of various industries. Headpowder's products are engineered to meet international standards and are known for their reliability, efficiency, and durability. The company's headquarters is located in Shandong, China, where it has established a robust research and development team focused on developing cutting-edge technologies in pneumatic conveying systems. Headpowder's expertise in quantitative weighing technology has enabled it to serve a wide range of clients across different sectors, providing customized solutions that enhance operational efficiency and productivity. The company's dedication to customer satisfaction and technical excellence has positioned it as a trusted partner in the global material handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top