With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Red sugar, known for its rich flavor and granular texture, presents unique logistical hurdles in industrial settings. Unlike standard granulated sugar, red sugar often contains higher moisture content and specific crystalline structures that make it prone to clogging, clumping, and dust generation. Traditional mechanical conveying methods, such as belt conveyors or screw conveyors, can often damage the delicate crystals or fail to handle the sticky nature of the material effectively. Furthermore, dust control is a critical concern in food processing facilities, as airborne particles can compromise hygiene standards and create safety hazards. Therefore, selecting an efficient and hygienic method for red sugar transportation is essential for maintaining product quality and operational safety.

To address these challenges, modern facilities are increasingly turning to red sugar pneumatic transportation systems. This technology utilizes the power of air pressure or vacuum to move the material through a closed pipeline network. Unlike bulk bag dumpers or rotary valves, pneumatic systems offer a completely enclosed environment, eliminating the risk of external contamination. The process involves feeding the red sugar into a feeder system, which then introduces the material into the pipeline where it is carried by the airflow to its destination. This method is particularly effective for handling fine powders and granules, ensuring a smooth and consistent flow without the physical wear and tear associated with mechanical parts.
A robust material transport system is built upon several critical components working in harmony. The primary unit is the feeder, which controls the rate at which the red sugar enters the pipeline. This is often followed by a filter system that removes dust from the exhaust air, ensuring the environment remains clean. The pipeline network is designed with specific diameters and angles to prevent blockages, while the vacuum or pressure source—typically a high-efficiency blower or compressor—provides the necessary energy to move the material over long distances. By integrating these components, the system ensures that the red sugar transportation process is both reliable and energy-efficient.
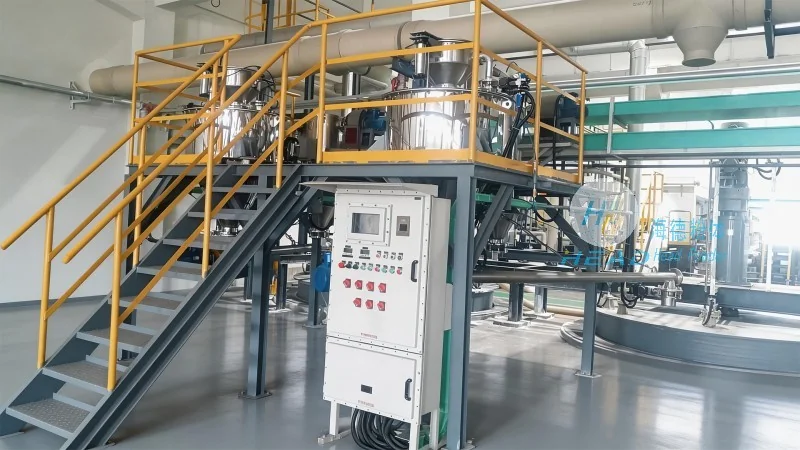
The adoption of pneumatic conveying technology offers numerous benefits that extend beyond simple movement. One of the most significant advantages is the reduction of cross-contamination. Since the system is sealed, there is no exposure to ambient air, which is vital for food-grade applications. Additionally, pneumatic systems are highly versatile; they can transport the material vertically, horizontally, or around corners with minimal complexity. This flexibility allows for more efficient plant layouts. For red sugar pneumatic transportation, this means that the delicate sugar can be moved from storage silos to packaging machines without the risk of spillage or degradation, preserving the product's integrity from start to finish.
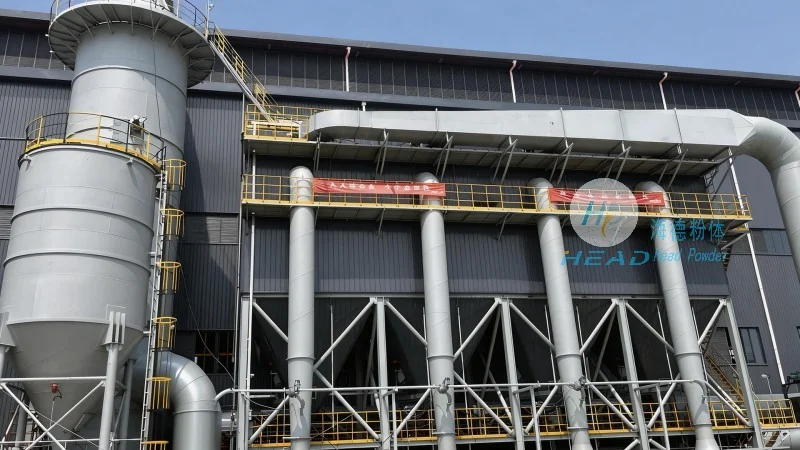
When considering a solution for material transport, the expertise of the engineering team is paramount. Shandong Headpowder Engineering Co., Ltd. specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the specific needs of the food industry. Our team understands the nuances of handling sensitive ingredients like red sugar. We utilize high-grade materials and precision engineering to ensure our equipment meets stringent hygiene standards. By choosing Headpowder, you are partnering with a provider that prioritizes durability, efficiency, and the preservation of your product's quality.
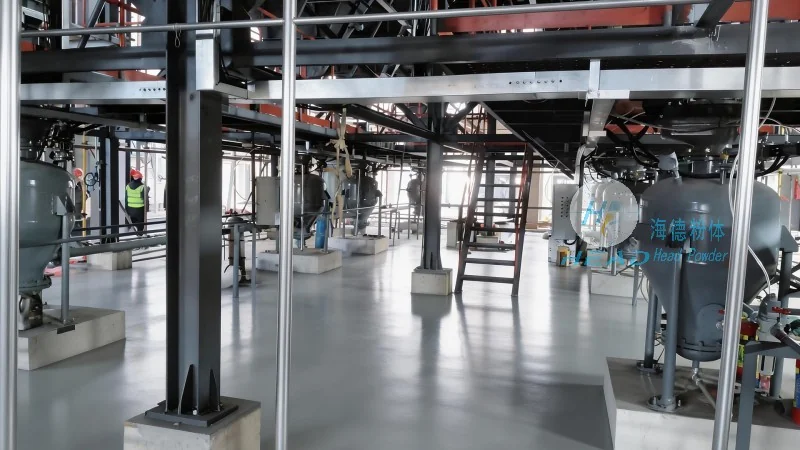
No two production lines are exactly alike, and a one-size-fits-all approach rarely works in industrial material handling. At Shandong Headpowder Engineering Co., Ltd., we pride ourselves on offering customized solutions for red sugar transportation. Our engineers conduct thorough site assessments to understand the specific constraints and requirements of your facility. Whether you need a system that integrates seamlessly with existing machinery or a completely new setup designed for high-capacity production, we provide a tailored approach. Our goal is to optimize your workflow, reduce downtime, and enhance the overall efficiency of your material transport operations.
Investing in the right conveying technology is a crucial step for any food processing facility. If you are looking for a reliable partner to upgrade your red sugar transportation capabilities, please do not hesitate to reach out. You can contact our sales team directly. Please reach out to Zhang Manager for detailed consultation and technical support. You can contact him via WeChat at 15662777102. Located in Shandong, China, Shandong Headpowder Engineering Co., Ltd. is ready to assist you in achieving seamless and efficient material handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top