

Working Principle and Features of Corn Cobs Powder Pneumatic Conveying Equipment
For industries dealing with corn cobs and other fine powders, efficient material handling is crucial. The corn cobs powder pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. offers a reliable solution to transport these materials with precision and minimal loss. This article explores the working principle and key features of this equipment, highlighting its benefits for various industrial applications.
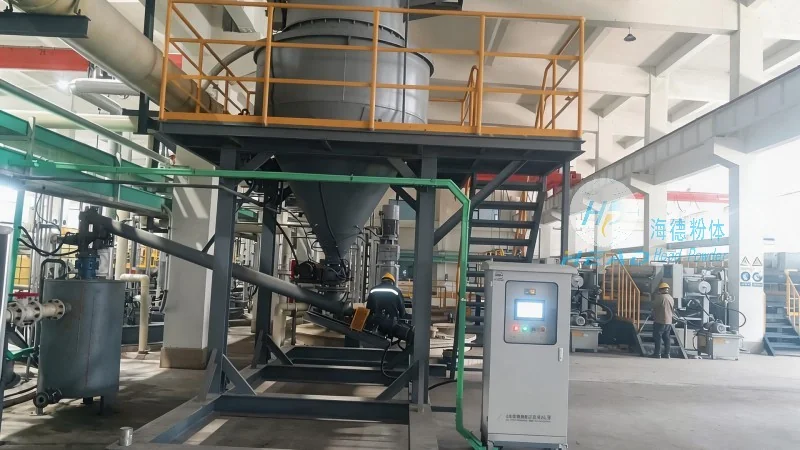
Overview of Corn Cobs Powder Pneumatic Conveying Equipment
The corn cobs powder pneumatic conveying system is designed to handle the transportation of corn cobs, which are often processed into fine powders for use in animal feed, biofuels, or other industrial products. Unlike traditional mechanical conveyors, this equipment uses compressed air to move the material through a pipeline network. This method reduces the risk of material degradation and contamination, making it ideal for sensitive applications.
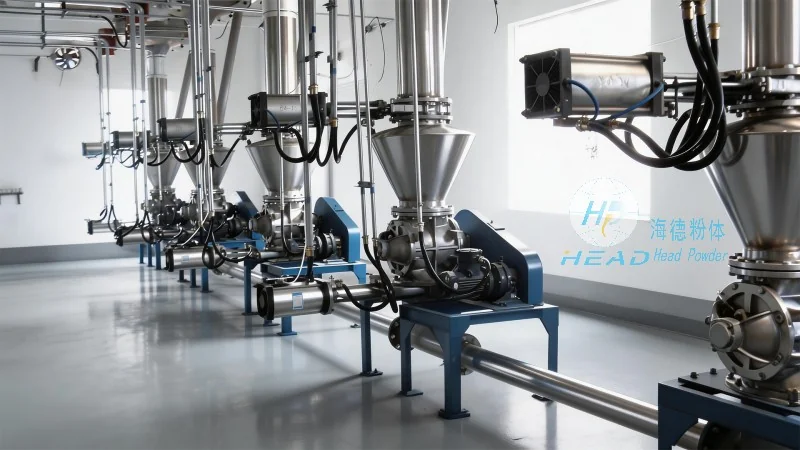
Working Principle of the Pneumatic Conveying System
The core of the corn cobs powder pneumatic conveying equipment is its ability to use air pressure to transport the material. The system typically consists of a hopper for material storage, a blower or compressor to generate the necessary air pressure, and a pipeline system that connects the source and destination points. When the material is released from the hopper, it is drawn into the pipeline by the moving air, which carries it to the desired location. The process is controlled by a series of valves and sensors that ensure the material is conveyed at the optimal speed and pressure.
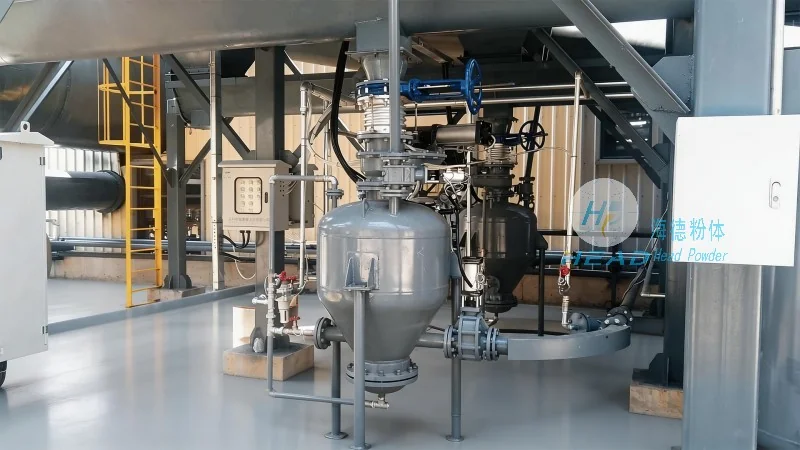
Key Features and Advantages
One of the primary advantages of this equipment is its ability to handle fine powders without causing dust or clogging. The design incorporates features such as self-cleaning pipelines and adjustable air flow controls, which help maintain consistent performance over time. Additionally, the system is energy-efficient, as it uses less power compared to traditional conveyor systems while achieving higher throughput rates. The equipment also offers flexibility in terms of layout, allowing it to be adapted to different plant configurations without major modifications.
Application in Industrial Settings
The corn cobs powder pneumatic conveying equipment is widely used in the agricultural and food processing industries. For example, in animal feed production, it efficiently transports corn cobs from storage silos to processing units, ensuring a steady supply of raw material. In biofuel plants, the system helps move the processed powder to storage tanks or reactors, improving operational efficiency. The equipment's ability to handle large volumes of material at a time makes it suitable for high-demand production lines, where reliability and consistency are paramount.
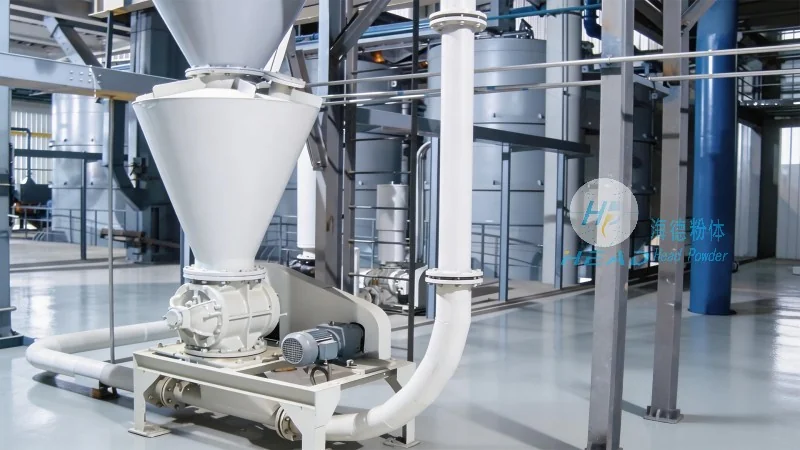
Conclusion and Company Information
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced pneumatic conveying solutions tailored to the needs of industries dealing with corn cobs and other fine powders. The company's equipment is designed to meet the highest standards of efficiency, durability, and safety. With its headquarters in Shandong, China, HeadPowder offers comprehensive support, including installation, maintenance, and technical assistance, to ensure that clients can maximize the performance of their material handling systems. By leveraging the principles of pneumatic transport, this equipment provides a cost-effective and reliable solution for moving corn cobs powder, contributing to improved productivity and reduced operational costs in various industrial applications.