With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
The Biological Enzyme Material Handling System is a specialized piece of equipment engineered for the efficient and precise transport of materials that involve biological enzymes. This system is designed to handle the unique properties of enzyme-based substances, ensuring optimal performance while preserving the integrity of the biological components. As a critical component in industrial processes that rely on enzymatic reactions, this system plays a vital role in enhancing productivity and operational efficiency.
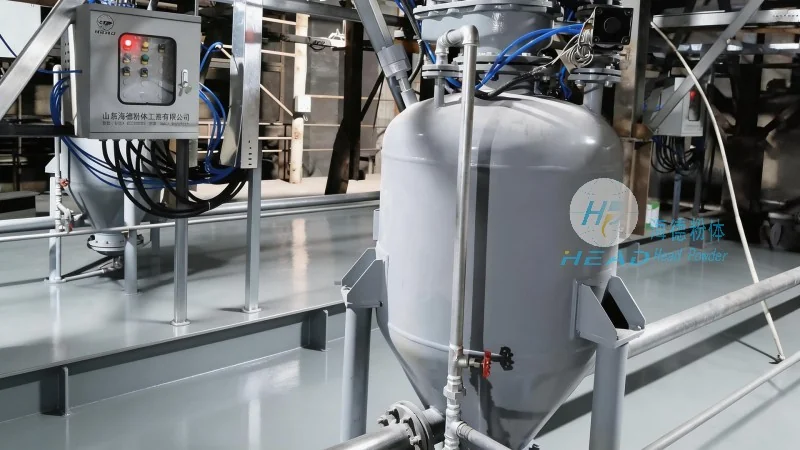
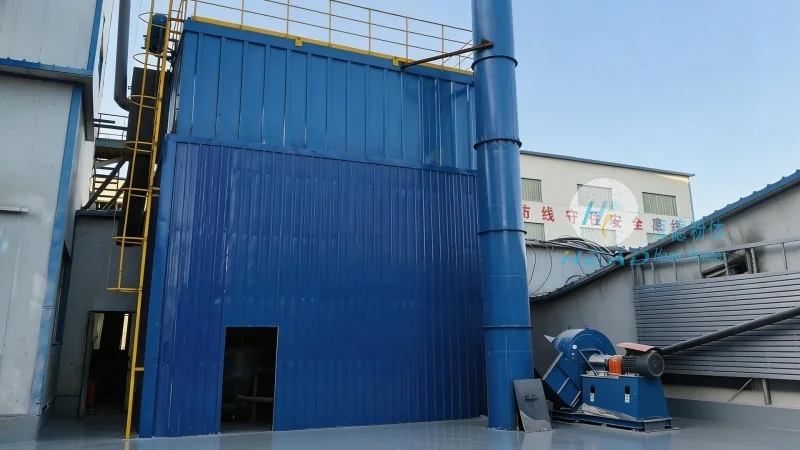
The core of the Biological Enzyme Material Handling System lies in its advanced mechanism that facilitates the seamless movement of enzyme-containing materials. The system operates through a combination of controlled flow mechanisms, temperature regulation, and precise dosing systems. These elements work in tandem to ensure that the enzymes are not denatured or degraded during transport. The system employs a closed-loop design to minimize exposure to external contaminants, which is crucial for maintaining the effectiveness of the biological enzymes. Additionally, the equipment is equipped with sensors and monitoring systems that provide real-time data on the material's condition, allowing for immediate adjustments to maintain optimal performance. The pumps are equipped with variable speed drives, enabling precise control over the flow rate to stabilize enzyme solutions. Temperature control units regulate the material's temperature, preventing thermal degradation. A filtration system removes particulate matter or contaminants, ensuring material purity. A central control system integrates sensor data, offering operators real-time insights into system performance and material condition.
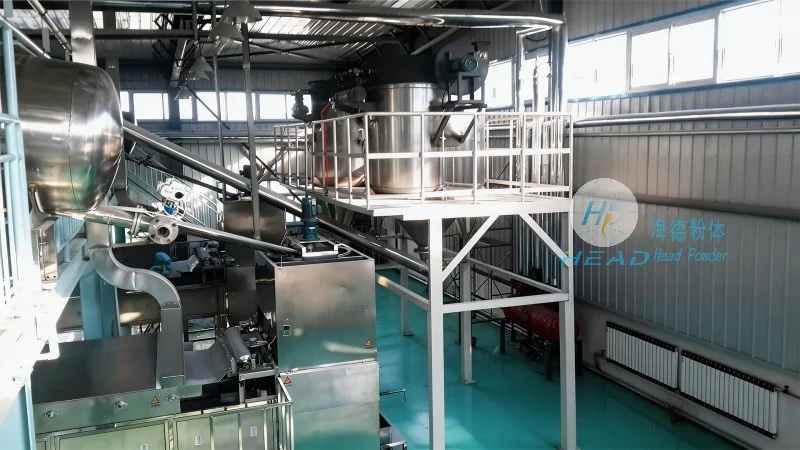
Several distinctive features set the Biological Enzyme Material Handling System apart from conventional material handling equipment. Firstly, its hygienic and sanitary design ensures easy cleaning and sanitization, essential for biological material applications. The system is constructed from corrosion-resistant and chemically inert materials like stainless steel and food-grade plastics, providing durability and maintaining material purity. Another notable feature is its adjustable speed and flow control, allowing customization of the transport process to meet specific enzyme material requirements. The system incorporates safety features such as overfill protection and emergency stop mechanisms, ensuring operational safety in industrial settings. Its compact design makes it suitable for integration into existing production lines without significant modifications, enhancing flexibility and adaptability.
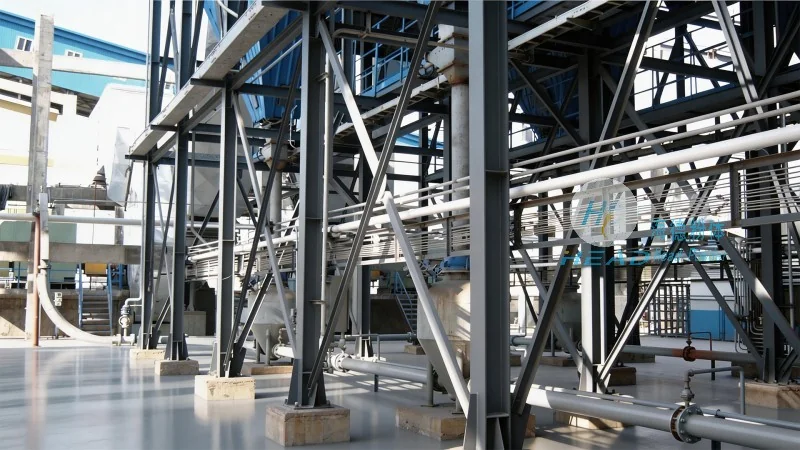
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the development and production of advanced material handling systems. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industrial sector, particularly in applications requiring precision and reliability. HeadPowder's commitment to research and development has enabled the company to create cutting-edge solutions that meet the evolving needs of its clients. The company's facilities, located in Shandong, China, are equipped with state-of-the-art technology and skilled personnel, ensuring that each product is manufactured to the highest standards. HeadPowder's team of experts works closely with clients to understand their specific requirements and provide tailored solutions that enhance operational efficiency and productivity. The company adheres to international quality standards and rigorous testing procedures, ensuring product reliability and durability. HeadPowder's customer-centric approach has earned it a strong reputation in the market, with clients relying on its expertise for efficient and dependable solutions. Continuous investment in research and development keeps HeadPowder at the forefront of technological advancements, delivering innovative and effective material handling systems to meet diverse industrial needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top