With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Bin pumps are essential equipment in modern industrial material handling systems, designed to transport bulk materials efficiently over long distances with high accuracy and reliability. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced bin pump solutions tailored to diverse industrial applications. This article explores the fundamental working principle of bin pumps and highlights their key characteristics that make them indispensable in various sectors.
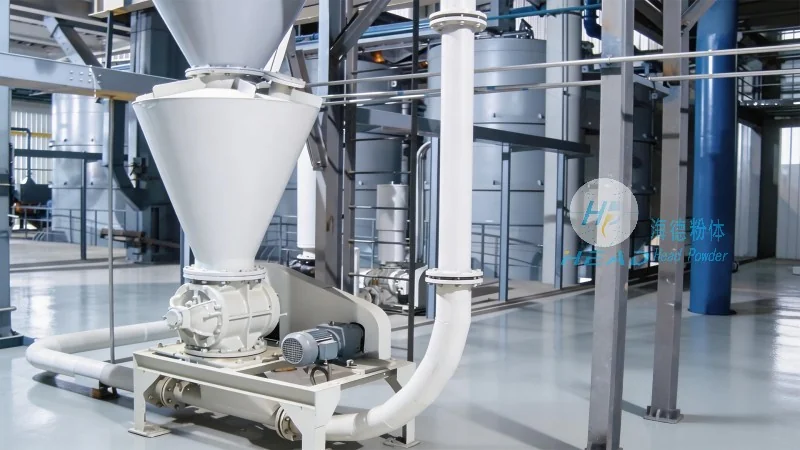
The core operation of a bin pump involves a series of coordinated actions to move bulk materials from a storage bin or hopper to the discharge point. The process typically begins with the material being fed into the pump's hopper. As the material accumulates, it creates pressure that triggers the pump's internal mechanism. In most bin pumps, this mechanism includes a diaphragm or piston that alternately compresses and expands, creating a vacuum and pressure cycle. This cycle draws the material into the pump chamber and then forces it out through the discharge line under controlled pressure. The entire operation is synchronized with the material flow rate and system requirements, ensuring consistent and efficient transport. The working principle of bin pumps is based on the principles of fluid dynamics and mechanical action, allowing them to handle a wide range of materials, from fine powders to granular substances, with minimal degradation or loss.
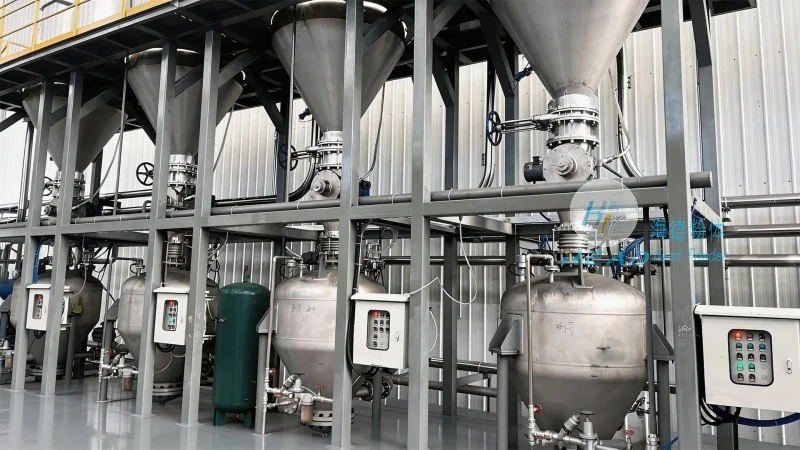
Bin pumps from Shandong HeadPowder Engineering Co., Ltd. are distinguished by several critical features that enhance their performance and adaptability in industrial settings. One of the primary advantages is their ability to handle high volumes of material with minimal maintenance. The robust construction and durable components ensure long-term reliability, even under demanding operational conditions. Another notable feature is the precise control over material flow, which is crucial for applications requiring accurate dosing or consistent discharge rates. This control is achieved through advanced valve systems and pressure regulation mechanisms that prevent material backflow or clogging. Additionally, bin pumps are designed for easy integration into existing material handling systems, with flexible connections and modular components that allow for seamless installation and customization. The company's commitment to quality and innovation is reflected in the advanced technology incorporated into their bin pump designs, such as variable speed drives and automated monitoring systems that optimize performance and reduce downtime.
The versatility of bin pump material handling systems makes them suitable for a wide array of industrial applications. In the chemical industry, bin pumps are used to transport powders and granules, ensuring safe and efficient handling of hazardous materials. In the food and pharmaceutical sectors, their sanitary design and contamination-free operation meet stringent regulatory requirements. The construction industry benefits from bin pumps for transporting cement, sand, and other bulk materials to construction sites, improving productivity and reducing labor costs. The key benefits of using bin pumps include increased efficiency, reduced energy consumption, and enhanced safety compared to traditional conveyor systems. By eliminating the need for multiple transfer points and reducing material handling time, bin pumps contribute to overall operational efficiency and cost savings. The reliability of these systems also minimizes downtime, which is critical for maintaining production schedules and meeting customer demands.
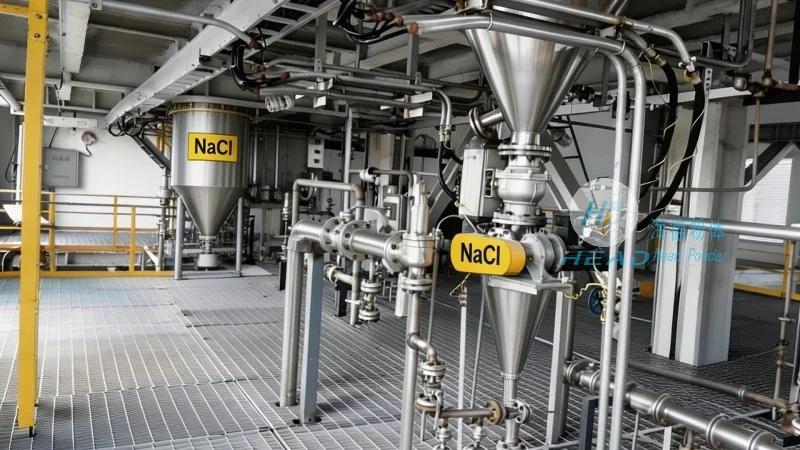
Bin pump material handling systems represent a sophisticated solution for efficient bulk material transport, combining advanced engineering with practical design. Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted provider of high-quality bin pump solutions, leveraging years of experience and technological expertise to meet the evolving needs of industrial clients. With a focus on durability, precision, and adaptability, their bin pumps offer superior performance and reliability for various applications. The company's commitment to customer satisfaction and continuous improvement ensures that their products remain at the forefront of industrial material handling technology. Whether for new installations or system upgrades, bin pumps from HeadPowder are a reliable choice for businesses seeking to optimize their material handling processes and enhance operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top