Working Principle and Features of Coke Powder Pneumatic Conveying Equipment
Coke powder is a crucial raw material in various industrial processes, such as steel production and chemical manufacturing. The efficient and reliable transportation of coke powder from storage to processing units is essential for maintaining production efficiency and reducing operational costs. Pneumatic conveying systems have emerged as a preferred solution for handling coke powder due to their ability to transport materials in a dust-free, low-cost, and flexible manner. This article will explore the working principle and key features of coke powder pneumatic conveying equipment, providing insights into how these systems operate and their advantages in industrial applications.
Working Principle of Coke Powder Pneumatic Conveying Equipment
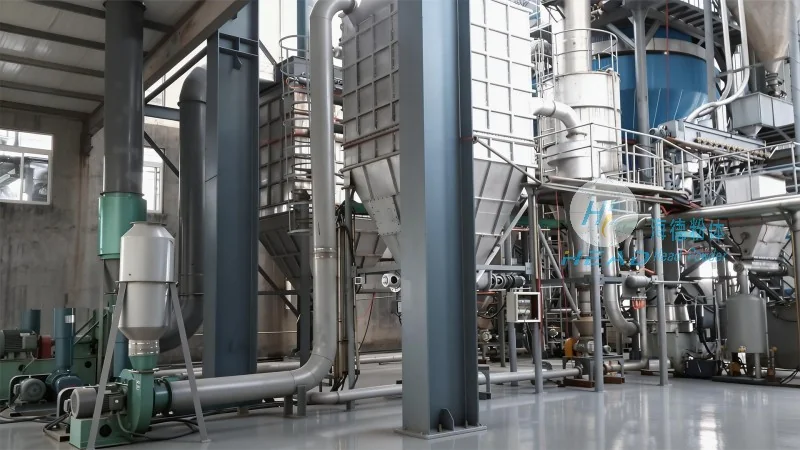
The core of a coke powder pneumatic conveying system is the air flow that propels the powder particles through a pipeline. The system typically operates under either positive pressure or negative pressure (suction) conditions. In positive pressure systems, a blower or compressor generates high-pressure air that forces the coke powder into the pipeline. The powder is then carried by the air stream, with the velocity of the air being sufficient to overcome the gravitational forces and frictional resistance of the powder particles. The pipeline design, including the size and angle of bends, is critical to ensure smooth flow and prevent particle deposition or blockages. Negative pressure systems, on the other hand, use a vacuum pump to create a low-pressure environment that draws the coke powder into the pipeline. This method is often used for short-distance or low-volume conveying tasks. The working principle involves the interaction between the air and the powder, where the air provides the necessary kinetic energy to move the particles, and the pipeline geometry ensures the material is transported efficiently.
Key Features of Coke Powder Pneumatic Conveying Equipment
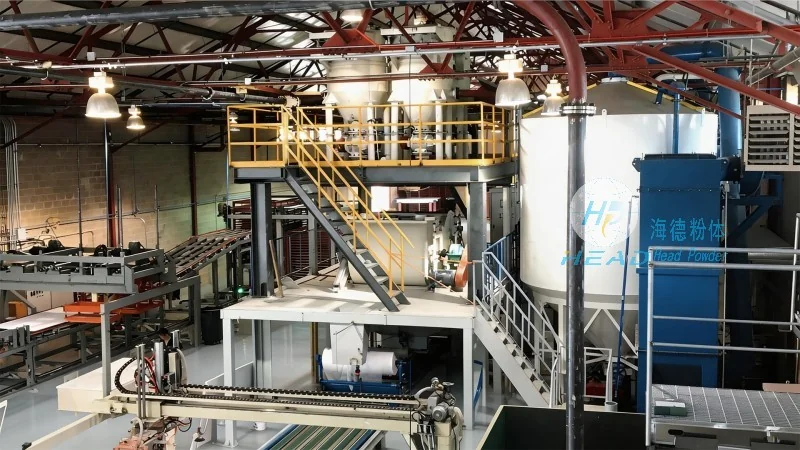
Several key features distinguish coke powder pneumatic conveying equipment from other material handling systems. First, the dust-free operation is a significant advantage. Unlike mechanical conveyors, which can generate dust and pose health hazards, pneumatic systems transport the powder in a sealed pipeline, minimizing environmental contamination and ensuring a safer working environment. Second, the flexibility of the system allows for easy integration into existing production lines. The pipeline can be configured in various shapes and sizes to accommodate different plant layouts, making it adaptable to diverse industrial settings. Third, the low maintenance requirements contribute to cost savings. Pneumatic conveying systems have fewer moving parts compared to mechanical systems, reducing the need for frequent repairs and replacements. Additionally, the ability to handle a wide range of particle sizes and moisture content makes these systems versatile for different coke powder types. The system's efficiency in terms of energy consumption is another notable feature, as it can transport materials over long distances with relatively low power input. Finally, the scalability of the equipment allows for adjustments in conveying capacity based on production needs, providing flexibility for growing industrial operations.
Applications and Benefits in Industrial Settings
Coke powder pneumatic conveying equipment is widely used in industries such as steel manufacturing, where coke is a primary fuel source for blast furnaces. The system ensures that coke powder is delivered to the furnace at a consistent rate, optimizing the combustion process and improving overall efficiency. In chemical plants, the equipment is used to transport coke powder to reactors and processing units, where it serves as a raw material in various chemical reactions. The benefits of using pneumatic conveying in these applications include improved product quality, reduced downtime due to fewer blockages, and enhanced safety through dust control. The ability to handle abrasive materials like coke powder without causing wear and tear on the equipment is also a key advantage, as it extends the lifespan of the system and reduces maintenance costs. Furthermore, the system's ability to operate continuously without interruptions allows for stable production, which is critical in high-demand industrial environments.
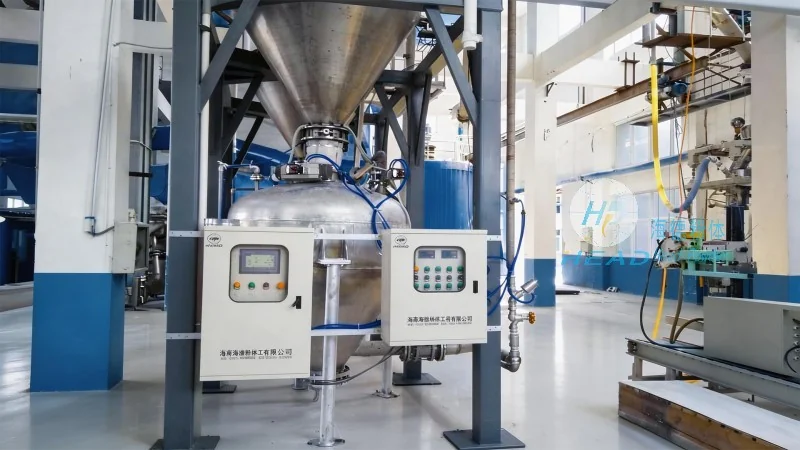
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of coke powder pneumatic conveying equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industrial material handling sector. HeadPowder specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of its clients. The company's products are known for their durability, efficiency, and reliability, meeting the stringent requirements of various industrial applications. HeadPowder's commitment to customer satisfaction is reflected in its comprehensive after-sales service, including technical support, maintenance, and spare parts supply. The company operates from its base in Shandong, China, leveraging its local expertise and resources to provide high-quality solutions to clients worldwide. By combining advanced technology with practical engineering, HeadPowder continues to enhance the performance of coke powder pneumatic conveying equipment, contributing to the efficiency and sustainability of industrial operations.