

What is an Organic Salt Powder Pneumatic Conveying Machine? What Are Its Design Principles?
Organic salt powder pneumatic conveying machines are specialized equipment designed to transport organic salt powders through a pneumatic system. These machines are essential in various industrial applications where the efficient and safe handling of powders is critical. Understanding the design principles behind these machines is crucial for optimizing their performance and ensuring reliable operation.
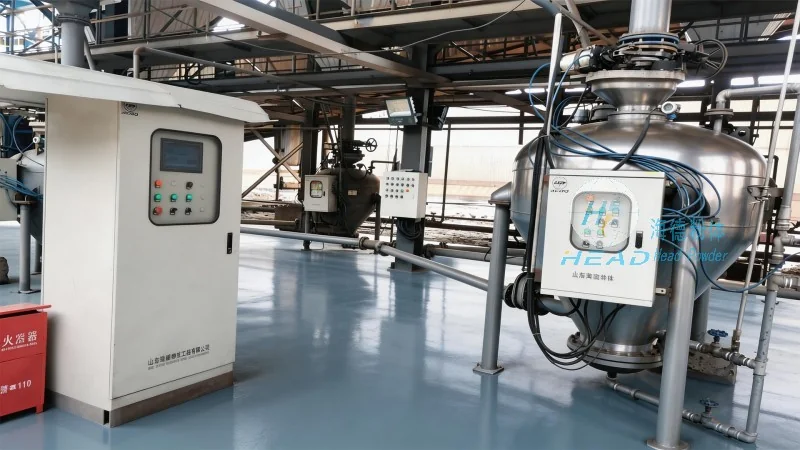
Introduction to Organic Salt Powder Pneumatic Conveying Machines
Organic salt powder pneumatic conveying machines, often referred to as pneumatic conveyors, are systems that use compressed air or other gases to move dry powders, including organic salts, from one location to another. Unlike traditional mechanical conveyors, pneumatic systems offer advantages such as the ability to transport materials over long distances, through vertical or horizontal paths, and even around obstacles. This makes them particularly suitable for industries dealing with organic salt powders, which may be sensitive to moisture, contamination, or physical damage during handling.
Key Components of Organic Salt Powder Pneumatic Conveying Systems
At the core of an organic salt powder pneumatic conveying machine are several key components that work in tandem to ensure efficient material transport. These components include the hopper or feed bin, which holds the organic salt powder; the air compressor or blower, which generates the necessary air pressure; the pipeline system, which transports the powder and air mixture; and the receiver or discharge hopper, where the material is collected. Additionally, many systems incorporate filters and cyclones to separate the powder from the air, ensuring that the organic salt powder remains clean and free from contaminants.
Design Principles for Efficient Organic Salt Powder Transport
The design of an organic salt powder pneumatic conveying machine is guided by several fundamental principles aimed at maximizing efficiency, minimizing material degradation, and ensuring safe operation. One of the primary principles is maintaining a consistent air-to-powder ratio, which is critical for achieving stable and reliable transport. The air velocity within the pipeline must be sufficient to keep the powder particles suspended but not so high as to cause excessive wear on the system components or degrade the organic salt powder.
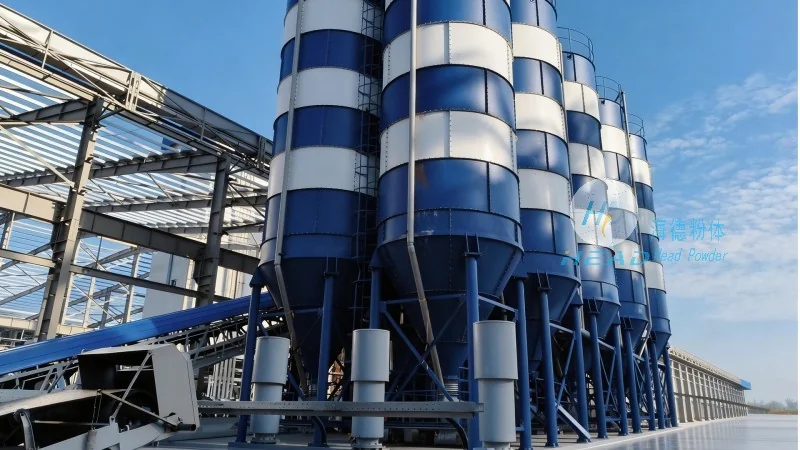
Another important design principle is the selection of appropriate pipeline materials and diameters. The choice of materials, such as stainless steel or food-grade plastics, depends on the properties of the organic salt powder and the operating conditions. The diameter of the pipeline is also carefully considered to balance the air velocity and pressure drop, ensuring that the system operates within optimal parameters. Additionally, the system is designed to minimize pressure losses and energy consumption, which are key factors in the overall efficiency of the conveying process.
Advantages of Organic Salt Powder Pneumatic Conveying Machines
Organic salt powder pneumatic conveying machines offer several advantages over traditional conveying methods. One of the most significant benefits is the ability to transport materials in a closed system, which helps to prevent contamination from external sources and reduces the risk of dust emissions. This is particularly important for organic salt powders, which may be sensitive to moisture or air exposure. Additionally, these systems can handle a wide range of particle sizes and shapes, making them versatile for various industrial applications.
Another advantage is the flexibility in system layout. Pneumatic conveyors can be configured to follow complex paths, including vertical lifts and horizontal turns, which is often necessary in industrial settings where space is limited or the material needs to be transported to different levels. This flexibility allows for the integration of the conveying system into existing production lines without significant modifications.
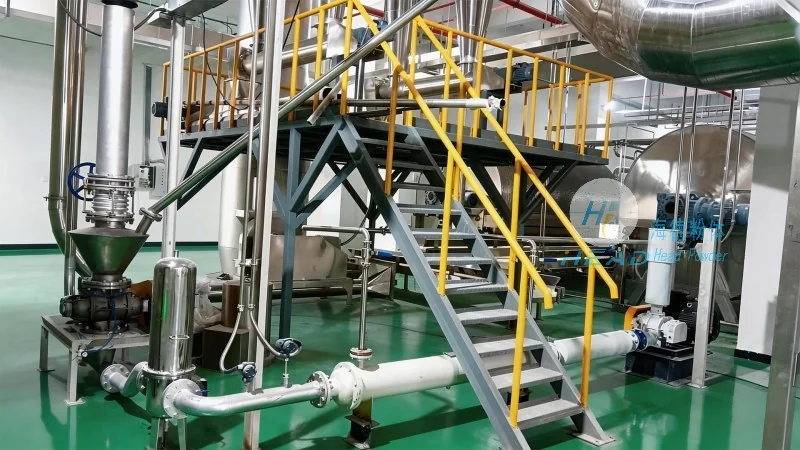
Applications of Organic Salt Powder Pneumatic Conveying Machines
Organic salt powder pneumatic conveying machines are widely used in various industries that handle organic salt powders. These include the chemical industry, food processing, pharmaceuticals, and agriculture. In the chemical industry, they are used to transport organic salts used in the production of fertilizers, pharmaceuticals, and other chemical products. In food processing, they are employed to handle organic salt powders used as food additives or preservatives. The pharmaceutical industry also relies on these systems to transport organic salt powders used in the formulation of medications.
In agriculture, pneumatic conveyors are used to transport organic salt powders such as fertilizers or animal feed supplements. The ability to handle these materials efficiently and safely is crucial for maintaining productivity and ensuring the quality of the final products. Overall, the versatility and reliability of organic salt powder pneumatic conveying machines make them an essential component in many industrial processes.
Conclusion
Organic salt powder pneumatic conveying machines are sophisticated equipment designed to efficiently and safely transport organic salt powders through pneumatic systems. The design principles behind these machines, including maintaining optimal air-to-powder ratios, selecting appropriate materials and pipeline diameters, and ensuring efficient filtration, are critical to their performance. The advantages of closed systems, flexibility in layout, and ability to handle various particle sizes make them a preferred choice in many industrial applications. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality organic salt powder pneumatic conveying machines that meet the specific needs of their clients, ensuring reliable and efficient material transport in various industrial settings.