With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Bin pump material handling equipment is a specialized industrial device designed to transport bulk materials from one location to another with high efficiency and precision. This equipment is widely used in various industries to handle powders, granules, and other bulk solids. The core function of a bin pump is to draw material from a storage bin or hopper and then discharge it through a pipeline system to the desired destination. Understanding the design principles behind bin pumps is crucial for optimizing material transport processes in industrial settings.
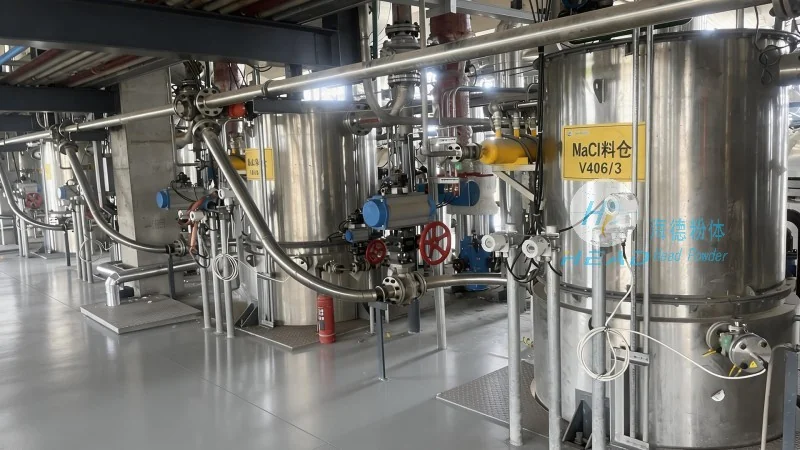
The bin pump consists of several key components that work together to achieve material transport. The primary components include a hopper or storage bin, a pump body, a valve system, and a discharge pipeline. The working principle involves the pump drawing material from the hopper using a suction mechanism, typically through a rotary or sliding valve. As the pump chamber fills with material, the valve closes to prevent backflow, and then the pump discharges the material through the outlet pipe. This process is often automated and can be controlled by a system of sensors and controls to ensure consistent flow rates and prevent blockages.
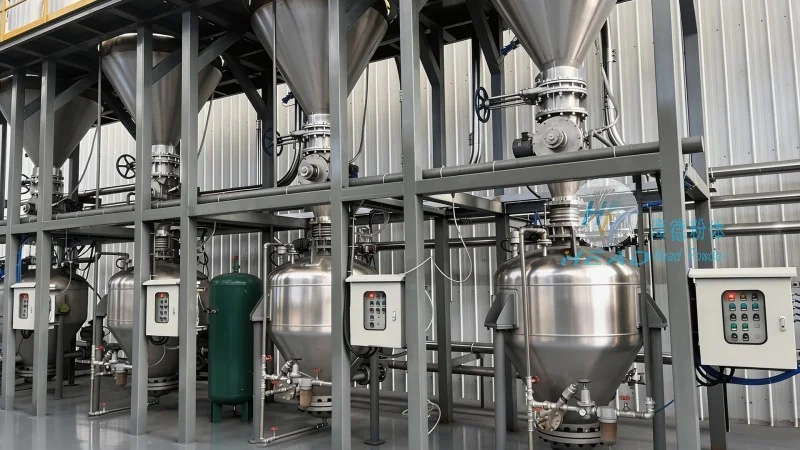
Design principles for bin pumps focus on maximizing efficiency, reliability, and safety in material handling operations. Engineers consider factors such as the properties of the material being handled (e.g., particle size, density, flowability), the required flow rate, and the distance over which material needs to be transported. The pump's design must accommodate the material's characteristics to prevent issues like clogging or degradation. For example, materials with high moisture content or fine particles may require special pump designs with anti-wear components or improved sealing systems. Additionally, the pump's structure is engineered to handle the pressure and force exerted by the material during transport, ensuring durability and long-term performance.
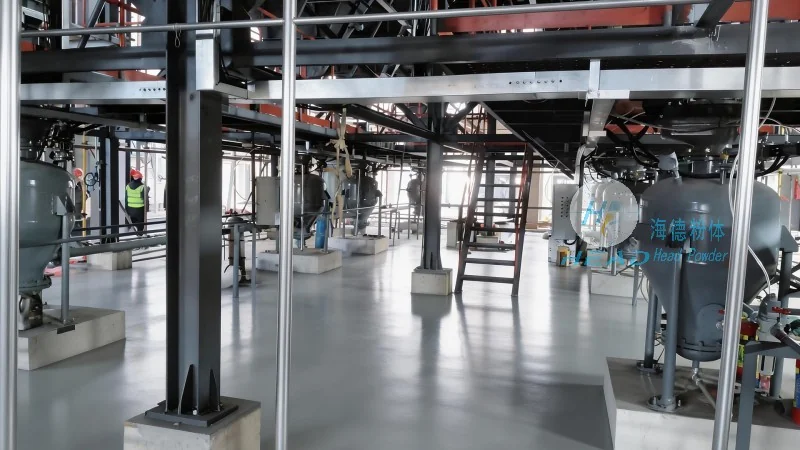
Bin pump systems are utilized in a wide range of industries where bulk material transport is essential. These include the chemical industry for transporting chemicals and additives, the food and beverage industry for handling powders like flour and sugar, the mining industry for moving ore and minerals, and the pharmaceutical industry for transporting raw materials and finished products. In each of these sectors, the bin pump's ability to handle large volumes of material with minimal human intervention makes it a critical component of the production and logistics processes.
There are several advantages to using bin pump systems for material handling. One key benefit is the high efficiency in transporting bulk materials, as bin pumps can handle large volumes of material at a consistent rate compared to traditional methods like conveyor belts or manual loading. This leads to increased productivity and reduced labor costs. Another advantage is the flexibility of the system, as bin pumps can be easily integrated with existing infrastructure and adapted to different material types and transport distances. Additionally, bin pumps are designed to minimize material degradation and contamination, which is particularly important in industries like food and pharmaceuticals where product quality is paramount. The automated nature of bin pump systems also reduces the risk of human error and improves safety in the workplace.
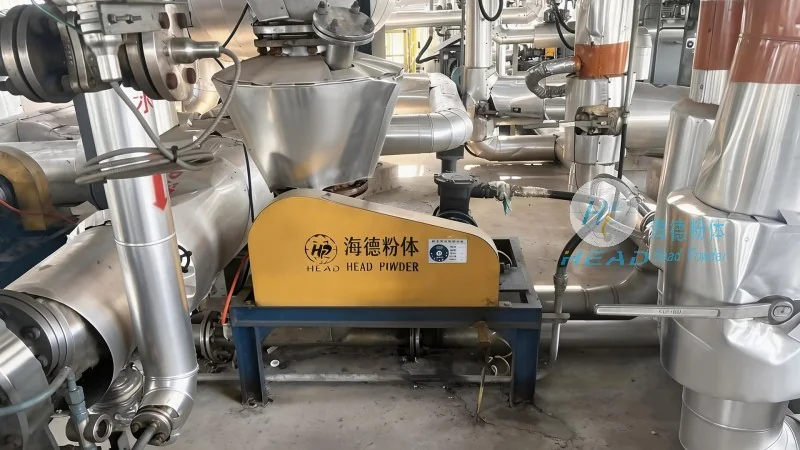
In conclusion, bin pump material handling equipment is a vital tool in modern industrial operations, providing efficient and reliable transport of bulk materials. The design principles behind these systems are tailored to meet the specific needs of different industries and materials, ensuring optimal performance and durability. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality bin pump solutions that meet the demands of various industrial applications. With a focus on innovation and customer satisfaction, the company continues to develop advanced material handling equipment that enhances productivity and efficiency in material transport processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top