With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Intelligent material handling conveyors represent a sophisticated evolution in industrial automation, designed to streamline the movement of goods within manufacturing and logistics environments. These systems integrate advanced technologies to enhance efficiency, accuracy, and operational flexibility, addressing the growing demands for speed and reliability in modern production processes.
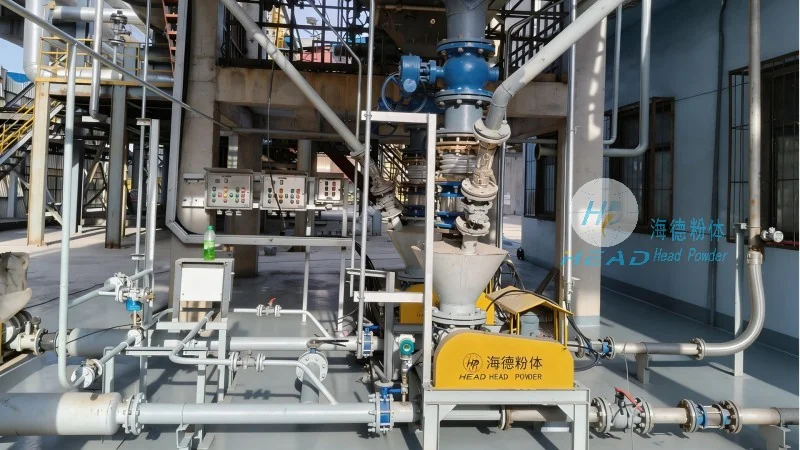
An intelligent material handling conveyor is a specialized system engineered to transport materials, components, or finished products through a production line or warehouse. Unlike traditional conveyors, these systems incorporate intelligent features such as real-time monitoring, adaptive control, and data-driven decision-making capabilities. The primary goal is to optimize workflow, reduce downtime, and improve overall productivity by ensuring that materials are moved precisely when and where they are needed.
HeadPowder, the brand under Shandong HeadPowder Engineering Co., Ltd., is a leading provider of industrial automation solutions. With a strong presence in China, particularly in Shandong, the company specializes in designing, manufacturing, and implementing intelligent material handling systems tailored to the unique needs of various industries. The company's commitment to innovation and quality has established it as a trusted partner for businesses seeking to enhance their operational efficiency through advanced conveyor technology.
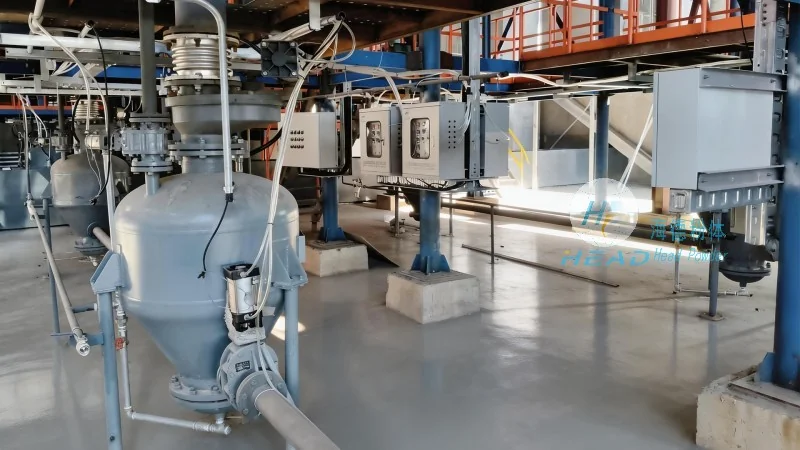
The design of an intelligent material handling conveyor is built upon several key principles that ensure its effectiveness and adaptability. First, automation is central, with systems often incorporating robotic arms, automated guided vehicles (AGVs), or programmable logic controllers (PLCs) to control the movement of materials. Second, integration of sensors and IoT devices enables real-time tracking and monitoring of the conveyor's performance, allowing for immediate adjustments to optimize flow. Third, modularity allows for easy customization and scalability, enabling the system to grow with the evolving needs of a business. Finally, energy efficiency is a critical consideration, with designs incorporating features like variable frequency drives (VFDs) to reduce power consumption while maintaining performance.
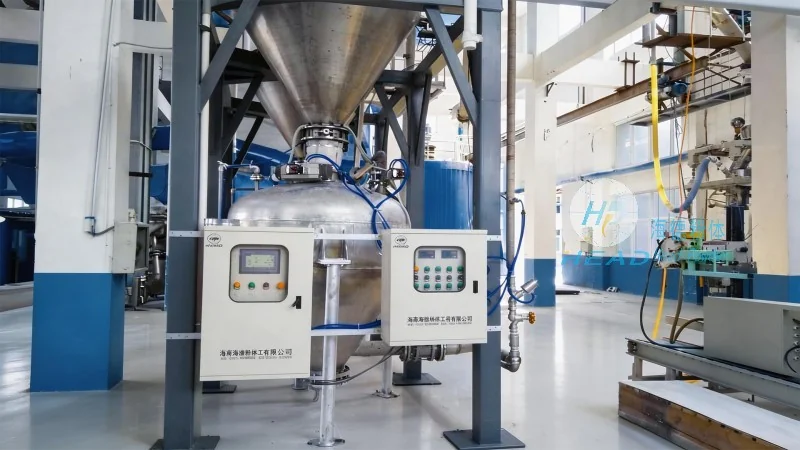
Intelligent material handling conveyors offer a range of features that contribute to their superior performance. These include high-speed operation, precise positioning, and the ability to handle a variety of material types and sizes. The systems are also designed for durability and low maintenance, reducing operational costs over time. By integrating with other industrial systems, such as inventory management software or quality control tools, these conveyors can provide comprehensive data insights, enabling businesses to make informed decisions and further improve their processes.
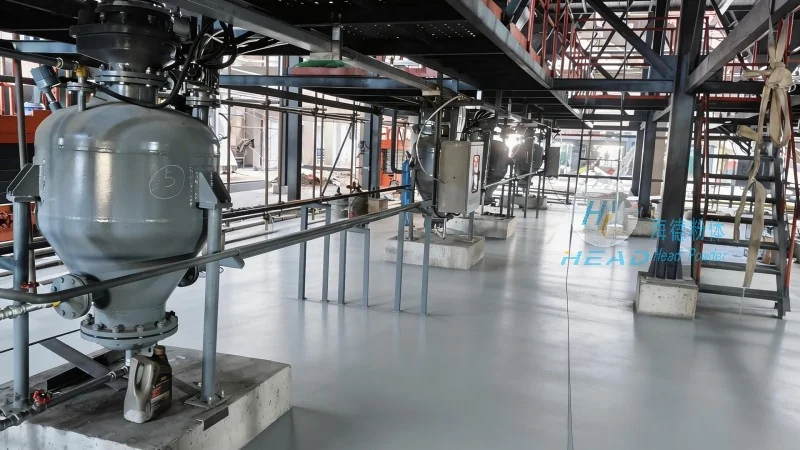
The versatility of intelligent material handling conveyors makes them suitable for a wide array of applications across various sectors. In manufacturing, they are commonly used in assembly lines to transport parts and components, ensuring a smooth and continuous production flow. In logistics and warehousing, these systems are employed for order picking, sorting, and distribution, enhancing the speed and accuracy of order fulfillment. Additionally, they are utilized in pharmaceutical and food processing industries, where strict hygiene and compliance standards require advanced, cleanable conveyor designs.
As industries continue to evolve, the demand for intelligent material handling conveyors is expected to grow, driven by the need for greater efficiency and adaptability. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in this evolution, providing cutting-edge solutions that help businesses stay competitive in a rapidly changing market. By leveraging the design principles and advanced features of these systems, organizations can achieve significant improvements in productivity, reduce operational costs, and enhance their overall operational performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top