With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the role and design principles of inorganic salt powder conveyors is crucial for industries dealing with bulk powder handling. These specialized equipment are engineered to efficiently transport various inorganic salts, such as sodium chloride, calcium carbonate, or other mineral powders, ensuring smooth and reliable material transfer in industrial processes. The proper functioning of these conveyors directly impacts production efficiency, material quality, and operational safety in sectors like chemical manufacturing, food processing, and pharmaceuticals.
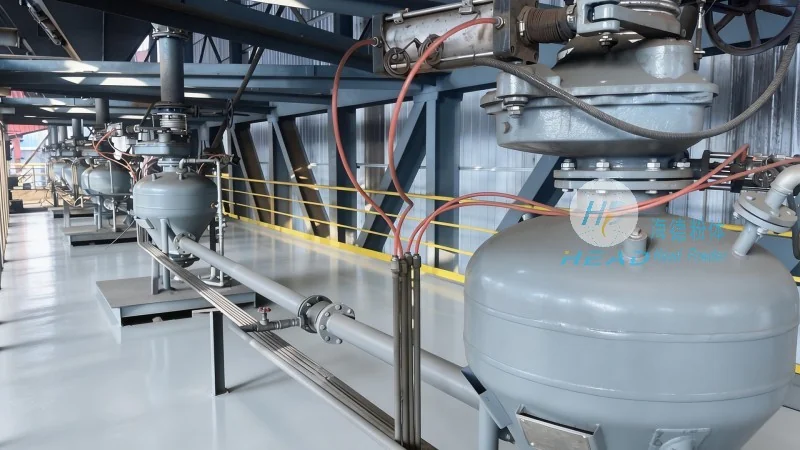
The design of an inorganic salt powder conveyor typically involves several critical components that work in harmony to achieve optimal performance. The primary elements include a hopper for material storage, a conveyor mechanism (like screw or pneumatic systems), and control systems for regulating flow and speed. The design principles focus on minimizing material degradation, preventing clogging, and ensuring consistent flow rates. For instance, the use of appropriate hopper angles and material-specific conveyor designs helps in reducing the risk of agglomeration and blockages, which are common issues in powder handling. Additionally, features like anti-static coatings and wear-resistant materials are incorporated to address the abrasive nature of many inorganic salts.
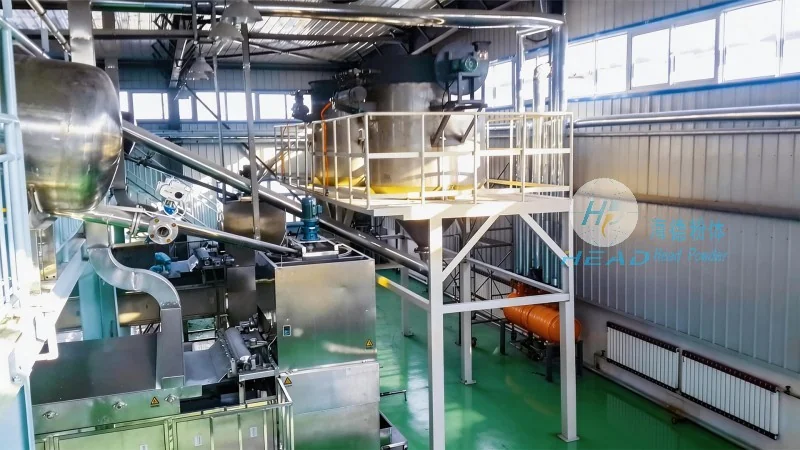
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in developing and manufacturing advanced powder handling equipment tailored to the needs of various industries. With years of experience in the field, HeadPowder understands the unique challenges associated with handling inorganic salts, such as their tendency to stick to surfaces or cause corrosion. The company’s engineers design conveyors with features like anti-stick coatings, adjustable speed controls, and robust construction to address these challenges effectively. By focusing on durability and efficiency, HeadPowder’s products help industries maintain high production standards while minimizing downtime and maintenance costs. The company’s commitment to innovation ensures that their conveyors meet the evolving demands of modern industrial applications.
Inorganic salt powder conveyors find wide applications across multiple sectors, including chemical manufacturing, food processing, and pharmaceuticals. In chemical plants, they are used to transport raw materials like calcium chloride or sodium bicarbonate, ensuring seamless integration into production lines. In food processing, conveyors help in moving salt for seasoning or preservation, maintaining hygiene and product quality. The benefits of using these conveyors include improved safety by reducing manual handling, enhanced accuracy in material measurement, and increased operational efficiency. Additionally, the design allows for easy integration with other processing equipment, making it a versatile solution for modern industrial setups. Industries that adopt these conveyors often report reduced waste, lower energy consumption, and better control over material flow.
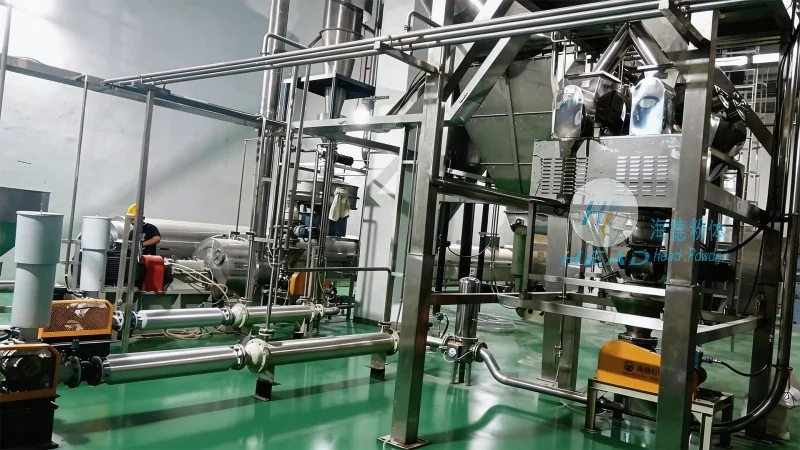
HeadPowder recognizes that each industrial application has unique requirements, which is why they offer customized solutions for inorganic salt powder conveyors. Customers can specify parameters such as material type, flow rate, and environmental conditions to get a tailored system. The company also provides comprehensive maintenance services to ensure the longevity of the equipment. Regular inspections, component replacements, and cleaning protocols are essential to maintain the conveyor’s performance. By adhering to proper maintenance practices, industries can maximize the lifespan of their conveyors and avoid unexpected breakdowns that could disrupt production. HeadPowder’s after-sales support includes technical guidance and spare parts availability, further enhancing the reliability of their equipment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top