

What is a Grain Silo Powder Conveying System? What are its Design Principles?
For industries dealing with bulk materials like grains, efficient and reliable powder conveying systems are crucial for operations. A grain silo powder conveying system is a specialized setup designed to transport bulk powders, such as grains, from storage silos to processing or packaging areas. This system plays a vital role in ensuring smooth material flow, minimizing downtime, and maintaining product quality throughout the handling process. In this article, we will explore the fundamental aspects of these systems, including their design principles and key components.
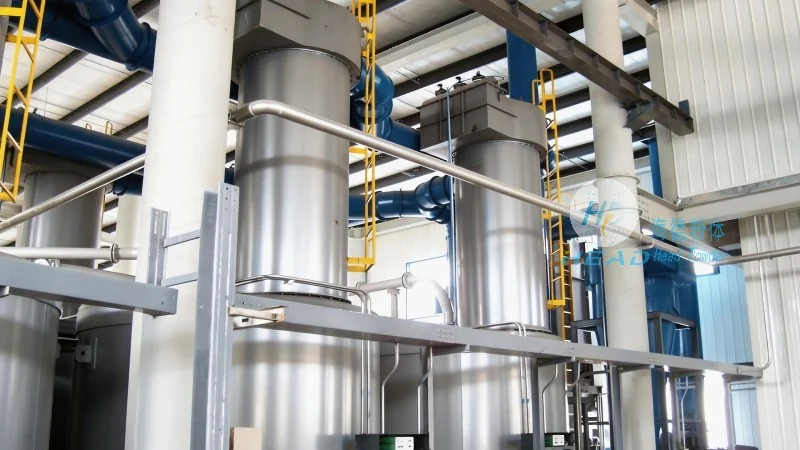
Key Components of a Grain Silo Powder Conveying System
The core of any grain silo powder conveying system consists of several interconnected components that work in harmony to achieve effective material transport. The primary components typically include a hopper or feeder, a conveyor mechanism (such as a screw conveyor, pneumatic conveyor, or bucket elevator), a control system, and a silo or storage tank. Each component is carefully selected and integrated to meet the specific requirements of the material being handled, the system's capacity, and the operational environment.
First, the hopper or feeder is responsible for receiving bulk material from the silo and feeding it into the conveyor system. This component must be designed to handle the material's characteristics, such as its flowability and density, to prevent issues like bridging or clogging. The feeder may include features like a rotary valve or a gate to regulate the flow rate, ensuring a consistent and controlled discharge of material.
Next, the conveyor mechanism is the heart of the system, responsible for moving the material from the feeder to the desired destination. There are several types of conveyors used in grain silo applications, each with its own advantages and applications. For example, screw conveyors are commonly used for horizontal or slightly inclined transport due to their simplicity and reliability. Pneumatic conveyors, on the other hand, use air pressure to transport material, making them suitable for fine powders and dusty environments. Bucket elevators are ideal for vertical transport, capable of handling heavy loads and steep inclines.
Design Principles for Optimal Performance
The design of a grain silo powder conveying system follows several key principles to ensure efficiency, safety, and longevity. These principles are tailored to the specific needs of the material and the operational conditions, and they are critical in preventing operational issues and maximizing system performance.
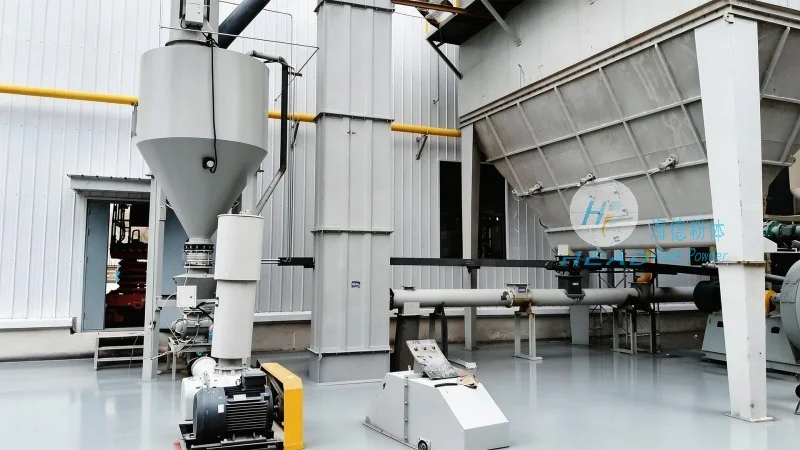
First and foremost, the system must be designed to handle the material's physical properties. This includes considering factors such as particle size, moisture content, and flowability. For example, materials with high moisture content may require special considerations to prevent caking or blockages, while fine powders may need a more gentle handling approach to avoid dust generation and material degradation. The design must also account for the material's density and bulk density, as these affect the system's capacity and power requirements.
Second, the system's capacity and throughput must be matched to the operational demands. The conveyor and feeder components must be sized appropriately to handle the expected flow rate, ensuring that the system can meet production requirements without bottlenecks. This involves calculating the material's flow rate based on factors like the silo's size, the conveyor's speed, and the system's efficiency. Proper sizing is essential to prevent overloading, which can lead to system failure or reduced performance.
Third, the system must be designed with safety and maintenance in mind. This includes incorporating features like emergency stop buttons, overload protection, and regular maintenance access points. The materials used in the construction of the system components must be durable and resistant to corrosion, especially when handling materials that may be acidic or abrasive. Additionally, the system should be designed to minimize dust generation and ensure proper ventilation to protect both the equipment and the personnel operating it.
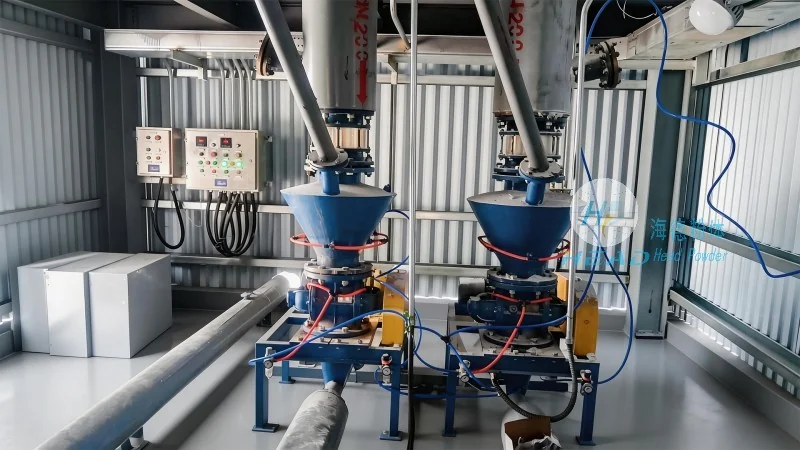
The Role of HeadPowder in Grain Silo Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for bulk material handling, including grain silo powder conveying systems. With a strong focus on innovation and customer-centric design, HeadPowder has established itself as a trusted partner for industries requiring reliable and efficient material transport solutions.
HeadPowder's expertise lies in designing and manufacturing custom conveying systems tailored to the unique needs of each client. The company's team of experienced engineers works closely with clients to understand their operational requirements, material characteristics, and budget constraints, ensuring that the final solution is both effective and cost-efficient. By leveraging advanced engineering techniques and high-quality materials, HeadPowder delivers systems that meet or exceed industry standards for performance, durability, and safety.
HeadPowder's grain silo powder conveying systems are designed with a focus on durability and long-term reliability. The components are constructed from robust materials, such as stainless steel or corrosion-resistant alloys, to withstand the harsh conditions of bulk material handling. The system's design incorporates features that minimize wear and tear, reducing the need for frequent maintenance and extending the system's lifespan. Additionally, the company provides comprehensive support services, including installation, commissioning, and ongoing maintenance, to ensure that clients can maximize the system's performance and lifespan.
Conclusion
In conclusion, a grain silo powder conveying system is a critical component in industries dealing with bulk materials, and its design principles are essential for ensuring efficient and reliable operation. By understanding the key components and design considerations, businesses can select and implement a system that meets their specific needs and enhances their overall operational efficiency. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these specialized solutions, helping industries to optimize their material handling processes and achieve their production goals.