With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
This article provides an in-depth look at the principle and application of pneumatic conveying equipment designed for handling fertilizer granules. As a specialized solution in material handling, this technology plays a crucial role in the efficient transport of bulk fertilizer products from production sites to storage or processing facilities. The equipment is engineered to meet the unique challenges of fertilizer granule characteristics, such as size, density, and moisture content, ensuring reliable and safe operation.
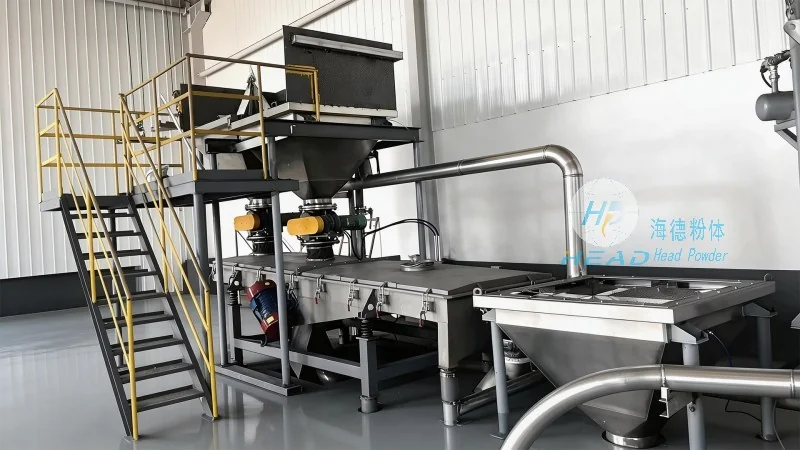
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in engineering solutions for material handling and processing equipment. With a focus on innovation and quality, the company has established itself as a trusted partner in the fertilizer and bulk material industry. HeadPowder's expertise lies in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of clients, ensuring optimal performance and durability.
The pneumatic conveying system for fertilizer granules typically consists of several key components, including a hopper for material storage, a conveyor line, a blower or compressor to generate air flow, and a control system. The working principle involves the following steps: first, fertilizer granules are fed into the hopper from the production line. Then, the blower creates a high-pressure air stream that draws the granules into the conveyor line. The air and granules are mixed and transported through the pipeline to the destination point, such as a silo or processing unit. The system uses positive or negative pressure depending on the application, with positive pressure being common for long-distance or high-capacity transport.
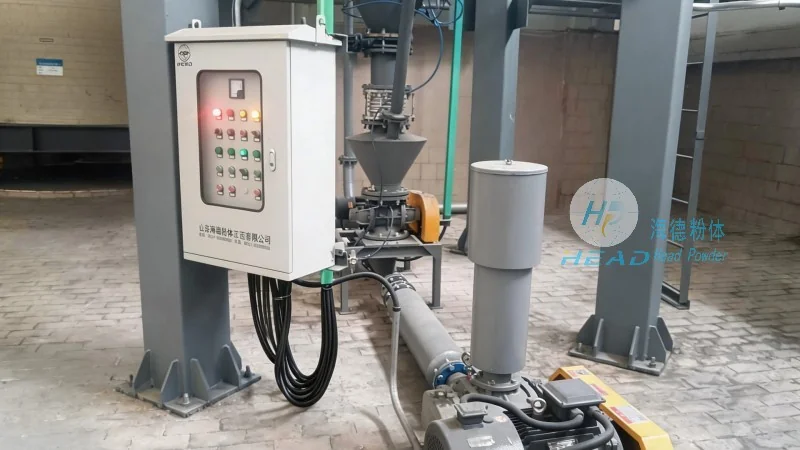
Compared to traditional mechanical conveying methods, pneumatic conveying offers several advantages when handling fertilizer granules. These include: 1) Reduced risk of product contamination due to enclosed systems, which is critical for maintaining the quality and purity of fertilizer products. 2) Lower maintenance costs as there are fewer moving parts compared to belt or screw conveyors. 3) Improved safety as the system is fully enclosed, minimizing dust exposure and the risk of accidents. 4) Flexibility in system design, allowing for multiple transfer points and integration with existing production lines. 5) Energy efficiency, as the system can be optimized to use the minimum amount of air required for effective transport.
The pneumatic conveying equipment is widely used in various stages of the fertilizer production and distribution process. For instance, it can be employed to transport granules from the granulation or drying unit to the packaging area. It is also suitable for moving fertilizer from storage silos to loading trucks or ships, ensuring a continuous and smooth supply chain. Additionally, the system can be integrated into automated production lines, enhancing overall operational efficiency and reducing labor costs.
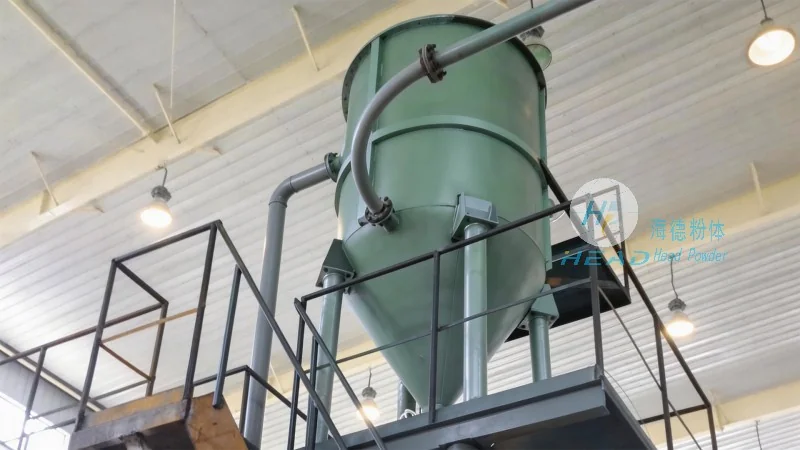
HeadPowder offers a range of pneumatic conveying systems with customizable specifications to meet different operational requirements. Key technical parameters include the capacity of the system (measured in tons per hour), the length and diameter of the conveyor line, the type of air compressor (positive or negative pressure), and the material of construction (such as stainless steel or carbon steel for corrosion resistance). The company works closely with clients to assess their specific needs and provide tailored solutions that maximize efficiency and minimize downtime.
Pneumatic conveying equipment for fertilizer granules is a vital technology in modern fertilizer handling operations. By leveraging the principles of air flow and material transport, this equipment ensures efficient, safe, and cost-effective movement of bulk fertilizer products. With its advantages in contamination control, maintenance, and flexibility, the system is an essential component for companies like Shandong HeadPowder Engineering Co., Ltd., which specializes in providing high-quality material handling solutions. As the fertilizer industry continues to evolve, the demand for reliable and efficient conveying systems will remain high, making this technology a cornerstone of modern production and distribution processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top