With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Chocolate powder handling systems are critical components in the food processing industry, particularly for manufacturers dealing with chocolate products. These systems ensure efficient, hygienic, and reliable transportation of chocolate powders from production lines to storage or packaging areas. The design and functionality of such systems directly impact production efficiency, product quality, and overall operational costs. This overview will explore the key structural elements and working principles of chocolate powder conveying systems, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in providing tailored solutions for the industry.
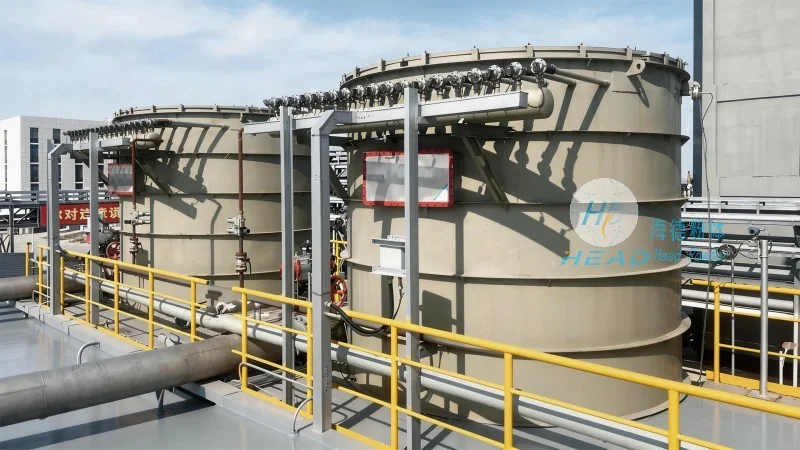
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer specializing in powder handling equipment. With a focus on innovation and precision engineering, the company has established itself as a trusted partner for businesses in the confectionery sector. HeadPowder's commitment to quality and customer satisfaction is reflected in its comprehensive range of powder handling solutions, including chocolate powder conveying systems. The company's headquarters and main operations are based in Shandong, China, where it leverages local expertise and resources to develop advanced machinery tailored to the unique demands of chocolate production.
The chocolate powder conveying system typically consists of several integrated components that work in tandem to ensure smooth and efficient operation. The primary structural elements include: conveying lines, which may be made of stainless steel or food-grade materials to maintain hygiene standards; feeding mechanisms, such as rotary valves or screw feeders, that control the flow of chocolate powder from storage silos or hoppers; airlock or rotary airlock valves, which prevent backflow and maintain a consistent pressure differential; and control panels, equipped with sensors and automation systems to monitor and regulate the conveying process. The design of these components is optimized to handle the specific properties of chocolate powders, such as their fine particle size, moisture sensitivity, and potential for caking. Stainless steel construction is a common choice due to its corrosion resistance, ease of cleaning, and compliance with food safety regulations. The conveying lines are often equipped with smooth, rounded surfaces to minimize powder buildup and ensure consistent flow. Feeding mechanisms are designed to handle varying bulk densities and flow rates, providing precise control over the powder discharge. Airlock valves are crucial for maintaining airtightness and preventing contamination from external sources. Control panels integrate sensors for level monitoring, pressure measurement, and flow rate control, enabling automated operation and real-time adjustments to optimize system performance.
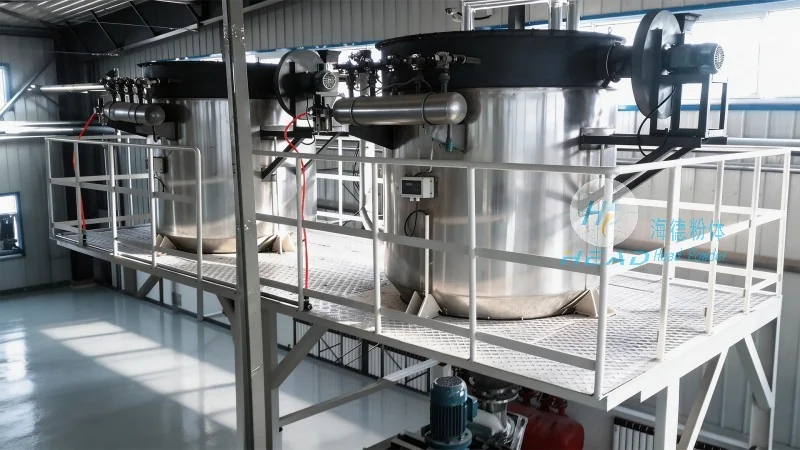
The operation of a chocolate powder conveying system is based on the principles of pneumatic or mechanical conveying, depending on the specific design. Pneumatic conveying systems use compressed air to transport chocolate powder through a network of pipes, while mechanical systems rely on screw conveyors or belt conveyors to move the powder. In pneumatic systems, the chocolate powder is drawn into the conveying line by the air flow, and the air-powder mixture is then transported to the destination. The system typically includes a blower or compressor to generate the necessary air pressure, and a filter to remove any fine particles from the air before it is released back into the environment. Mechanical systems, on the other hand, use rotating screws or belts to push the chocolate powder along the conveying path. These systems are often preferred for applications where the powder is highly abrasive or where airtightness is critical. The working principle involves the continuous rotation of the screw or belt, which creates a positive displacement that moves the powder forward. The speed and torque of the motor driving the conveyor can be adjusted to control the flow rate, ensuring that the system operates at optimal efficiency. Both pneumatic and mechanical systems are designed to handle the unique challenges of chocolate powders, such as their tendency to clump or adhere to surfaces. Advanced systems may incorporate features like vibration or agitators to prevent caking and maintain consistent flow. The control system monitors key parameters, such as pressure, flow rate, and temperature, to detect any deviations and adjust the operation accordingly. This ensures that the chocolate powder is conveyed safely and efficiently, minimizing the risk of product contamination or equipment damage.
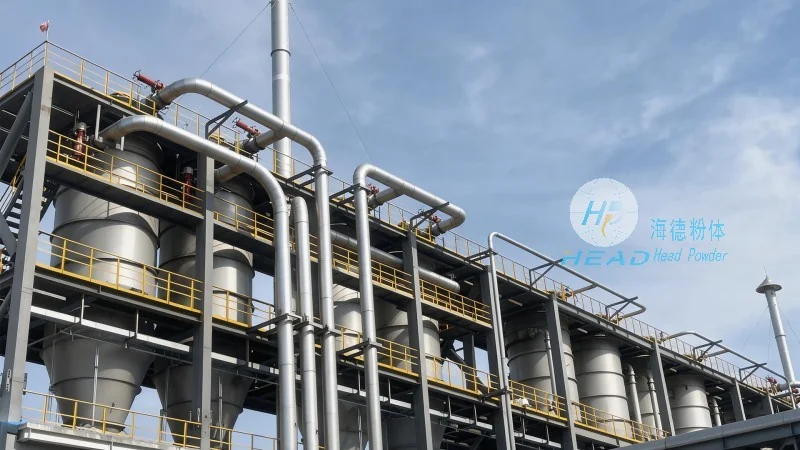
HeadPowder Engineering's chocolate powder conveying systems are engineered with several key features that enhance performance and reliability. These systems are designed to handle the specific characteristics of chocolate powders, including their fine particle size, moisture content, and potential for caking. The use of stainless steel construction ensures durability and easy cleaning, which is essential for maintaining food safety standards. The systems are equipped with advanced control panels that integrate sensors and automation technology, allowing for precise monitoring and adjustment of the conveying process. This automation reduces the need for manual intervention, improving operational efficiency and minimizing human error. The conveying lines are designed with smooth, rounded surfaces and minimal dead zones to prevent powder accumulation and ensure consistent flow. This design reduces the risk of caking and improves the overall hygiene of the system. HeadPowder's systems also incorporate features such as airlock valves and filter systems to maintain airtightness and prevent contamination. The airlock valves prevent backflow and maintain a consistent pressure differential, while the filters remove any fine particles from the air before it is released. These features ensure that the chocolate powder remains free from contaminants and that the system operates within safe and hygienic parameters. The company's expertise in powder handling technology allows for customized solutions that meet the specific requirements of each client. Whether for small-scale production or large industrial operations, HeadPowder provides systems that are tailored to the unique needs of the confectionery industry. The systems are designed to be scalable, allowing for easy expansion as production needs grow. This flexibility makes HeadPowder's solutions suitable for a wide range of applications, from chocolate manufacturing to ingredient handling in other food processing facilities.
Chocolate powder conveying systems are widely used in various stages of chocolate production, from raw material handling to finished product packaging. In the production process, these systems are used to transport chocolate powders from storage silos to mixing lines, ensuring a consistent supply of ingredients. During the mixing stage, the systems help maintain the uniformity of the chocolate blend by delivering the powder at a controlled rate. After mixing, the systems transport the chocolate powder to storage tanks or directly to packaging lines. The efficiency of the conveying system directly impacts the overall production cycle time, as delays in powder handling can lead to bottlenecks in the production line. By ensuring smooth and reliable powder transport, these systems help manufacturers maintain high production throughput and meet customer demand. The use of advanced conveying systems also contributes to improved product quality. Consistent flow rates and hygienic handling minimize the risk of contamination and ensure that the chocolate powder meets the required quality standards. This is particularly important in the confectionery industry, where product quality and safety are paramount. HeadPowder's systems are designed to meet the stringent requirements of food safety regulations, such as those set by the FDA and other international bodies. The systems are constructed from materials that are compliant with food-grade standards and are easy to clean and sanitize. This ensures that the chocolate powder remains free from contaminants and that the equipment can be maintained in a hygienic condition. The impact of these systems extends beyond individual manufacturers. By improving the efficiency and reliability of chocolate powder handling, HeadPowder's solutions contribute to the overall productivity and competitiveness of the confectionery industry. The ability to handle large volumes of chocolate powder with minimal downtime and maintenance reduces operational costs and increases profitability for businesses. Additionally, the advanced technology used in these systems helps manufacturers stay competitive in a rapidly evolving market. The integration of automation and control systems allows for real-time monitoring and adjustment, enabling manufacturers to respond quickly to changes in production demand or product specifications. This adaptability is crucial in an industry where consumer preferences and market trends are constantly changing. Overall, chocolate powder conveying systems play a vital role in modern chocolate production, and the expertise of companies like HeadPowder is essential for meeting the demands of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top