With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling rare earth materials. This article provides an overview of the key equipment components and the underlying structural principles that define the functionality and efficiency of these systems.
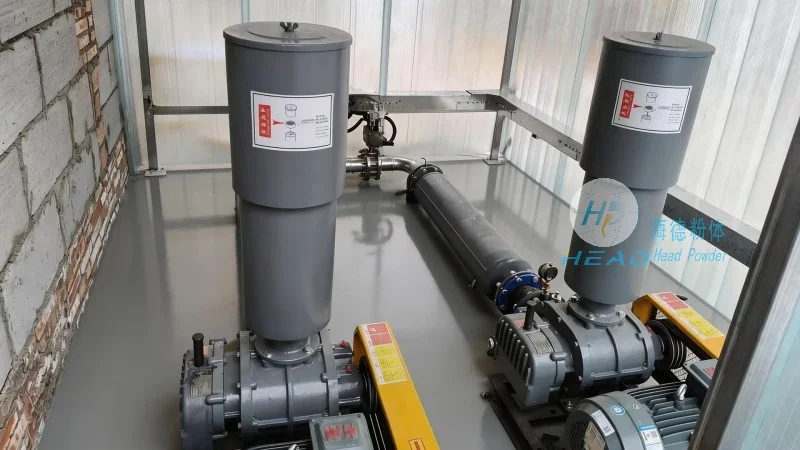
The core components of a rare earth pneumatic conveying system typically include a material feeder, a conveying pipeline, a dust separator, and a receiver. Each component is engineered to work in concert to ensure the safe, efficient, and reliable transport of rare earth powders or granules. The material feeder is responsible for accurately dosing the material into the system, while the conveying pipeline, often made from corrosion-resistant materials such as stainless steel or special alloys, ensures the material is transported under controlled air pressure. The dust separator is critical for maintaining air quality and preventing material loss, and the receiver collects the conveyed material for subsequent processing or storage.
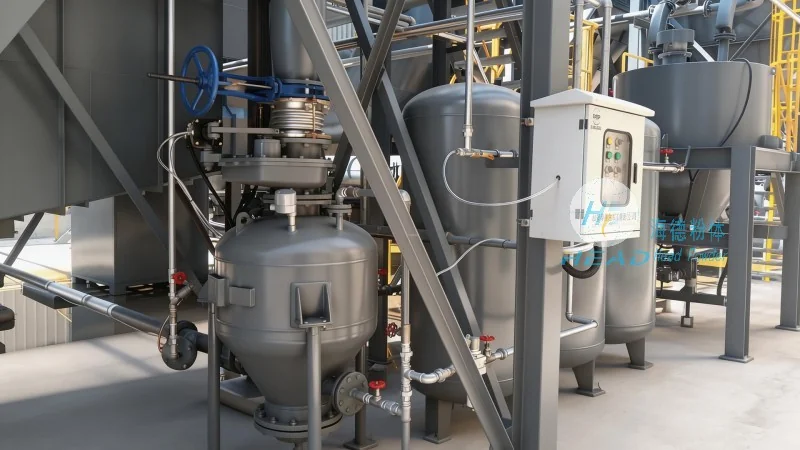
The fundamental principle of pneumatic conveying is the use of compressed air to create a flow that transports solid particles. In the case of rare earth materials, which often have specific handling requirements due to their chemical properties and particle size distribution, the system design must account for factors like material density, moisture content, and potential reactivity. The structural design involves optimizing the air velocity and pressure within the pipeline to achieve the desired conveying capacity without causing material degradation or equipment wear. For example, the use of pulse-jet or continuous air flow systems may be selected based on the material's characteristics and the required transport distance. The system also incorporates features such as check valves and flow control devices to manage the air and material flow dynamically, ensuring smooth operation and preventing backflow or blockages.
HeadPowder's rare earth pneumatic conveying systems are designed with several key features that enhance performance and reliability. These include advanced material handling capabilities that accommodate the unique properties of rare earth materials, such as high purity requirements and sensitivity to moisture or contamination. The systems are equipped with robust filtration and separation mechanisms to maintain material quality and comply with environmental regulations. Additionally, the modular design allows for easy integration into existing production lines and facilitates maintenance and repairs. The use of high-quality materials and precision engineering ensures long service life and minimal downtime, making these systems a cost-effective solution for industries that rely on the consistent and efficient transport of rare earth materials.
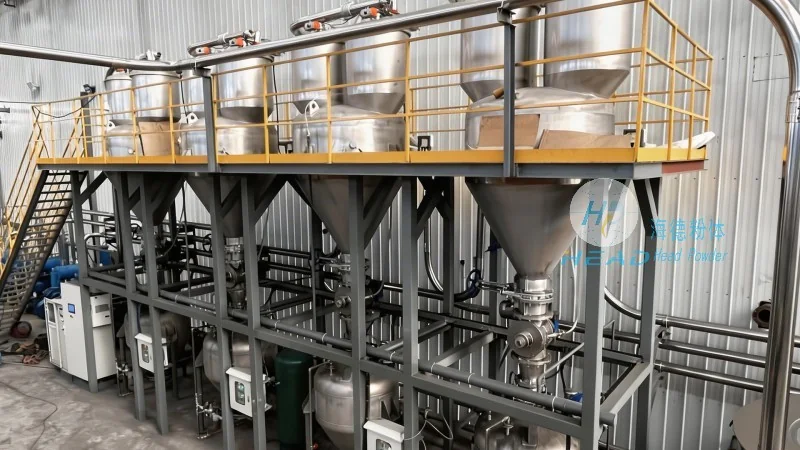
Rare earth pneumatic conveying systems are widely used in the processing and manufacturing of rare earth elements, which are critical components in various high-tech industries, including electronics, renewable energy, and automotive. The ability to transport these materials efficiently and safely is essential for maintaining production efficiency and meeting quality standards. HeadPowder's systems are tailored to meet the specific needs of these industries, providing solutions that enhance productivity while ensuring compliance with safety and environmental standards. By leveraging advanced engineering and material science, these systems contribute to the overall optimization of rare earth material handling processes, supporting the growth and sustainability of the industries that depend on them.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top