With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Wheat material pneumatic conveying systems are essential in modern grain handling and processing facilities. These systems efficiently transport wheat and other bulk materials from one location to another using air pressure or vacuum. The operation process and working principle of such systems are crucial for ensuring optimal performance, reliability, and efficiency in grain handling operations.
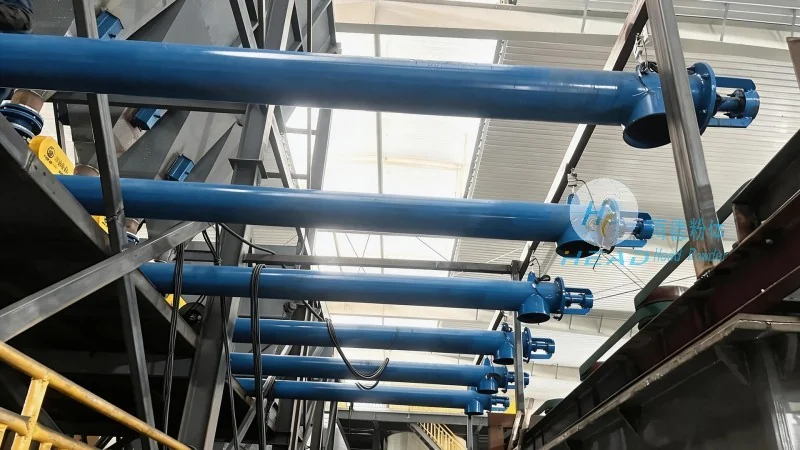
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of advanced pneumatic conveying equipment. With a strong presence in China, particularly in Shandong, the company specializes in designing, manufacturing, and installing customized wheat material conveying systems tailored to the specific needs of grain processing industries. Our expertise lies in delivering high-quality, reliable, and efficient solutions that meet the demanding requirements of modern agricultural and food processing applications.
The operation of a wheat material pneumatic conveying system involves several key steps that ensure smooth and continuous material transport. The process typically begins with the loading of wheat into the hopper or storage silo. From there, the material is drawn into the conveying line through a combination of air pressure and vacuum. The system uses a blower or compressor to generate the necessary air flow, which propels the wheat particles through the pipeline. The conveying line may include components such as bends, filters, and control valves to manage the flow and prevent blockages. The material is then discharged at the destination point, such as a processing unit or storage bin. Throughout the process, the system monitors air pressure, flow rate, and material level to maintain optimal performance and prevent system failures.
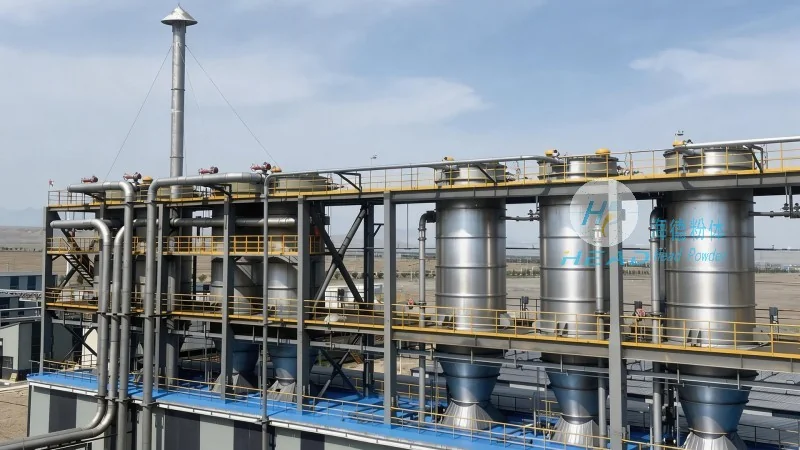
The working principle of a wheat material pneumatic conveying system is based on the principles of fluid dynamics and particle transport. The system utilizes a combination of positive pressure and negative pressure to move the wheat particles through the conveying line. In positive pressure systems, a blower or compressor creates an air stream that pushes the wheat particles forward. The air velocity is maintained at a level sufficient to keep the particles suspended and prevent them from settling or clogging the pipeline. In negative pressure systems, a vacuum is created at the discharge end, which draws the wheat particles into the conveying line. The system may also incorporate a combination of both positive and negative pressure, known as a mixed system, to achieve optimal conveying efficiency. The key components of the system include the hopper, conveyor line, air mover (blower or vacuum pump), and control valves. Each component plays a critical role in ensuring the smooth and efficient transport of wheat material.
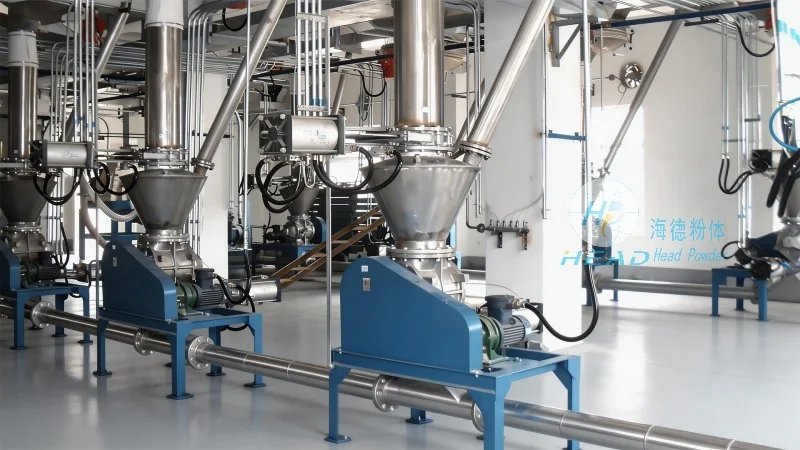
Wheat material pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. These systems are highly efficient in terms of energy consumption and material handling, as they minimize the need for manual labor and reduce the risk of material damage. The systems are also flexible and can be easily integrated into existing grain processing facilities, allowing for seamless expansion or modification of the conveying infrastructure. Additionally, pneumatic conveying systems are less prone to clogging and blockages compared to mechanical systems, which can lead to increased downtime and maintenance costs. The systems also provide better control over the material flow, allowing for precise regulation of the conveying rate and material distribution. Overall, the advantages of pneumatic conveying systems make them an ideal choice for modern wheat processing operations.
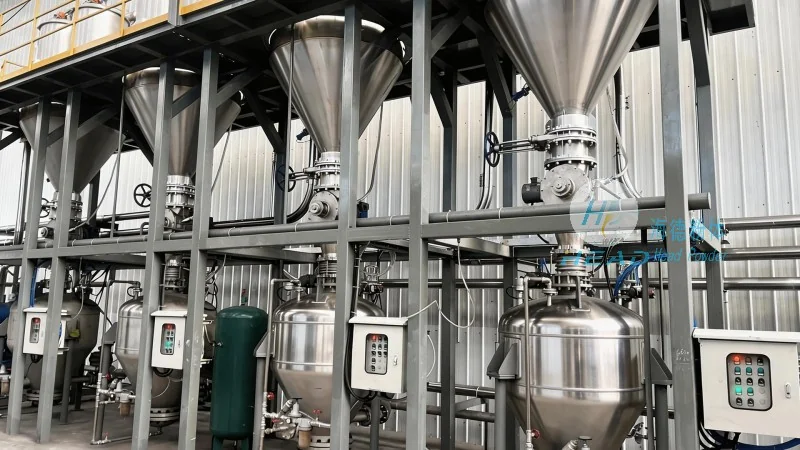
Wheat material pneumatic conveying systems are widely used in various applications within the grain processing industry. These systems are commonly employed in flour mills, where they transport wheat from storage silos to grinding and milling equipment. The systems are also used in feed mills, where they convey wheat to mixing and processing units. Additionally, pneumatic conveying systems are used in seed processing facilities, where they transport wheat seeds for cleaning, sorting, and packaging. The systems are also suitable for use in bulk handling operations, such as in ports and terminals, where they transport wheat from ships or trucks to storage facilities. The versatility and efficiency of pneumatic conveying systems make them a preferred choice for a wide range of wheat processing applications.
At Shandong HeadPowder Engineering Co., Ltd., we are committed to providing our customers with high-quality, reliable, and efficient wheat material pneumatic conveying systems. Our team of experienced engineers and technicians works closely with customers to understand their specific needs and design customized solutions that meet their requirements. We use advanced manufacturing techniques and high-quality materials to ensure the durability and longevity of our systems. Our products are rigorously tested and inspected to meet international standards and industry regulations. We also provide comprehensive after-sales support, including installation, maintenance, and repair services, to ensure that our customers receive the best possible service and support. With our strong presence in China and our commitment to quality, HeadPowder is the ideal partner for all your wheat material conveying needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top