With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced material handling systems. The company's focus on innovation and precision engineering has led to the creation of the Nitrogen Cycle Material Handling System, a sophisticated solution tailored for industries requiring controlled environments and efficient material transport. This system integrates cutting-edge technology to ensure optimal performance, safety, and reliability in various industrial applications.
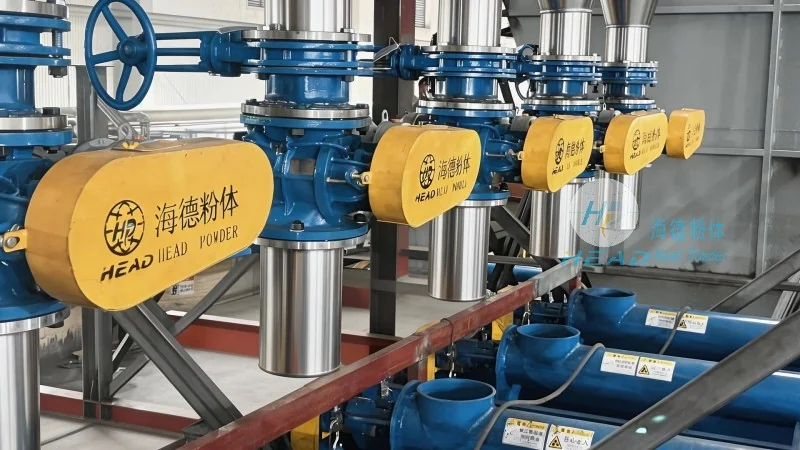
The Nitrogen Cycle Material Handling System is engineered to facilitate the seamless transfer of materials within industrial settings while maintaining a stable nitrogen atmosphere. This system is particularly valuable in sectors such as pharmaceuticals, food processing, and electronics manufacturing, where contamination control and process integrity are paramount. By utilizing nitrogen as a protective gas, the system creates an inert environment that prevents oxidation, moisture, and other contaminants from affecting the materials being handled. The design incorporates high-efficiency components, including vacuum pumps, nitrogen generators, and material handling units, all working in harmony to achieve precise control over the material flow and environmental conditions.
The Nitrogen Cycle Material Handling System comprises several critical components, each playing a vital role in the overall operation. The primary components include: (1) Nitrogen Generation Unit: This unit produces high-purity nitrogen gas, typically through pressure swing adsorption (PSA) or membrane separation technologies. The generated nitrogen is then filtered and dried to meet the required purity standards for the application. (2) Vacuum Pump System: The vacuum pump is responsible for creating a negative pressure within the material handling chamber, enabling the suction and transport of materials. The pump's performance directly impacts the system's ability to handle different material types and sizes. (3) Material Handling Unit: This component includes conveyor belts, hoppers, and feeding mechanisms that transport the materials from the source to the destination. The unit is designed to handle various material characteristics, such as bulk solids, powders, or granules, ensuring smooth and continuous operation. (4) Control System: The control system integrates sensors, valves, and programmable logic controllers (PLCs) to monitor and regulate the entire process. It ensures that the nitrogen flow, vacuum levels, and material transport are maintained within the specified parameters, providing real-time feedback and automated adjustments as needed.
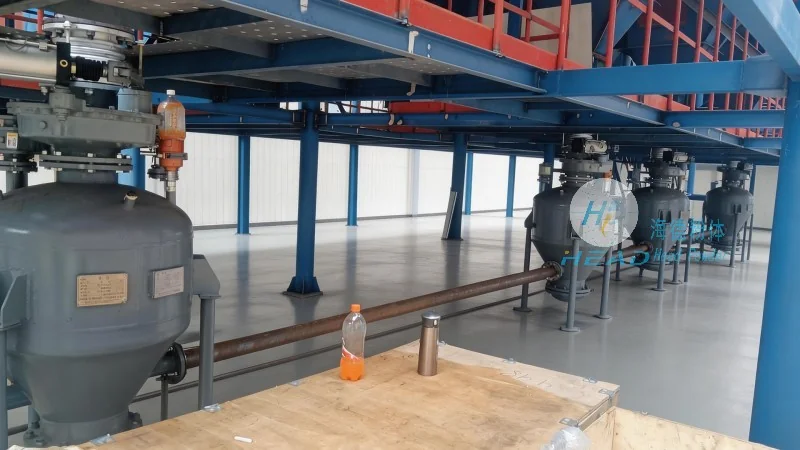
The operation of the Nitrogen Cycle Material Handling System follows a systematic sequence of steps to ensure efficient and safe material transport. The process begins with the preparation of the system, where the nitrogen generation unit produces the required amount of high-purity nitrogen. The nitrogen is then introduced into the material handling chamber, establishing an inert atmosphere. Simultaneously, the vacuum pump is activated to create a negative pressure, drawing the material from the source into the chamber. As the material is drawn in, it is conveyed through the material handling unit, which may include conveyor belts or screw conveyors, to the desired destination. The control system continuously monitors the nitrogen concentration, vacuum level, and material flow rate, adjusting the system parameters as necessary to maintain optimal conditions. Once the material has been successfully transported, the system can be reset for the next cycle, ensuring continuous operation without interruption.
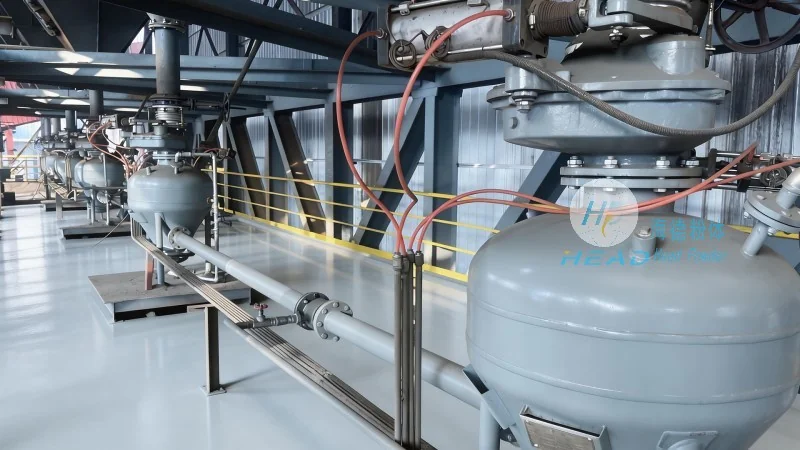
The working principle of the Nitrogen Cycle Material Handling System is based on the combination of nitrogen gas control and vacuum technology to achieve controlled material transport. The system operates by creating a pressure differential between the material source and the destination. The nitrogen gas is used to maintain a stable, low-oxygen environment within the transport chamber, preventing any oxidation or contamination of the materials. The vacuum pump then creates a negative pressure, which draws the material from the source into the chamber. The material is then moved through the handling unit, guided by the control system, to the target location. The system's design allows for precise control over the flow rate and direction of the material, ensuring that the transport process is efficient and reliable. Additionally, the system incorporates safety features, such as pressure sensors and emergency shut-off valves, to prevent any potential hazards during operation. This comprehensive approach ensures that the Nitrogen Cycle Material Handling System provides a robust and effective solution for industries requiring controlled material handling under inert conditions.
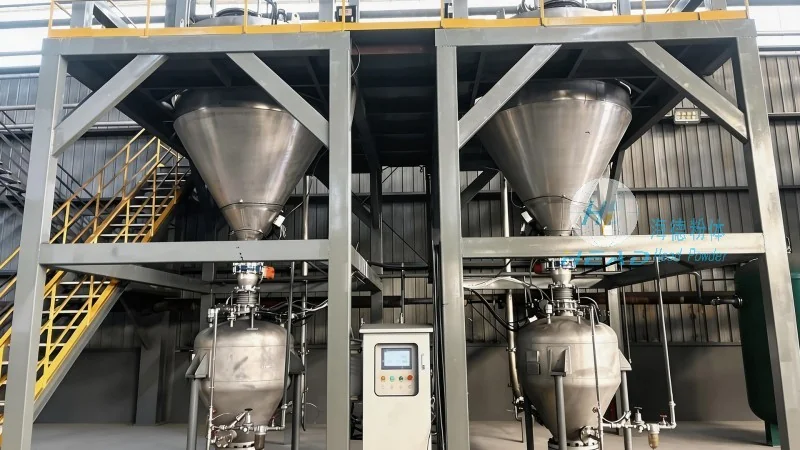
The Nitrogen Cycle Material Handling System offers numerous benefits to industries that require precise material transport in controlled environments. Some of the key advantages include: (1) Enhanced Material Protection: By maintaining a nitrogen atmosphere, the system protects sensitive materials from oxidation, moisture, and other contaminants, preserving their quality and integrity. (2) Improved Efficiency: The system's integrated design and automated control features reduce the need for manual intervention, leading to increased operational efficiency and reduced downtime. (3) Cost Savings: The use of nitrogen as a protective gas and the system's energy-efficient components contribute to lower operational costs over time. (4) Versatility: The system can handle a wide range of materials, including powders, granules, and bulk solids, making it suitable for various industrial applications. The Nitrogen Cycle Material Handling System is particularly beneficial in industries such as pharmaceutical manufacturing, where product purity is critical, and in food processing, where contamination control is essential. Additionally, it is widely used in electronics manufacturing to prevent dust and moisture from affecting sensitive components.
Shandong HeadPowder Engineering Co., Ltd. has developed the Nitrogen Cycle Material Handling System as a cutting-edge solution for industries requiring controlled material transport under inert conditions. Through its advanced design and integration of nitrogen generation, vacuum technology, and material handling components, the system provides a reliable and efficient means of transporting materials while maintaining a stable, contamination-free environment. The company's commitment to innovation and quality ensures that the system meets the highest industry standards, making it an ideal choice for businesses seeking to enhance their operational efficiency and product quality. With its headquarters in Shandong, China, HeadPowder continues to lead the way in providing advanced material handling solutions to meet the evolving needs of modern industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top