With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Coal and stone powder material handling systems are critical components in various industrial applications, designed to efficiently transport bulk materials like coal and stone powder. These systems leverage advanced engineering principles to ensure reliable, high-capacity material movement while maintaining operational safety and efficiency. The core of such systems lies in their ability to handle abrasive and fine materials, which are common in mining, power generation, and construction industries.
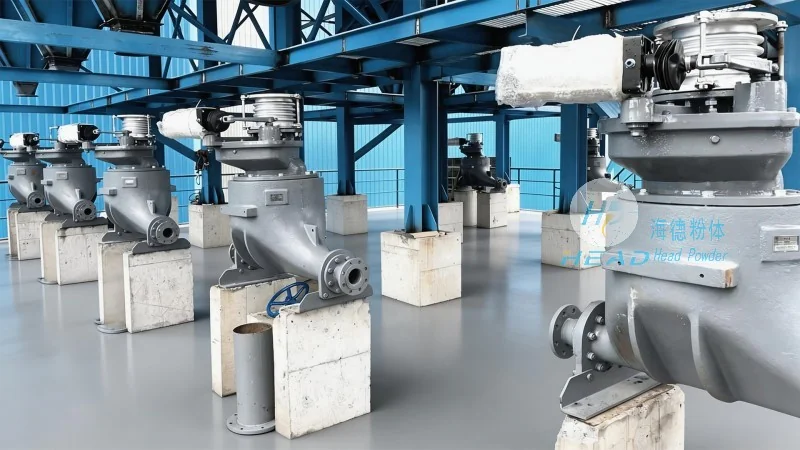
The fundamental principle of coal and stone powder material handling systems revolves around the integration of robust machinery and intelligent control technologies. These systems typically include components such as feeders, conveyors, and processing units, all working in tandem to achieve seamless material flow. For example, belt conveyors are widely used due to their high load capacity and adaptability to various environments. The system's design emphasizes minimal material degradation and energy efficiency, which are crucial for long-term operational costs and sustainability. Advanced materials and engineering techniques, such as wear-resistant coatings and optimized belt tensions, enhance the system's durability and performance under harsh conditions.
The working scene characteristics of coal and stone powder material handling systems are shaped by the diverse industrial environments they serve. In power plants, these systems are essential for transporting coal from storage to combustion units, ensuring a continuous fuel supply. The systems must handle large volumes of coal with precision, often under high-pressure and temperature conditions. In mining operations, the systems facilitate the movement of stone powder and other byproducts from extraction sites to processing facilities, supporting the extraction and processing chain. The operational environments vary from indoor industrial facilities to outdoor open-pit mines, requiring systems that can withstand extreme weather conditions, dust, and moisture. The adaptability of these systems to different working scenes is a key factor in their widespread adoption across industries.
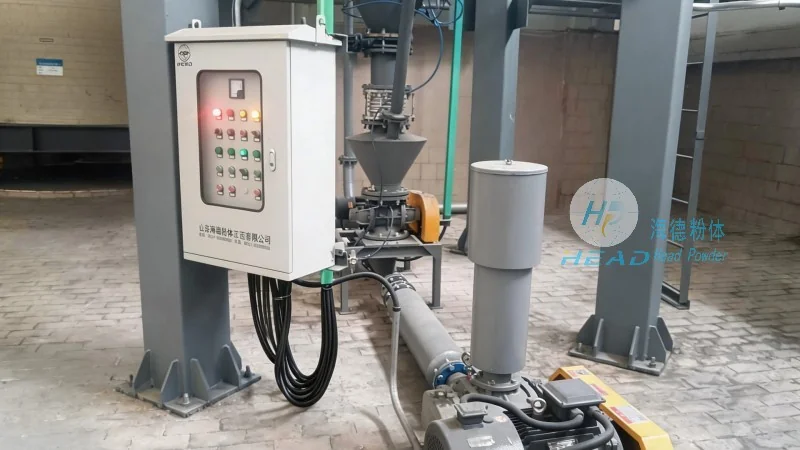
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing coal and stone powder material handling systems tailored to client needs. With a strong focus on innovation and quality, HeadPowder Engineering leverages decades of industry experience to deliver reliable and efficient systems. The company's commitment to customer satisfaction and operational excellence is reflected in its comprehensive service offerings, including system design, installation, and maintenance. HeadPowder Engineering's solutions are engineered to meet the specific requirements of industrial applications, ensuring optimal performance and longevity. The company's presence in China, particularly in Shandong, positions it as a trusted partner for businesses seeking advanced material handling technologies.
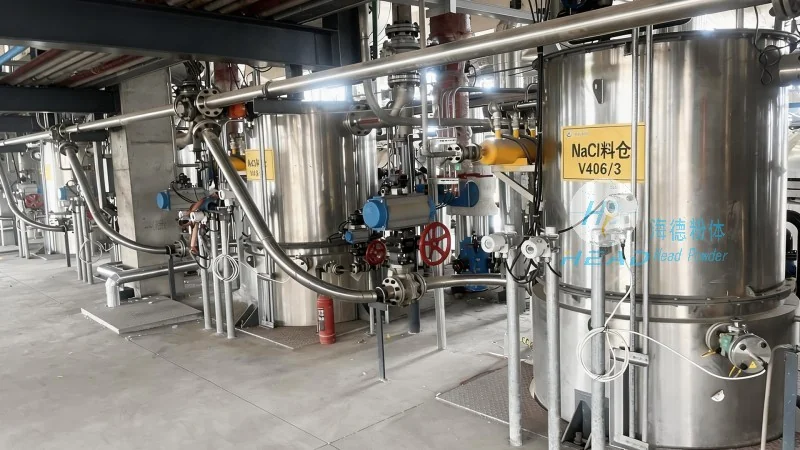
Coal and stone powder material handling systems offer several key features and advantages that make them indispensable in industrial settings. High capacity and continuous operation are primary benefits, enabling businesses to maintain production efficiency without interruptions. The systems are designed for durability, with components built to withstand the abrasive nature of coal and stone powder, reducing maintenance frequency and costs. Energy efficiency is another critical advantage, as modern systems incorporate advanced control mechanisms to minimize energy consumption while maximizing throughput. Additionally, these systems are equipped with safety features, such as overload protection and emergency stop functions, ensuring operational safety for personnel and equipment. The adaptability of the systems to different working conditions further enhances their utility, making them suitable for a wide range of industrial applications.
In conclusion, coal and stone powder material handling systems are essential for the efficient operation of industries that rely on bulk material transport. The systems' principles and working scene characteristics are tailored to meet the demands of various industrial environments, ensuring reliable and efficient material movement. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing advanced solutions that address the unique challenges of material handling in coal and stone powder applications. By leveraging innovative engineering and robust design, these systems contribute to improved productivity, reduced operational costs, and enhanced safety in industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top