With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries dealing with bulk powders, maintaining a clean and efficient material handling process is crucial. The dust-free bulk bag unloading station, often referred to as a bulk bag discharger or ton bag unloader, plays a pivotal role in ensuring safe and hygienic material transfer. This equipment is designed to handle large quantities of powders from super sacks or ton bags while minimizing dust generation and contamination. In this article, we explore the underlying principles of such systems and the specific operational scenarios where they excel.
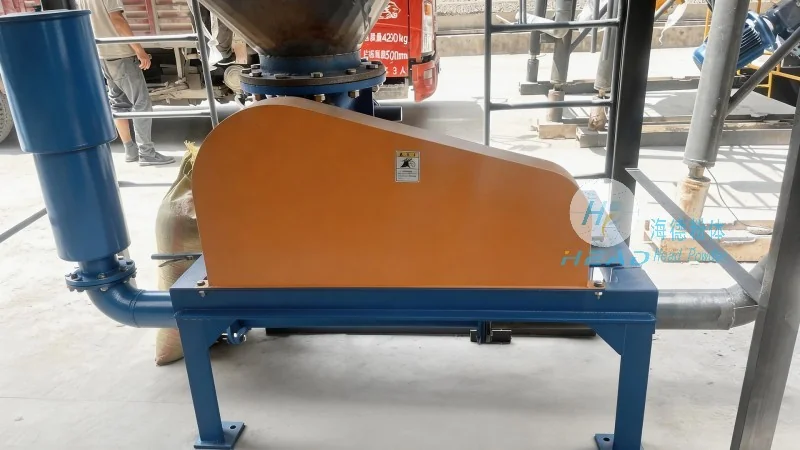
A dust-free bulk bag unloading station is a specialized piece of equipment used to transfer bulk powders from flexible containers like super sacks or ton bags into processing equipment or storage tanks. The primary goal of these systems is to achieve a completely sealed operation, preventing dust from escaping into the environment and ensuring that the material remains clean and free from contamination. This is particularly important in industries where product purity, worker safety, and regulatory compliance are paramount, such as pharmaceuticals, food processing, and chemical manufacturing.
The core of a dust-free bulk bag unloading station consists of several key components that work in tandem to achieve efficient and dust-free material transfer. The main elements include a hopper or receiving chamber, a discharge valve or gate, a vacuum or pressure system for air management, and a dust collection system. The process typically begins with the placement of a bulk bag into the receiving hopper. The bag is then secured, and the discharge valve is opened to allow the powder to flow into the system. Simultaneously, an air management system (either vacuum or pressure) is activated to create a negative or positive pressure environment, which helps to draw or push the powder through the system while preventing dust from escaping. These systems are designed and manufactured by Shandong HeadPowder Engineering Co., Ltd., ensuring high-quality construction and reliable performance.
One of the critical features is the dust collection system, which is usually integrated with the hopper and discharge area. This system uses filters or cyclones to capture any airborne particles, ensuring that the environment remains clean and safe for operators. The sealed design of the station also helps to maintain the integrity of the material, preventing moisture absorption or contamination from external sources. The working principle revolves around creating a controlled environment where the material is handled without exposing it to the open air, thus minimizing dust generation and ensuring a clean transfer process.
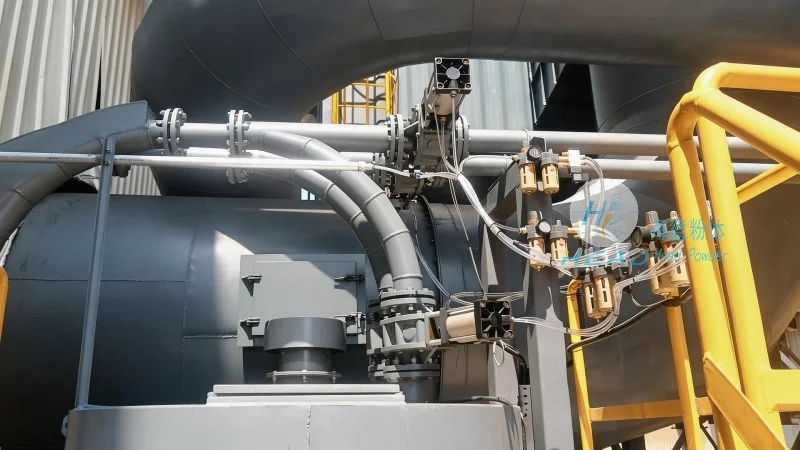
Dust-free bulk bag unloading stations are employed in a wide range of operational scenarios across various industries. In the pharmaceutical industry, for example, these systems are essential for handling active pharmaceutical ingredients (APIs) and other sensitive powders, where even trace amounts of contamination can affect product quality and safety. The sealed operation prevents cross-contamination and maintains the sterility of the material. Similarly, in the food processing sector, such as for flour, sugar, or dairy powders, the dust-free design ensures that the product remains free from dust and microbial contamination, meeting stringent food safety regulations.
In the chemical manufacturing industry, these stations are used for handling various chemical powders, including raw materials and intermediates. The ability to handle large quantities of powders efficiently while maintaining a clean environment is crucial for production continuity and worker safety. The systems are also adapted for use in industries like agriculture, where bulk fertilizers or pesticides are transferred from super sacks into processing equipment. Each application benefits from the consistent and reliable performance of the dust-free unloading station, which reduces downtime and improves overall operational efficiency.
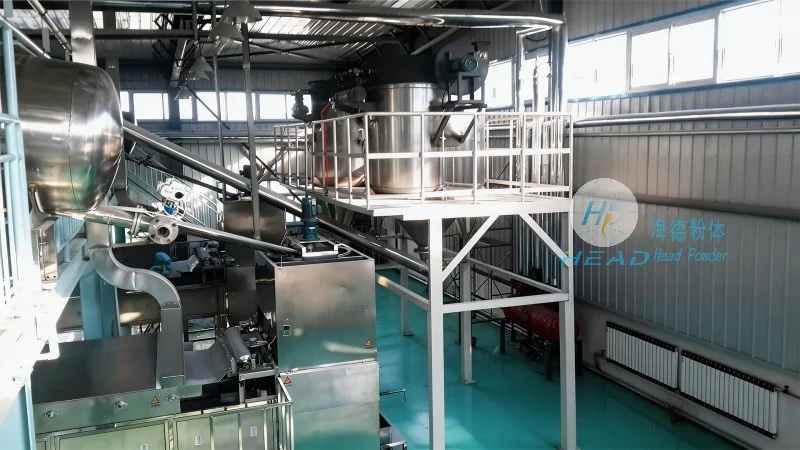
Implementing a dust-free bulk bag unloading station offers several advantages that enhance both operational efficiency and safety. First, the sealed design significantly reduces dust emissions, creating a safer working environment for employees and complying with environmental regulations. This is particularly important in industries where dust is a known health hazard, such as in the handling of silica or other respiratory irritants. Second, the system improves product quality by preventing contamination from dust, moisture, or other external factors. This is critical in industries where product purity directly impacts consumer trust and regulatory approval.
Third, the efficiency of bulk bag unloading is enhanced by the ability to handle large quantities of material in a short time. The automated or semi-automated operation reduces labor costs and minimizes the risk of human error during material transfer. Additionally, the sealed system reduces the need for additional cleaning and maintenance, as the material is handled in a controlled environment, reducing the risk of cross-contamination between batches. Overall, the dust-free bulk bag unloading station provides a cost-effective and reliable solution for bulk powder handling, improving both productivity and safety in the workplace.
In conclusion, the dust-free bulk bag unloading station is a vital piece of equipment for industries dealing with bulk powders. Its working principle, centered on sealed operation and integrated dust management, ensures efficient and safe material transfer. The operational scenarios where these systems are applied span multiple industries, from pharmaceuticals and food processing to chemical manufacturing and agriculture. The advantages, including improved safety, product quality, and operational efficiency, make the dust-free bulk bag unloading station an indispensable tool for modern material handling. As industries continue to prioritize clean and efficient processes, the demand for such equipment is likely to grow, further solidifying its role in the future of bulk powder handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top