With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider of advanced powder handling solutions, specializes in the design and manufacturing of metering bin pumps for efficient bulk material transport. This article explores the fundamental principles behind these systems and highlights key characteristics of their operational environments.
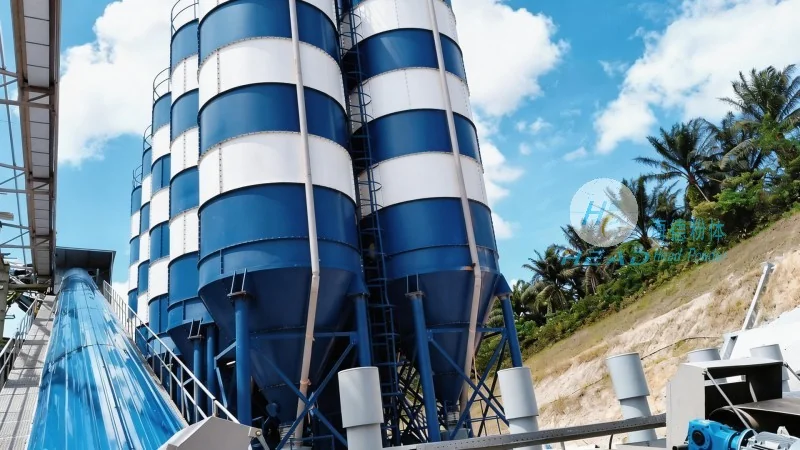
A metering bin pump operates on the principle of pneumatic conveying, where bulk powders are transported through a pipeline using compressed air or other gas. The pump itself is typically a vertical or horizontal cylinder equipped with a hopper at the top and a discharge outlet at the bottom. When the hopper is filled with material, the pump’s internal mechanism (such as a diaphragm or piston) is activated to create a pressure differential. This pressure change forces the powder to move from the hopper into the discharge line, ensuring a controlled and consistent flow rate. The metering function is achieved through precise control of the pump’s cycle time and pressure, allowing for accurate measurement and delivery of the material. This technology is particularly effective for materials that are difficult to handle with traditional methods, such as fine powders, granules, or cohesive substances.
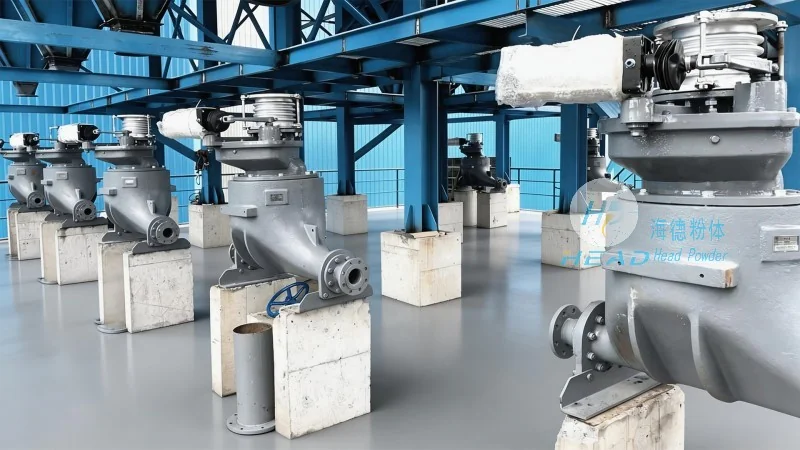
The operational environments for metering bin pumps vary widely across different industries, each presenting unique challenges and requirements. In the cement industry, for example, these pumps are used to transport raw materials like limestone and clinker from storage silos to production lines. The key characteristics here include high material throughput, durability to handle abrasive materials, and the ability to operate under high-pressure conditions. In the chemical industry, metering bin pumps are employed to handle reactive or hazardous powders, where precise dosing and containment are critical. The working scene characteristics in this sector emphasize safety, leak-proof design, and compliance with regulatory standards. For the food and pharmaceutical industries, the focus shifts to hygiene and cleanliness, with pumps constructed from stainless steel and featuring easy-to-clean components. These applications require strict control over particle size and moisture content, ensuring product quality and safety. Additionally, in the mining sector, metering bin pumps are used to transport ore and other bulk materials from mines to processing facilities, where the emphasis is on reliability and the ability to handle large volumes of material over extended periods.
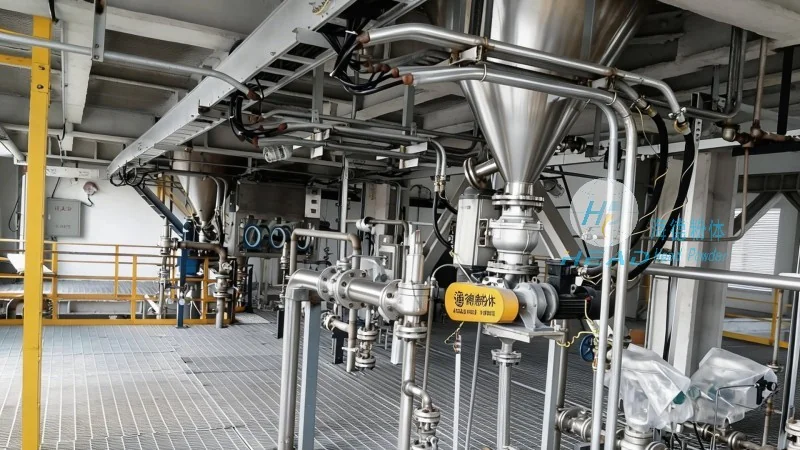
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a trusted name in the powder handling industry. With years of experience and a commitment to innovation, the company has developed cutting-edge metering bin pumps that meet the diverse needs of global clients. The company’s team of engineers and technicians works closely with customers to understand their specific requirements, from material properties to operational constraints, and designs customized solutions accordingly. HeadPowder’s products are known for their efficiency, reliability, and durability, making them a preferred choice for industries that demand high-performance bulk material handling systems. The company’s facilities in Shandong are equipped with state-of-the-art manufacturing equipment and quality control systems, ensuring that every product meets the highest standards of performance and safety. By combining technical expertise with customer-centric approach, HeadPowder continues to lead the way in providing advanced powder handling solutions for various industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top