

Principle and Working Scene Characteristics of Coconut Shell Powder Pneumatic Conveying System
Coconut shell powder, as a common industrial material, requires efficient and reliable conveying methods for processing and transportation. The pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., offers an advanced solution tailored to the unique properties of coconut shell powder. This system combines technology and practical application to ensure stable and efficient material handling in various industrial settings.
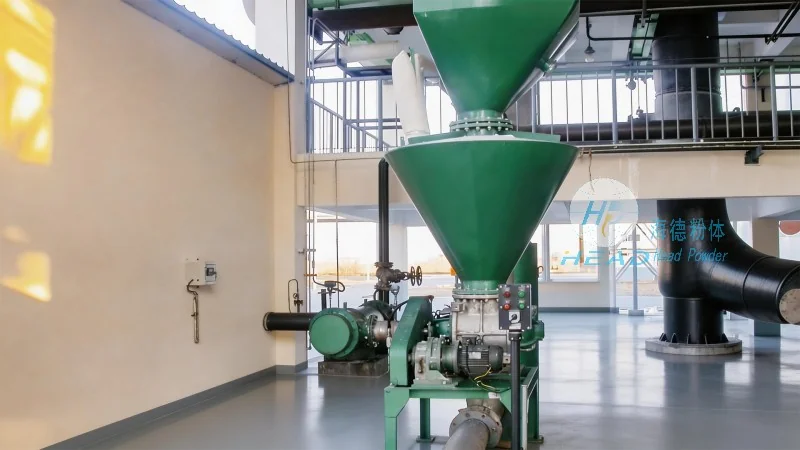
Principle of the Pneumatic Conveying System
The core principle of the coconut shell powder pneumatic conveying system is the use of air as the conveying medium to transport powder materials. By creating a pressure differential or using suction, the system can transport the powder from the source to the destination. The system typically includes components such as a hopper, a blower or vacuum pump, a pipeline network, and a receiving hopper. The operation involves feeding the coconut shell powder into the hopper, where it is then drawn into the pipeline by the air flow. The air flow carries the powder particles through the pipeline, delivering them to the desired location. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational efficiency.
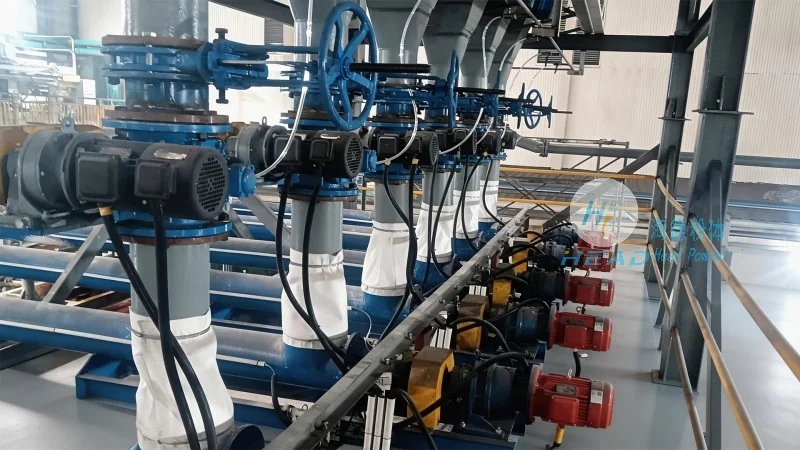
Key Components and Their Functions
The pneumatic conveying system for coconut shell powder consists of several critical components, each playing a vital role in the overall operation. The hopper serves as the storage and feeding unit, ensuring a consistent supply of powder to the system. The blower or vacuum pump generates the necessary air pressure or suction to move the powder through the pipeline. The pipeline network, made of durable materials like stainless steel or plastic, is designed to withstand the abrasive nature of coconut shell powder and maintain airtight integrity. The receiving hopper collects the delivered powder, completing the conveying process. Each component is carefully selected and integrated to ensure optimal performance and longevity.
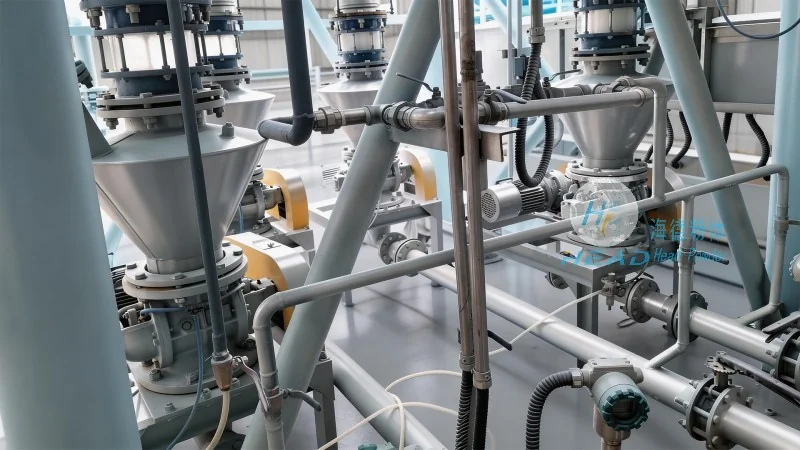
Working Scene Characteristics
The working scene characteristics of the coconut shell powder pneumatic conveying system are tailored to the specific needs of industrial applications. The system is suitable for environments where traditional mechanical conveying methods may be impractical or inefficient, such as in food processing, pharmaceuticals, or chemical industries. The system's ability to handle fine powders without segregation or agglomeration makes it ideal for applications requiring high purity and consistent quality. Additionally, the system is designed to minimize dust emissions and maintain a clean working environment, which is crucial in industries where hygiene is a priority. The flexibility of the system allows it to be adapted to various production scales, from small-scale operations to large industrial facilities.
Advantages of the System
Implementing the coconut shell powder pneumatic conveying system offers numerous advantages over traditional conveying methods. One of the primary benefits is the reduction in labor costs and maintenance requirements, as there are fewer mechanical parts involved. The system also provides better control over the material flow, ensuring consistent delivery rates and preventing material buildup or blockages. Another advantage is the improved safety and hygiene, as the enclosed pipeline system minimizes dust exposure and contamination risks. The system's adaptability to different powder characteristics and production volumes makes it a versatile solution for various industrial needs. Furthermore, the system's energy efficiency, particularly when using high-efficiency blowers, contributes to lower operational costs and environmental impact.
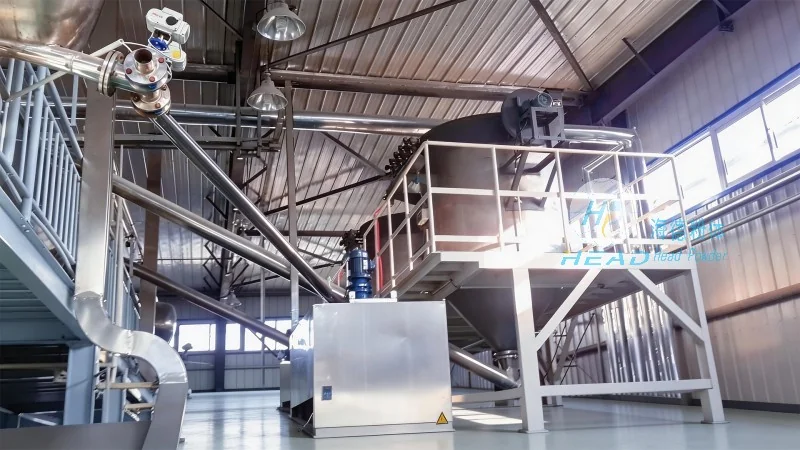
Application Examples
The coconut shell powder pneumatic conveying system is widely used in various industrial applications. For instance, in the food industry, it is employed to transport coconut shell powder for use in food products or as a raw material in other processing steps. In the chemical industry, the system is utilized to convey the powder for manufacturing or processing purposes, ensuring precise control over the material flow. The system is also applicable in the pharmaceutical sector, where the hygienic design and dust-free operation are essential for maintaining product quality and safety. Each application leverages the system's ability to handle fine powders efficiently and maintain a clean environment, aligning with industry standards and regulations.