With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications requiring efficient and flexible material handling, the suction-pressure mixed material pneumatic conveying system has emerged as a reliable solution. This technology combines the advantages of both suction and pressure pneumatic conveying methods, offering enhanced performance and versatility in transporting various bulk materials. In this article, we will explore the working principle and key features of this advanced system, highlighting its applications and benefits in modern industrial processes.
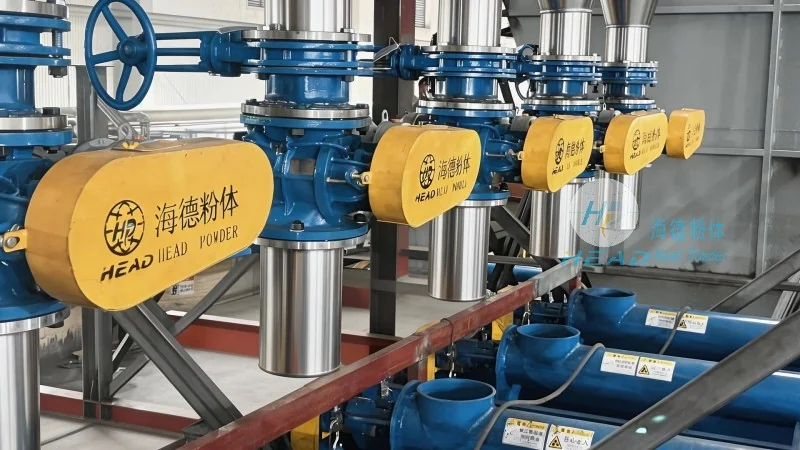
The suction-pressure mixed material pneumatic conveying system is designed to transport dry bulk materials over short to medium distances. It integrates the capabilities of both suction and pressure conveying, allowing for flexible operation based on the specific requirements of the material being handled. This system is particularly suitable for industries such as food processing, pharmaceuticals, chemicals, and minerals, where material purity and low contamination are critical.
The operation of the suction-pressure mixed material pneumatic conveying system involves a combination of negative and positive pressure stages. The process typically begins with the material being drawn into the system using a vacuum source, which creates a low-pressure environment at the material inlet. This stage is known as the suction phase, where the material is aspirated from the source and mixed with the conveying air. The mixed material-air stream then moves through the conveying line under the influence of the vacuum, transporting the material to the first pressure stage.
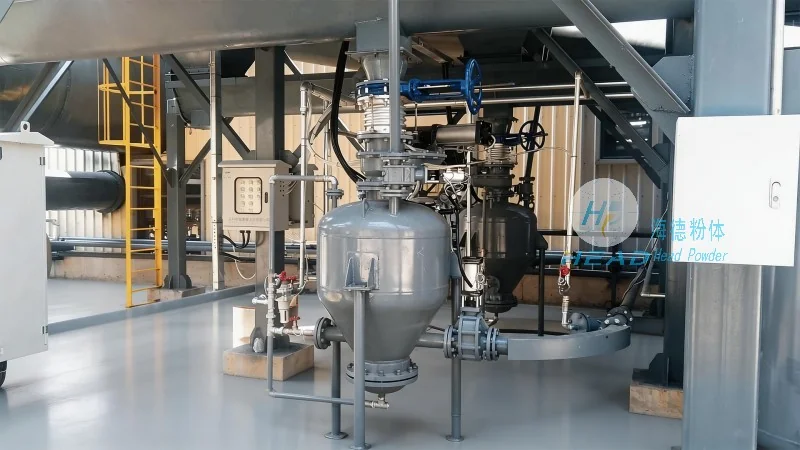
At the pressure stage, the vacuum is replaced by a positive pressure boost, which increases the velocity of the material-air mixture and propels it to the destination point. This dual-stage approach ensures efficient material transport while minimizing energy consumption and maintaining the integrity of the material. The system utilizes a series of components, including a material hopper, a vacuum pump, a pressure booster, and a conveying line, all working in tandem to achieve the desired conveying performance.
One of the primary advantages of this system is its ability to handle a wide range of materials, including powders, granules, and fine particles. The mixed suction-pressure operation allows for gentle material handling, reducing the risk of product degradation or agglomeration. Additionally, the system offers high conveying efficiency, with minimal material loss and low maintenance requirements. The modular design of the system enables easy integration into existing industrial setups, making it a cost-effective solution for material handling needs.
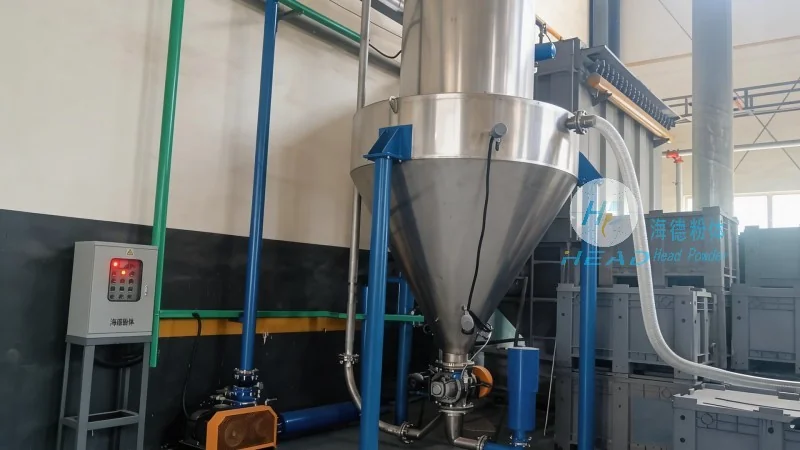
The suction-pressure mixed material pneumatic conveying system also provides flexibility in terms of conveying distance and material flow rate. By adjusting the vacuum and pressure levels, operators can control the speed and volume of material transport, adapting to varying production demands. This adaptability makes the system suitable for both batch and continuous production processes, ensuring consistent performance and reliability.
The versatility of the suction-pressure mixed material pneumatic conveying system makes it applicable in numerous industrial sectors. In the food industry, it is used for transporting ingredients such as flour, sugar, and spices, maintaining hygiene and preventing contamination. In the pharmaceutical sector, the system ensures the safe and sterile handling of active pharmaceutical ingredients (APIs) and other sensitive materials. The chemical industry utilizes this technology for transporting powders and granules, such as pigments, catalysts, and reagents, while the minerals industry benefits from efficient material transport in mining and processing operations.
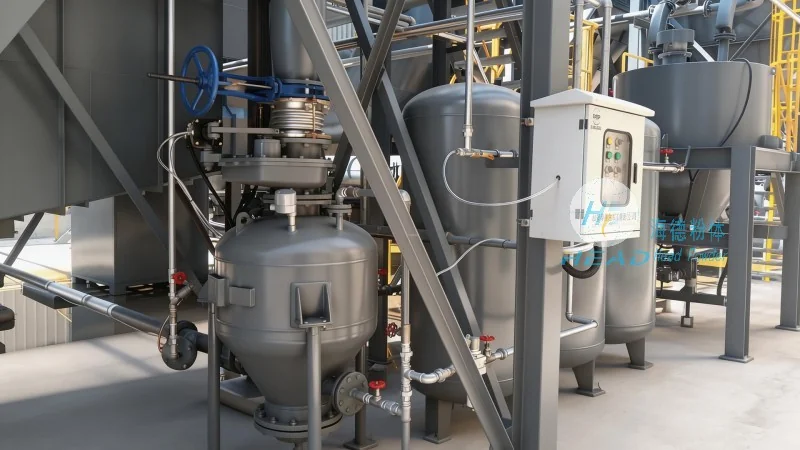
Furthermore, the system is ideal for applications requiring dust-free and enclosed material handling, as it operates within a sealed system, preventing dust emissions and protecting the environment. This feature is particularly important in industries where regulatory compliance and environmental standards are stringent.
The suction-pressure mixed material pneumatic conveying system represents a sophisticated solution for modern material handling challenges. By combining the strengths of suction and pressure conveying, it offers enhanced efficiency, flexibility, and reliability in transporting bulk materials. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of various industries. With a focus on innovation and quality, HeadPowder ensures that its systems meet the highest standards of performance and durability, providing long-term value to its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top