With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer specializing in the design, development, and production of advanced powder handling equipment. Based in Shandong, China, the company has established itself as a leading provider in the field of pneumatic conveying systems, particularly those utilizing nitrogen protection for enhanced safety and efficiency in powder transport. This article delves into the working principle and key features of nitrogen-protected powder pneumatic conveying equipment, highlighting how such systems address the unique challenges of handling sensitive or reactive powders.
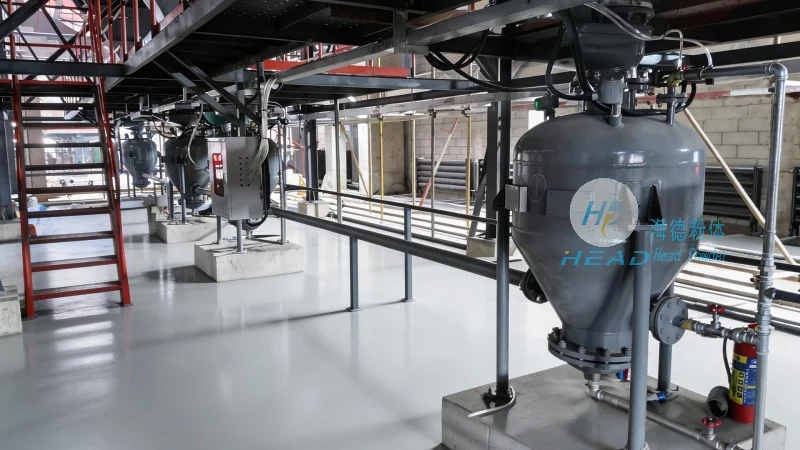
The core of nitrogen-protected powder pneumatic conveying equipment lies in its ability to create a sealed, inert environment for powder transport. The system operates by using compressed nitrogen gas to displace air from the conveying line, effectively preventing the introduction of oxygen or moisture that could degrade the powder or cause safety hazards. The process typically involves several key components working in tandem:
First, a hopper or storage vessel holds the powder material. A rotary valve or feeder then controls the flow of powder into the conveying line. Compressed nitrogen is introduced into the system, often through a pressure regulator and filter to ensure purity. The nitrogen gas then flows through the conveying line, carrying the powder particles along with it. The system may include pulse jets or venturi nozzles to enhance the mixing and transport of the powder, ensuring consistent flow rates and preventing blockages. At the destination, the powder is discharged into a receiving hopper or container, while the nitrogen gas is either recycled or safely vented.
Several distinct features set nitrogen-protected powder pneumatic conveying systems apart from conventional pneumatic conveying solutions. These features are designed to address the specific needs of industries dealing with sensitive, explosive, or moisture-sensitive powders:
1. Complete Inertization: The primary feature is the creation of a fully nitrogen-filled conveying line, which eliminates oxygen and moisture from the transport environment. This is critical for preventing oxidation, combustion, or moisture-related degradation of the powder, ensuring that the material remains in its original state throughout the conveying process.
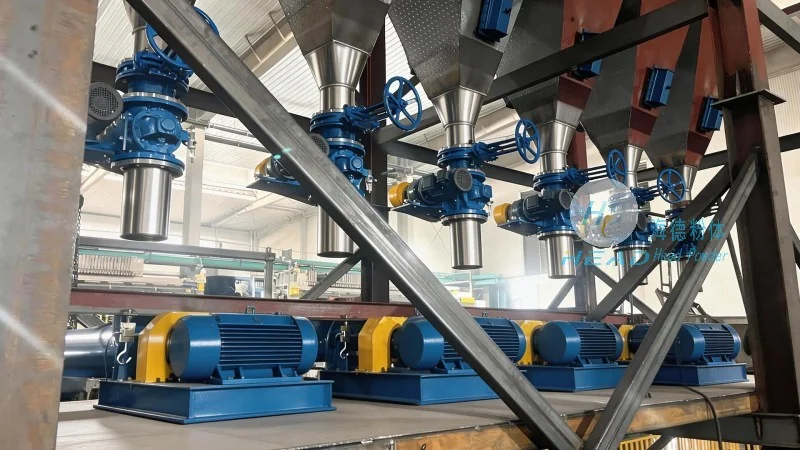
2. Enhanced Safety: By replacing air with nitrogen, the risk of dust explosions is significantly reduced. Nitrogen is an inert gas, which does not support combustion, making the system safer for handling flammable or explosive powders. This is particularly important in industries such as pharmaceuticals, food processing, and chemical manufacturing, where safety is paramount.
3. Improved Powder Quality: The sealed environment prevents contamination from external sources, such as dust, moisture, or other particles. This ensures that the powder maintains its purity and quality, which is essential for applications where product consistency is critical, like in pharmaceuticals or high-value food products.
4. Efficient Material Handling: The system offers high conveying efficiency with minimal pressure drop, allowing for long-distance transport of powders with minimal energy consumption. The use of nitrogen as the conveying medium ensures consistent flow rates, reducing the need for frequent maintenance or adjustments.
5. Customizable Design: Nitrogen-protected systems can be tailored to meet the specific requirements of different applications. This includes adjustable conveying rates, variable nitrogen pressure, and modular components that can be integrated into existing production lines. The design flexibility allows for adaptation to various powder types and processing needs.
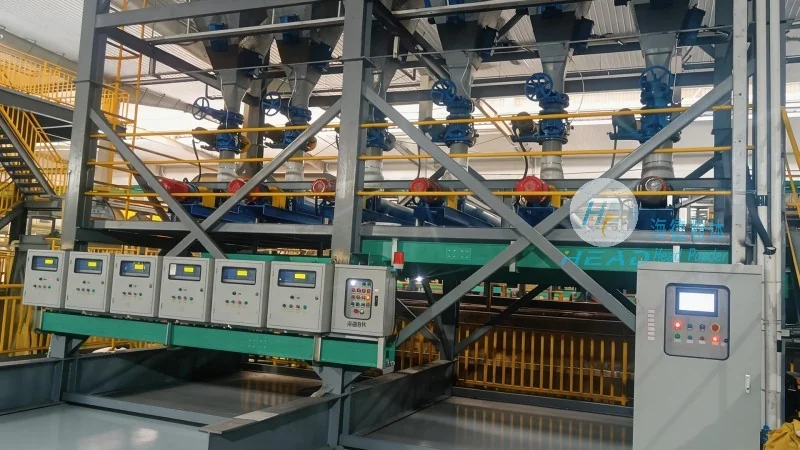
The versatility of nitrogen-protected powder pneumatic conveying equipment makes it suitable for a wide range of industries. Some of the key applications include:
1. Pharmaceutical Industry: For handling active pharmaceutical ingredients (APIs) and other sensitive powders that require strict contamination control and safety measures. The inert environment ensures that the drug substance remains pure and stable, meeting regulatory standards.
2. Food and Beverage Industry: For conveying ingredients such as sugar, flour, spices, and other food powders. The nitrogen protection prevents moisture absorption and oxidation, preserving the flavor, color, and nutritional value of the products.
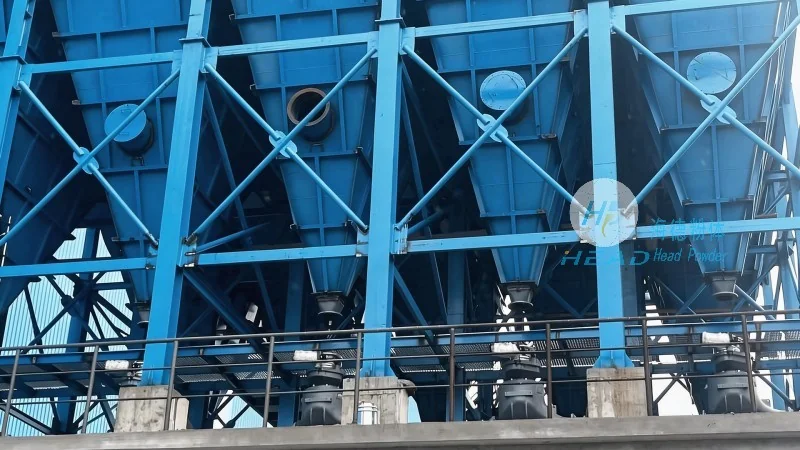
3. Chemical Industry: For transporting flammable or reactive chemicals, where the risk of explosion or reaction with air is high. The nitrogen-protected system provides a safe and reliable method for handling these materials.
4. Mineral and Mining Industry: For conveying fine powders from processing plants, such as coal, limestone, or other minerals. The system ensures efficient transport while maintaining the integrity of the material.
5. Plastics and Rubber Industry: For handling polymer powders and additives, where moisture and oxygen can affect the quality of the final product. The nitrogen protection helps maintain the material's properties and prevent degradation.
For industries dealing with sensitive or hazardous powders, nitrogen-protected powder pneumatic conveying equipment offers a superior solution compared to traditional air-based systems. The combination of enhanced safety, improved powder quality, and efficient material handling makes it an essential component in modern processing facilities. By leveraging the expertise of manufacturers like Shandong HeadPowder Engineering Co., Ltd., companies can implement reliable and effective powder transport systems that meet their specific operational and regulatory requirements. The investment in such equipment not only improves process efficiency but also ensures compliance with safety standards, ultimately contributing to the long-term success and sustainability of the business.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top