With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for mineral sand and powder materials. This article provides an in-depth exploration of the working principle and key features of such systems, highlighting their efficiency and reliability in material handling applications.
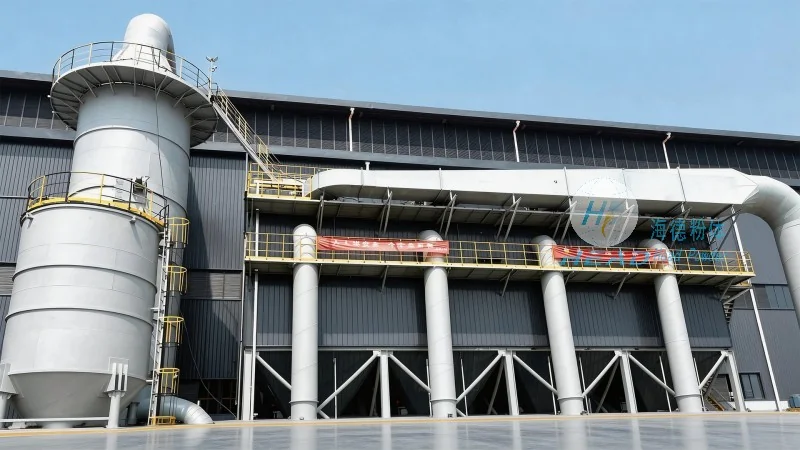
Pneumatic conveying systems are essential for transporting dry, fine materials like mineral sand over short to medium distances. These systems utilize air or gas as the conveying medium to move particles through a pipeline network. The technology offers a flexible and efficient solution for industries dealing with bulk powder handling, ensuring minimal product degradation and reduced operational costs compared to traditional methods like belt conveyors or bucket elevators.
The core operation of a mineral sand powder pneumatic conveying system involves several key steps. First, the material is fed into a hopper or feeder, where it is then introduced into a pipeline. A fan or blower generates a high-velocity airflow within the pipeline, which lifts and transports the mineral sand particles. The system typically operates under either positive pressure (pressure conveying) or negative pressure (vacuum conveying), depending on the specific application requirements. Positive pressure systems are commonly used for long-distance or high-capacity transport, while vacuum systems are ideal for short distances or when material needs to be drawn from multiple sources.
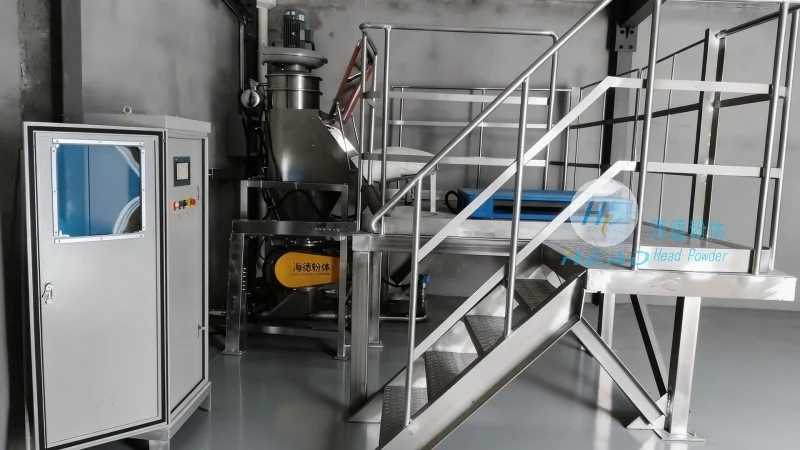
HeadPowder's pneumatic conveying systems for mineral sand powder offer several distinct advantages that make them a preferred choice in various industrial settings. One of the primary features is the ability to handle fine and abrasive materials without causing excessive wear or degradation. The enclosed pipeline design minimizes dust emissions, enhancing workplace safety and compliance with environmental regulations. Additionally, these systems provide excellent control over material flow, allowing for precise dosing and batching, which is crucial in processes like mixing, blending, and packaging.
Effective mineral sand powder pneumatic conveying systems rely on a combination of specialized components, each playing a critical role in the overall operation. The main components include the feeder or hopper for material input, the fan or blower to generate airflow, the pipeline network for material transport, and the receiver or discharge hopper for material collection. Other essential components may include filters to remove dust from the exhaust air, pressure relief valves to prevent over-pressurization, and control valves to regulate airflow and material flow. Each component is carefully designed and integrated to ensure optimal performance and longevity of the system.
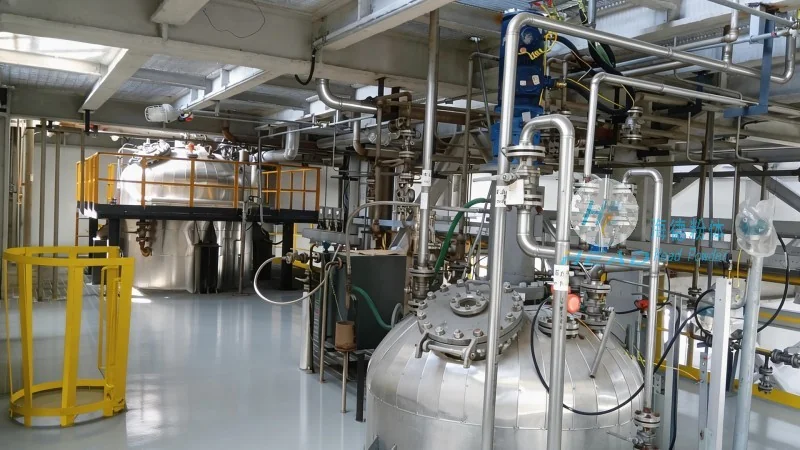
Mineral sand powder pneumatic conveying systems are widely used across multiple industries, including mining, construction, and chemical processing. In mining operations, they are used to transport crushed ore and sand from processing plants to storage facilities or for further processing. In the construction industry, these systems facilitate the handling of sand and other aggregates for concrete production and road construction. The chemical industry also benefits from such systems for transporting fine powders like minerals and additives in manufacturing processes. The versatility of the system makes it adaptable to various material types and operational conditions.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of advanced pneumatic conveying solutions tailored to the needs of mineral sand and powder handling industries. By leveraging their expertise in system design and engineering, HeadPowder delivers efficient, reliable, and cost-effective solutions that enhance operational productivity and safety. The company's commitment to quality and innovation ensures that their pneumatic conveying systems meet the highest standards, providing long-term value to clients across various sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top