With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications involving calcium hydroxide, efficient material handling is crucial. The systems designed for this purpose are engineered to ensure safe, reliable, and consistent transport of the material. This article explores the working principles and key features of such equipment, providing insights into how these systems operate and what makes them effective in various industrial settings.
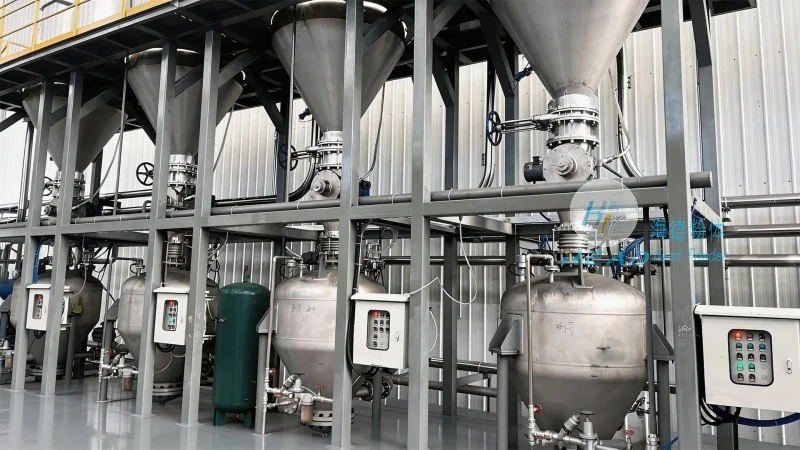
The core working principle of calcium hydroxide material handling systems revolves around the integration of mechanical components to facilitate the movement of the material from one location to another. Typically, these systems utilize a combination of conveyors, pumps, or specialized transport mechanisms tailored to the physical properties of calcium hydroxide. The process begins with the material being loaded into a storage or feeding unit. From there, it is transferred through a series of stages, including feeding mechanisms, transport lines, and discharge points. The design ensures minimal material degradation and loss, maintaining the integrity of the calcium hydroxide throughout the handling process. Control systems are often integrated to regulate the flow rate and pressure, ensuring optimal performance and safety. This systematic approach allows for consistent and efficient material movement, which is essential for maintaining production efficiency in industrial operations.
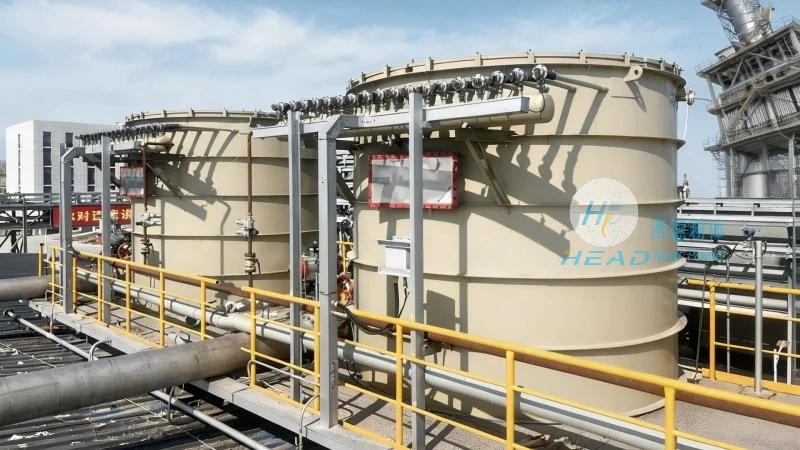
Several key features distinguish effective calcium hydroxide material handling systems. First, durability and corrosion resistance are critical, as calcium hydroxide can be abrasive and may interact with certain materials. High-quality materials, such as stainless steel or specialized coatings, are used to construct the equipment, ensuring longevity and minimal maintenance. Second, the systems are designed for safety, incorporating features like overfill protection, leak detection, and emergency stop mechanisms. These safety measures are vital in industrial environments where material handling involves potential hazards. Third, the equipment is often equipped with adjustable speed controls and variable flow capabilities, allowing operators to adapt the system to different production needs. This flexibility enhances operational efficiency and reduces downtime. Additionally, many systems include monitoring and diagnostic tools, enabling real-time tracking of performance and early detection of issues. These features collectively contribute to the reliability and effectiveness of calcium hydroxide material handling equipment.
The design of calcium hydroxide material handling systems is often tailored to specific industrial applications. For example, in manufacturing processes where calcium hydroxide is used as a raw material, the system may include specialized feeding hoppers and conveyor belts to handle bulk quantities. In construction or agricultural applications, the equipment might be designed for outdoor use, with weather-resistant components and protective enclosures. The choice of transport method—such as pneumatic conveyors, screw conveyors, or hydraulic systems—depends on the material's characteristics and the distance it needs to be moved. Each application requires careful consideration of factors like material flow rate, pressure requirements, and environmental conditions. By addressing these specific needs, the systems can be optimized for maximum performance and minimal operational challenges.
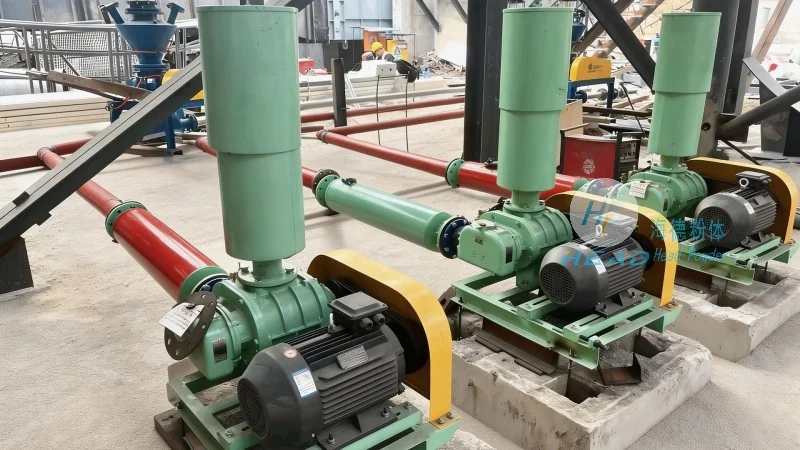
Calcium hydroxide material handling systems are essential components in industries that rely on this chemical for various applications. Understanding their working principles and key features is vital for selecting and maintaining effective equipment. The systems' durability, safety features, and adaptability make them suitable for a wide range of industrial settings. As technology advances, these systems continue to evolve, incorporating more efficient control mechanisms and materials to enhance performance. For businesses dealing with calcium hydroxide, investing in well-designed material handling equipment is crucial for maintaining productivity and ensuring operational safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top