With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Vacuum suction material handling systems represent a sophisticated approach to transporting bulk materials efficiently and safely. These systems are widely utilized across various industries, including food processing, pharmaceuticals, and chemical manufacturing, due to their ability to handle a diverse range of materials while maintaining high standards of hygiene and operational efficiency.
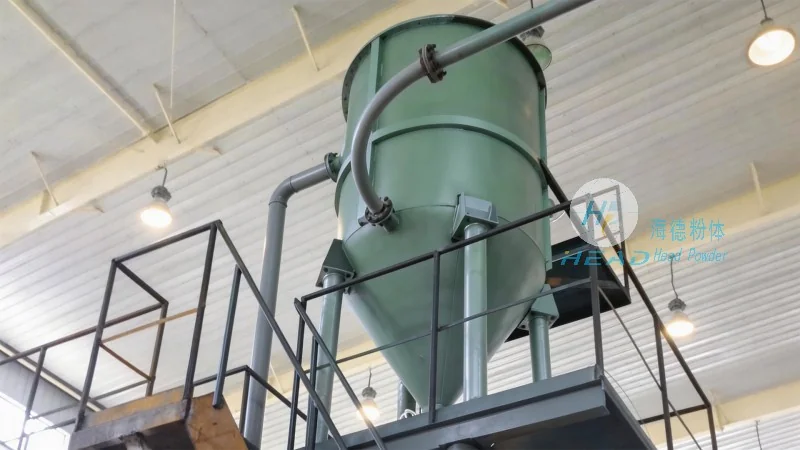
The fundamental operation of a vacuum suction material handling system relies on the creation of a negative pressure environment. At the heart of this technology is a vacuum pump, which draws air from the system, thereby reducing pressure inside the suction pipe and the material container. This pressure differential causes the material to be drawn into the pipe and transported to the destination point. The process typically involves several key components: a vacuum pump, suction nozzles or hoses, a material container, and a discharge mechanism. The vacuum pump generates the necessary suction force, while the nozzles or hoses are strategically placed to capture the material from the source. The material is then conveyed through the pipeline under the influence of the vacuum, and finally discharged at the receiving end. This method eliminates the need for mechanical contact with the material, reducing contamination risks and enabling the handling of delicate or sensitive products.
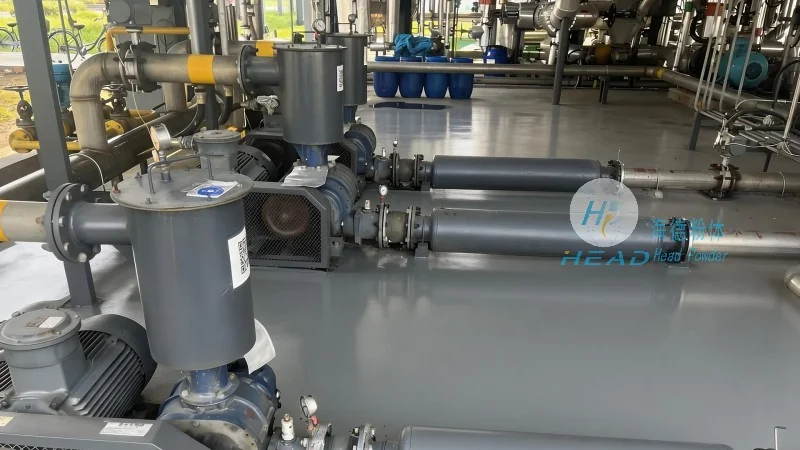
One of the most prominent features of vacuum suction systems is their ability to handle a wide variety of materials, from powders and granules to small particles and even liquids in some configurations. This versatility makes them suitable for applications where traditional conveying methods may be less effective or even unsuitable. Another critical feature is the system's environmental friendliness. Unlike positive pressure systems that may release dust or particles into the air, vacuum suction systems operate by drawing material into the system, thus minimizing dust emissions and improving workplace air quality. This is particularly beneficial in industries where air quality regulations are stringent. Additionally, vacuum suction systems offer enhanced safety features. By eliminating the need for moving parts in direct contact with the material, the risk of material spillage or contamination is significantly reduced. The enclosed system design also helps in preventing dust from spreading, contributing to a safer working environment. From an operational perspective, these systems are known for their energy efficiency. The vacuum pump operates at lower pressures compared to positive pressure systems, leading to reduced energy consumption and lower operational costs over time. Furthermore, the design allows for easy integration with existing production lines, making it a flexible solution for various industrial setups.
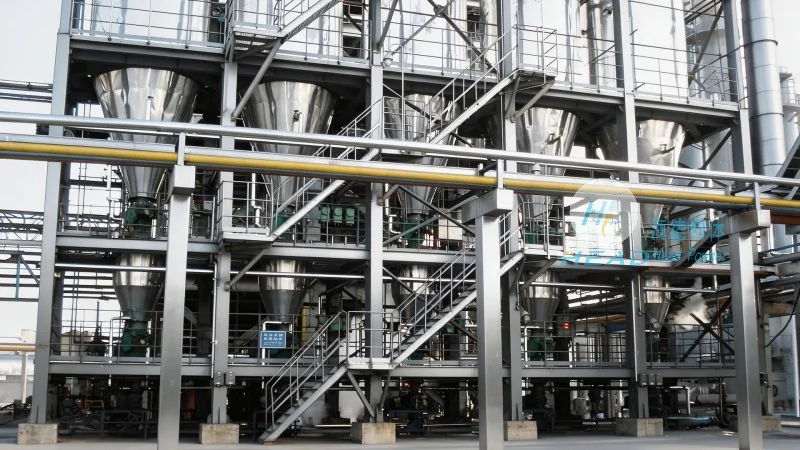
Vacuum suction material handling systems find extensive applications across multiple sectors. In the food and beverage industry, they are commonly used for transporting ingredients such as flour, sugar, and spices, ensuring that the products remain uncontaminated and maintain their quality. The pharmaceutical industry also relies on these systems for handling active pharmaceutical ingredients (APIs) and other sensitive materials, where hygiene and purity are paramount. In the chemical industry, vacuum suction systems are employed to transport powders and granules, providing a safe and efficient method to move materials that may be hazardous or reactive. Other industries, including agriculture and mining, also utilize these systems for material handling tasks, leveraging their ability to handle bulk materials in a controlled manner.
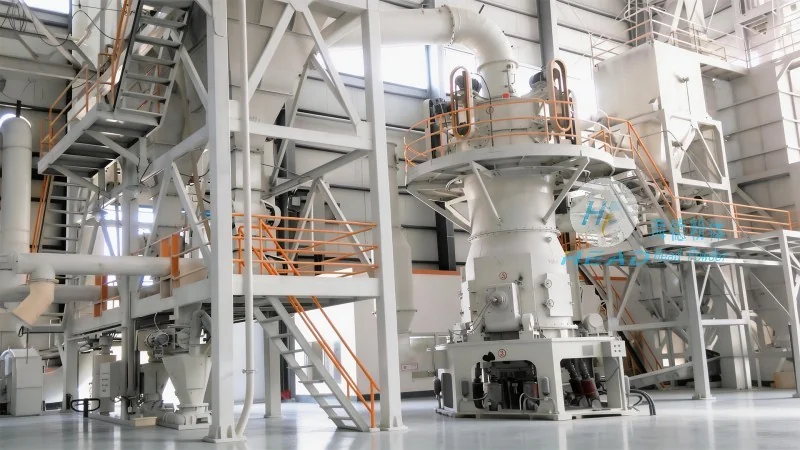
As a leading provider of material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing vacuum suction material handling systems tailored to meet the diverse needs of various industries. With a strong commitment to quality and innovation, the company has established itself as a trusted partner in the field of bulk material transport. HeadPowder's systems are engineered to deliver reliable performance, ensuring that clients achieve optimal efficiency and safety in their material handling operations. The company's expertise lies in understanding the unique requirements of each application and providing customized solutions that enhance productivity while maintaining compliance with industry standards. HeadPowder's dedication to customer satisfaction and technological advancement has positioned it as a key player in the global material handling market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top