With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications involving the handling of silicate powders, efficient and reliable conveying systems are essential to ensure smooth operations and maintain product quality. The silicate powder conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is designed to address the unique challenges associated with transporting these materials, which often include high moisture content, abrasive properties, and varying particle sizes. This equipment is engineered to provide a robust solution for industries such as ceramics, glass, and construction materials, where the consistent and safe movement of silicate powders is critical.
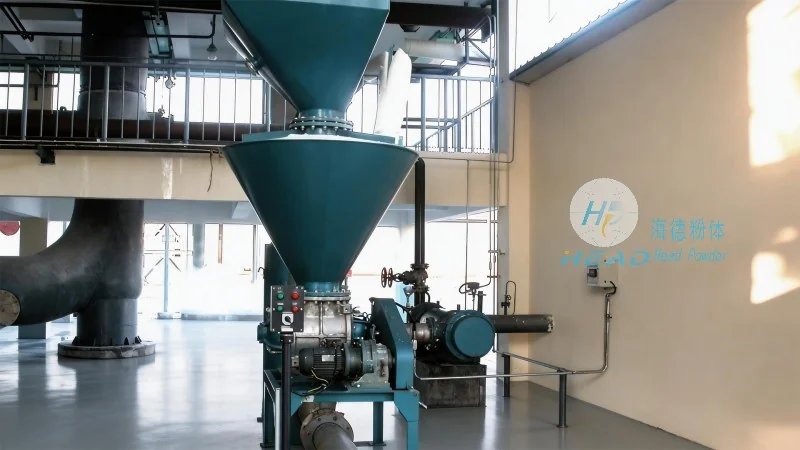
The core of the silicate powder conveying system lies in its integrated design, which combines advanced components to achieve efficient material transport. The system typically operates through a combination of mechanical and pneumatic mechanisms, allowing for both bulk and fine powder handling. A key component is the hopper, which serves as the initial storage and feeding unit, ensuring a steady supply of material to the conveyor. The hopper is equipped with a feeding valve or screw feeder that controls the flow rate, preventing overloading and maintaining consistent pressure within the system. As the material moves from the hopper into the conveyor, it is propelled through a series of pipes or ducts, often using air or mechanical force. The conveying mechanism may include a positive displacement blower or a screw conveyor, depending on the specific application requirements. This design allows for precise control over the flow rate and pressure, minimizing material degradation and ensuring that the silicate powders are transported without clogging or segregation. The system also incorporates a dust collection and filtration unit to maintain air quality and prevent contamination, which is particularly important for applications where product purity is paramount.
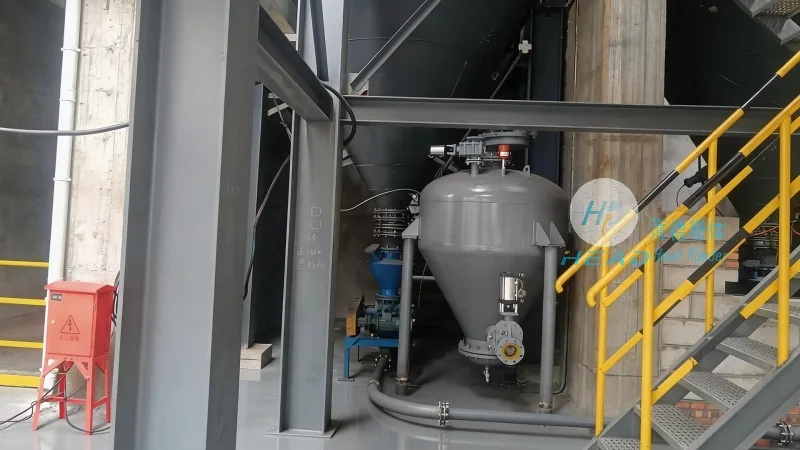
Shandong HeadPowder Engineering Co., Ltd. has incorporated several advanced features into their silicate powder conveying system to enhance performance and reliability. One of the primary features is the adjustable flow control system, which allows operators to modify the conveying rate based on real-time operational needs. This flexibility is crucial for adapting to varying production schedules or material characteristics. The system also includes a built-in monitoring and alarm system that detects issues such as blockages, pressure drops, or abnormal temperature changes. These alerts enable timely maintenance, reducing downtime and preventing potential equipment damage. Another notable feature is the corrosion-resistant construction, which is essential for handling silicate powders that may be acidic or contain abrasive particles. The materials used in the construction, such as stainless steel and high-grade plastics, ensure long-term durability and minimal maintenance. Additionally, the system is designed for easy integration with existing production lines, with modular components that can be customized to fit specific space constraints or operational requirements. This adaptability makes it suitable for a wide range of industrial settings, from small-scale manufacturing to large-scale production facilities.
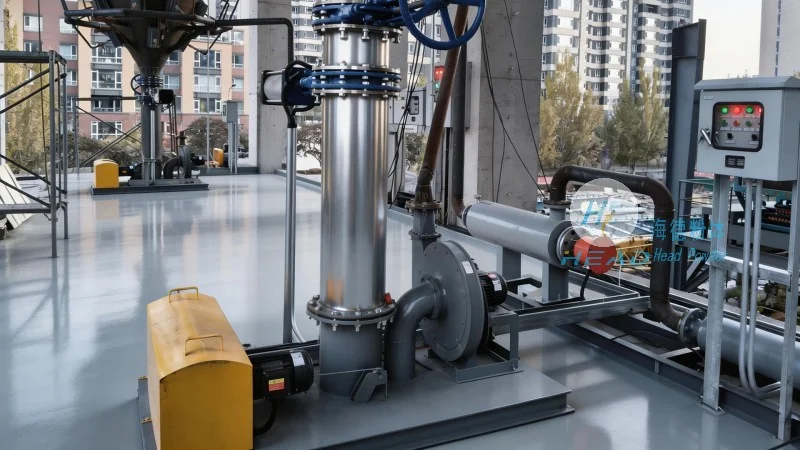
The implementation of the silicate powder conveying system offers numerous benefits for industrial operations. Firstly, it significantly improves material handling efficiency by reducing the time and labor required for manual transport. The automated system ensures consistent and reliable delivery of powders, minimizing the risk of human error and product contamination. Secondly, the system enhances product quality by preventing segregation and degradation during transport. The controlled environment and gentle handling of the materials maintain the integrity of the silicate powders, which is vital for applications where particle size and uniformity are critical. Thirdly, the system contributes to operational cost savings through reduced maintenance and energy consumption. The energy-efficient design and durable construction lower long-term operational expenses, while the monitoring system helps identify and address issues before they escalate into costly breakdowns. Furthermore, the system promotes workplace safety by eliminating the need for manual handling of powders, reducing the risk of respiratory issues or other health hazards associated with dust exposure. This not only protects the workforce but also complies with safety regulations, ensuring a secure working environment.
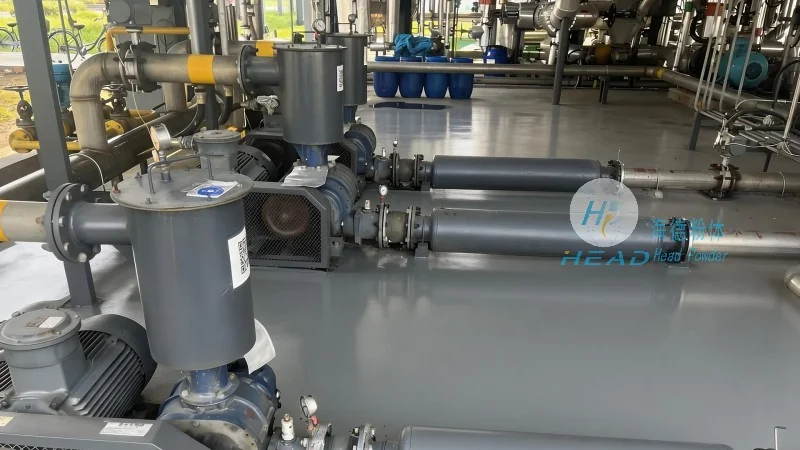
In conclusion, the silicate powder conveying system equipment from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated solution for the efficient and reliable handling of silicate powders. By integrating advanced mechanical and pneumatic components, the system addresses the unique challenges of transporting these materials while maintaining product quality and operational efficiency. The key features, including adjustable flow control, monitoring systems, and corrosion-resistant construction, ensure that the equipment is both versatile and durable. The benefits of using this system extend beyond improved productivity, encompassing cost savings, enhanced safety, and consistent product quality. For industries that rely on silicate powders, this equipment provides a reliable and effective means of material transport, supporting their operational needs and contributing to overall success.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top