With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the operational mechanics and distinctive attributes of sodium sulfate powder conveying systems is crucial for industries dealing with bulk solid handling. These systems are engineered to efficiently transport sodium sulfate, a widely used chemical in various industrial applications, from storage to processing units. The design and functionality of such systems are tailored to meet the specific demands of material flow, ensuring reliability and efficiency in chemical processing operations.
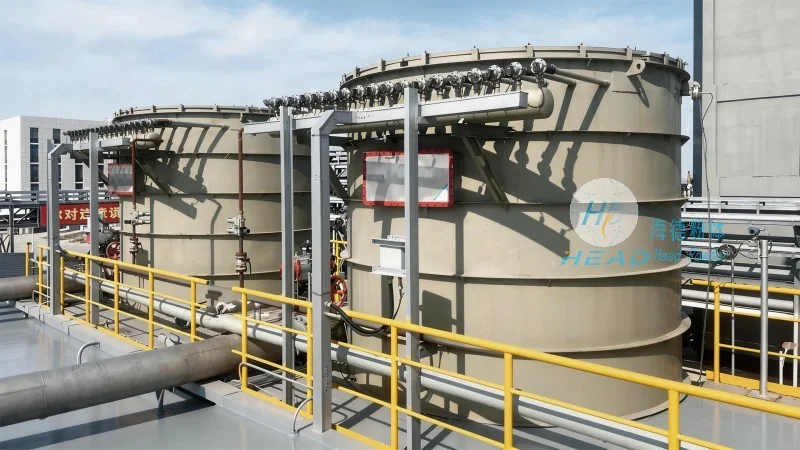
The core working principle of sodium sulfate powder conveying systems revolves around the movement of bulk material through a network of components designed to handle fine powders. Typically, these systems utilize pneumatic or mechanical methods to transport the powder. In pneumatic conveying systems, compressed air is used to create a flow that propels the sodium sulfate particles through pipes. This method is particularly effective for long-distance and high-volume transport, as it minimizes material degradation and contamination. Mechanical conveying systems, on the other hand, employ screw conveyors, belt conveyors, or bucket elevators to move the powder. These systems are often preferred for shorter distances or when the material requires gentle handling to prevent agglomeration or breakage.
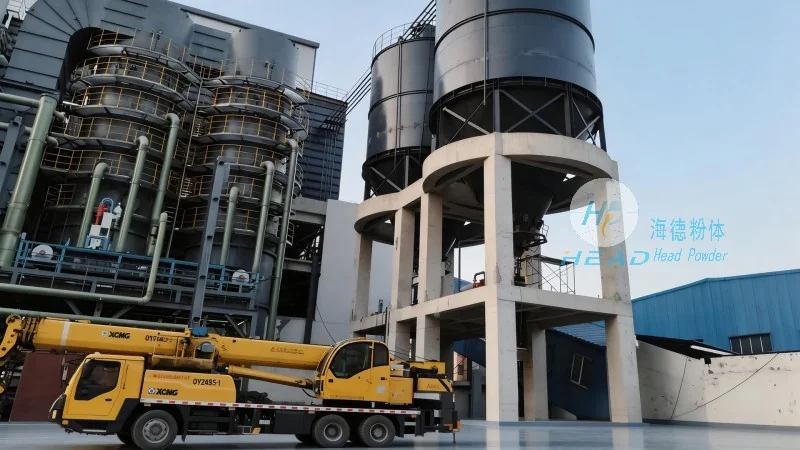
Key components in a typical sodium sulfate powder conveying system include a hopper for material storage, a feeder to control the flow rate, a conveying line (such as pipes or conveyor belts), and a receiver for the discharged material. The system operates by first loading the sodium sulfate into the hopper, where it is then fed into the conveying line. The feeder ensures a consistent and controlled flow, preventing overloading or underloading that could affect system performance. The conveying line transports the powder to the destination, where it is collected in the receiver. This process is often automated, with sensors and control systems monitoring the flow rate, pressure, and other parameters to maintain optimal operation.
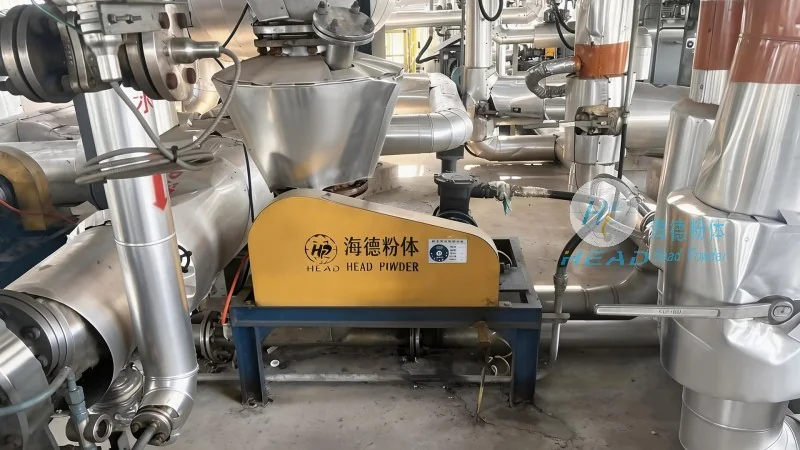
Sodium sulfate powder conveying systems are characterized by several key features that enhance their performance and suitability for industrial applications. One of the primary features is their ability to handle fine powders without causing clogging or blockages. This is achieved through the use of specialized materials and designs that prevent material buildup in the conveying lines. For instance, some systems employ self-cleaning mechanisms or adjustable screw speeds to maintain smooth material flow. Another important feature is the system's efficiency in terms of energy consumption and operational costs. Modern conveying systems are designed to minimize energy usage while maximizing throughput, making them cost-effective for large-scale operations. Additionally, these systems offer flexibility in terms of layout and integration with existing processing facilities. They can be customized to fit specific space constraints and can be integrated with other equipment, such as mixers or reactors, to form a comprehensive material handling solution.
Another notable feature is the system's ability to maintain material quality and purity. Sodium sulfate is often used in applications where contamination is unacceptable, such as in food processing or pharmaceutical manufacturing. Therefore, conveying systems are designed with sanitary and cleanable components to prevent cross-contamination. This includes materials like stainless steel, which are resistant to corrosion and easy to clean. The system also incorporates features like dust collection and filtration to ensure that the powder remains free from contaminants and that the air is clean and safe for the environment. Furthermore, the systems are equipped with safety features to prevent accidents and ensure operator safety. These may include emergency stop buttons, pressure relief valves, and monitoring systems that alert operators to any abnormalities in the system's operation.
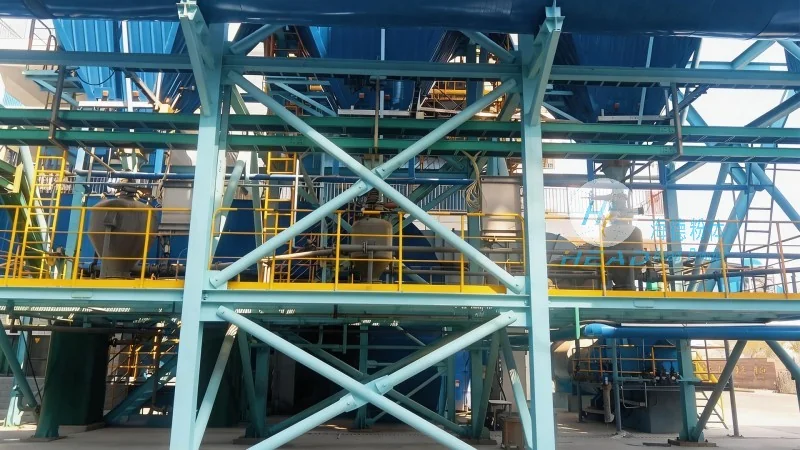
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced powder handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing sodium sulfate powder conveying systems tailored to the needs of various industries. HeadPowder's expertise lies in understanding the unique challenges of bulk solid handling and developing customized solutions that enhance operational efficiency and reliability. The company is based in Shandong, China, and operates state-of-the-art facilities equipped with cutting-edge technology and adheres to strict quality control standards to ensure that all products meet the highest industry standards. HeadPowder serves a wide range of clients, including chemical manufacturers, food processors, and pharmaceutical companies, providing them with reliable and efficient powder conveying systems that meet their specific requirements. The company's commitment to customer satisfaction and technological advancement has established it as a trusted partner in the powder handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top