With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Ammonia fertilizer material handling systems are critical components in modern agricultural and industrial operations, designed to efficiently transport and manage ammonia-based fertilizers from production to application. These systems ensure the safe and reliable movement of potentially hazardous materials while optimizing operational efficiency and minimizing environmental impact. Understanding the core design principles behind such systems is essential for engineers, farmers, and industry professionals to maximize performance and safety.
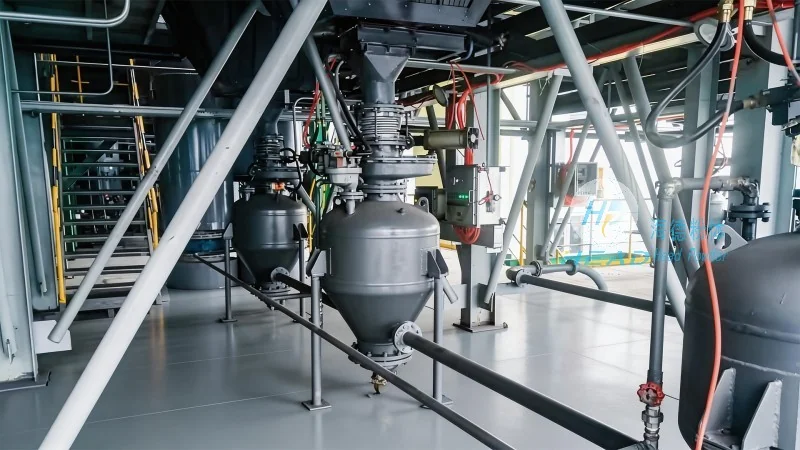
Ammonia fertilizer material handling systems are specialized equipment and infrastructure used to transport, store, and distribute ammonia-based fertilizers. These systems are integral to the agricultural supply chain, as ammonia is a key raw material in the production of nitrogen-based fertilizers, which are vital for crop growth and food security. The systems must adhere to strict safety standards due to ammonia's corrosive and toxic properties, making design and implementation a complex process that balances functionality with regulatory compliance.
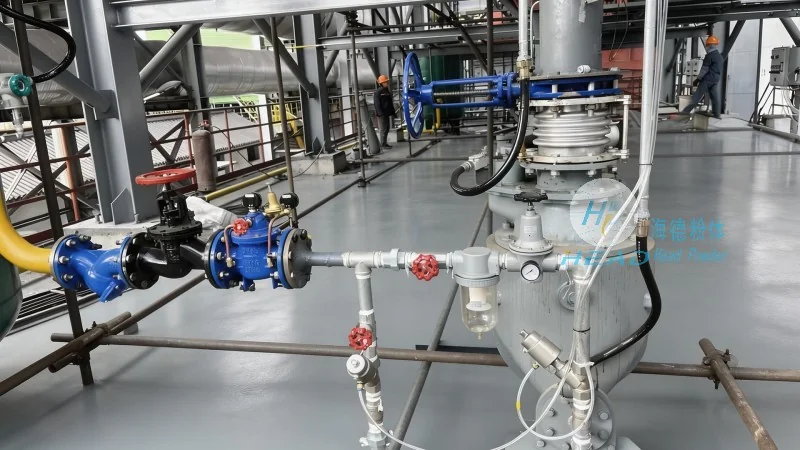
The design of ammonia fertilizer material handling systems is guided by several fundamental principles to ensure safety, efficiency, and durability. First, material compatibility is paramount. Components such as pipes, valves, and storage tanks must be constructed from materials that resist corrosion from ammonia and its byproducts, such as urea or ammonium salts. Common materials include stainless steel, special alloys, and lined carbon steel, which provide long-term resistance to chemical attack. Second, pressure and temperature control is critical. Ammonia is often stored and transported under pressure, and temperature fluctuations can affect its physical properties and safety. Systems incorporate pressure relief valves, temperature sensors, and insulated piping to maintain stable conditions and prevent accidents. Third, segregation and containment is essential to prevent cross-contamination and environmental spills. The design includes double-walled storage tanks, leak detection systems, and emergency shutdown procedures to mitigate risks. Finally, ergonomics and operational efficiency are considered to minimize human error and maximize productivity. Systems are designed with user-friendly controls, automated processes, and clear signage to ensure safe and efficient operation.
Ammonia fertilizer material handling systems typically consist of several key components that work in tandem to achieve their objectives. The primary components include: storage tanks, which are used to store bulk ammonia or its derivatives; transfer pumps, which move the material from storage to processing or distribution points; pipelines and fittings, which transport the material through the system; valves and controls, which regulate flow and pressure; and monitoring and safety systems, which detect leaks, pressure changes, and other hazards. Each component is carefully selected and integrated to ensure seamless operation and compliance with safety regulations.
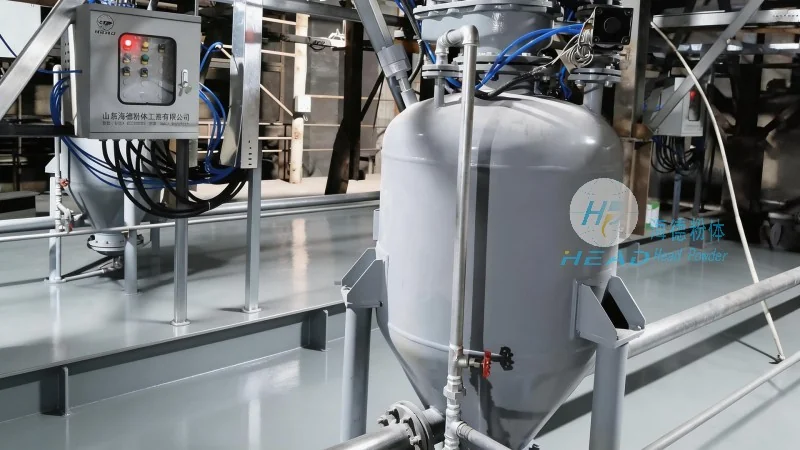
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions in the fertilizer industry, specializes in the design, manufacturing, and installation of ammonia fertilizer material handling systems. With years of experience and a commitment to quality, HeadPowder has become a trusted partner for agricultural and industrial clients seeking reliable and efficient systems. The company's expertise lies in customizing solutions to meet specific client needs, ensuring that systems are tailored to operational requirements, safety standards, and budget constraints. HeadPowder's team of engineers and technicians work closely with clients to understand their unique challenges and develop innovative solutions that enhance performance and safety. The company's facilities are located in Shandong, China, where it leverages local resources and expertise to deliver high-quality products and services.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top