With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial operations that involve handling magnesium sulfate heptahydrate, a specialized piece of equipment is often required to ensure efficient and safe powder transport. This equipment, commonly known as the magnesium sulfate heptahydrate powder conveying system, is designed to manage the movement of this specific chemical compound from one location to another within a production facility. The system is crucial for maintaining the quality and integrity of the material, especially given the hygroscopic nature of magnesium sulfate heptahydrate, which can absorb moisture from the air and affect its properties.
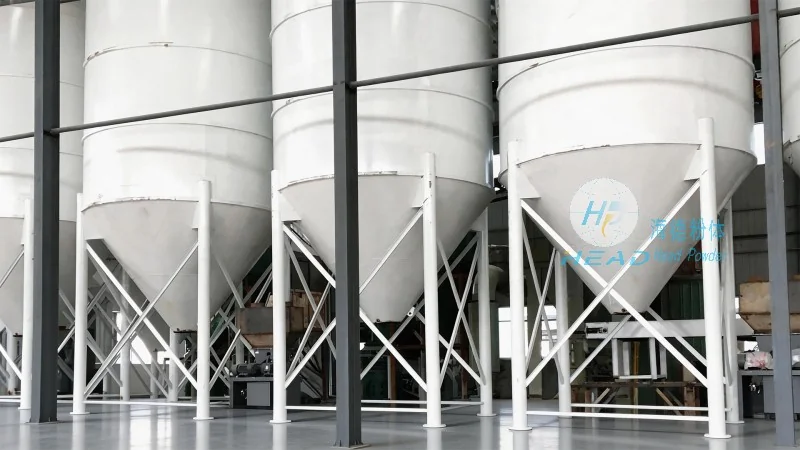
Developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, this powder conveying equipment is engineered to meet the demands of various industrial applications. The system is tailored to handle the unique characteristics of magnesium sulfate heptahydrate, such as its fine particle size and tendency to clump or agglomerate. By incorporating advanced design features, the equipment ensures that the material is transported without degradation, maintaining its purity and effectiveness for downstream processes.
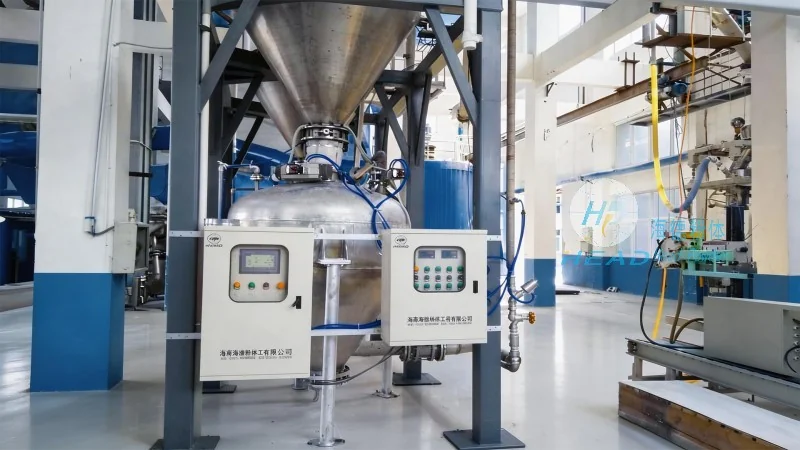
The magnesium sulfate heptahydrate powder conveying equipment typically consists of several key components, each playing a vital role in the overall operation. These components include a hopper for material storage, a conveyor mechanism (such as a screw conveyor or pneumatic system) for transporting the powder, and a control system to regulate the flow and speed of the material. The design principles behind this equipment are centered on efficiency, reliability, and safety. For instance, the system is designed to minimize material loss and prevent contamination, which is critical for pharmaceutical or food-grade applications where magnesium sulfate heptahydrate is used.
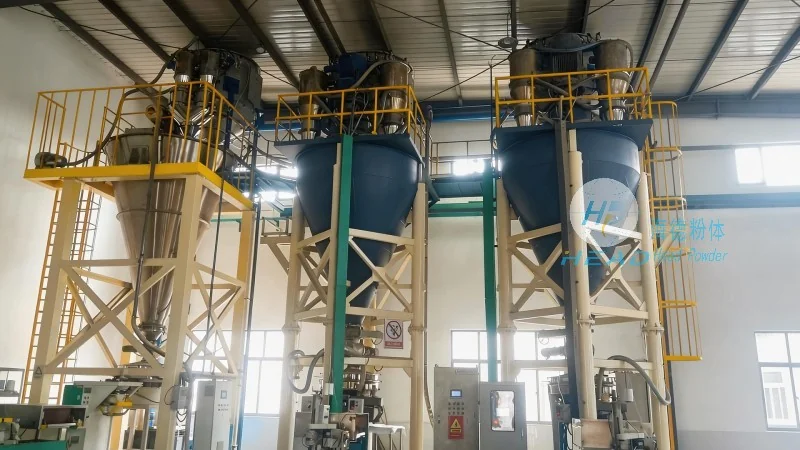
The operation of the magnesium sulfate heptahydrate powder conveying equipment begins with the material being fed into the hopper. The hopper is designed with a sloped bottom to facilitate the flow of the powder into the conveyor mechanism. Depending on the specific design, the conveyor may use mechanical force (like a screw or auger) or pneumatic pressure to move the material through the system. The control system monitors the flow rate and adjusts the speed of the conveyor as needed to maintain a consistent and controlled delivery of the material. This ensures that the downstream processes receive a steady supply of magnesium sulfate heptahydrate without interruptions or variations in quality.
Implementing this specialized conveying equipment offers several advantages for industrial operations. First, it enhances the efficiency of material handling by reducing the time and labor required to transport magnesium sulfate heptahydrate. The automated system minimizes human error and ensures consistent performance, leading to improved productivity. Second, the equipment helps maintain the quality of the material by preventing exposure to moisture and air, which can cause degradation or clumping. This is particularly important for applications where the purity of magnesium sulfate heptahydrate is critical, such as in pharmaceutical manufacturing or food processing. Third, the system is designed for safety, with features like dust suppression and enclosed conveyor systems to minimize the risk of dust explosions or inhalation hazards associated with handling fine powders.
The magnesium sulfate heptahydrate powder conveying equipment is widely used in various industries that rely on this chemical compound. In the pharmaceutical industry, it is used to transport magnesium sulfate heptahydrate for the production of medications, where consistent quality and purity are paramount. In the food industry, it is used in the manufacturing of baking powders and other food additives, where the material must meet strict regulatory standards. Additionally, the equipment is utilized in the chemical and agricultural sectors for the production of fertilizers and other magnesium-based products. By providing a reliable and efficient method of powder transport, this equipment supports the smooth operation of these industries and ensures that the final products meet the required specifications.
Shandong HeadPowder Engineering Co., Ltd. offers customization options for the magnesium sulfate heptahydrate powder conveying equipment to meet the specific needs of different clients. The company can adapt the system to work with existing production lines or integrate it with other processing equipment, such as mixers or granulators. This flexibility allows clients to optimize their operations and achieve better results. For example, the conveyor speed and capacity can be adjusted based on the production volume, and the system can be equipped with additional features like dust collection or material analysis to enhance its functionality. The company's expertise in powder handling technology ensures that the customized equipment is designed to operate efficiently and safely, providing long-term value to the client.

To ensure the longevity and performance of the magnesium sulfate heptahydrate powder conveying equipment, regular maintenance is essential. The system should be inspected regularly for wear and tear on components such as the conveyor screws or seals, which can affect the efficiency of the operation. Cleaning the equipment after each use is also important to prevent the buildup of material and maintain hygiene, especially in industries like pharmaceuticals or food processing. Additionally, the control system should be checked to ensure that it is functioning correctly and that the flow rates are being monitored accurately. By following proper maintenance procedures, clients can extend the lifespan of the equipment and minimize downtime, which is crucial for maintaining production schedules and meeting customer demands.
In conclusion, the magnesium sulfate heptahydrate powder conveying equipment is a critical component for industrial operations that handle this specific chemical compound. Developed by Shandong HeadPowder Engineering Co., Ltd., the system is designed to ensure efficient, safe, and reliable transport of magnesium sulfate heptahydrate. By incorporating advanced design principles and components, the equipment helps maintain the quality and integrity of the material, supporting the success of various industries. As a leading manufacturer based in China, Shandong HeadPowder Engineering Co., Ltd. continues to provide high-quality solutions for powder handling, helping clients achieve their production goals while adhering to safety and regulatory standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top