With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Calcium phosphate is a critical raw material in various industrial applications, including pharmaceuticals, food processing, and chemical manufacturing. Efficient and reliable material handling is essential to ensure consistent quality and productivity in production lines. This article explores the calcium phosphate material handling system, detailing its design principles and operational aspects.
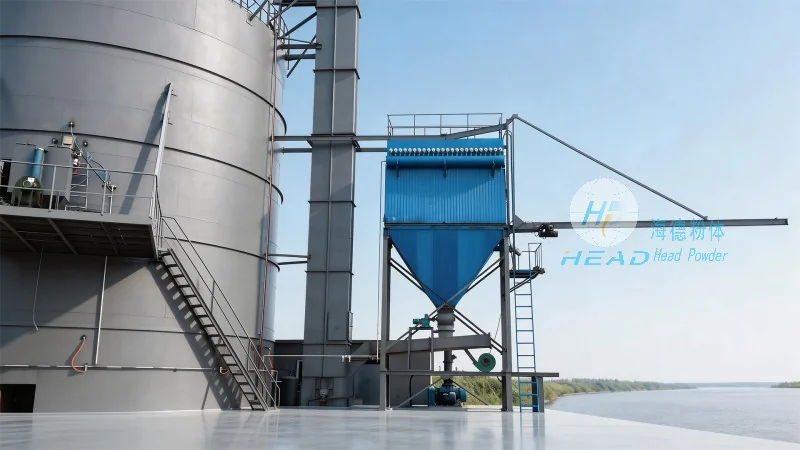
The calcium phosphate material handling system is engineered to manage the flow of calcium phosphate powders and granules from storage to processing units. The design incorporates several key components that work in tandem to optimize material movement. These include bulk material feeders, conveyor systems, and control mechanisms. The system's design principles prioritize material integrity, minimizing dust generation and ensuring uniform flow rates. For instance, the use of enclosed conveyor belts and dust collection systems is standard to maintain product purity and operator safety. The control system integrates sensors and automation to adjust feed rates based on real-time demand, enhancing operational flexibility.
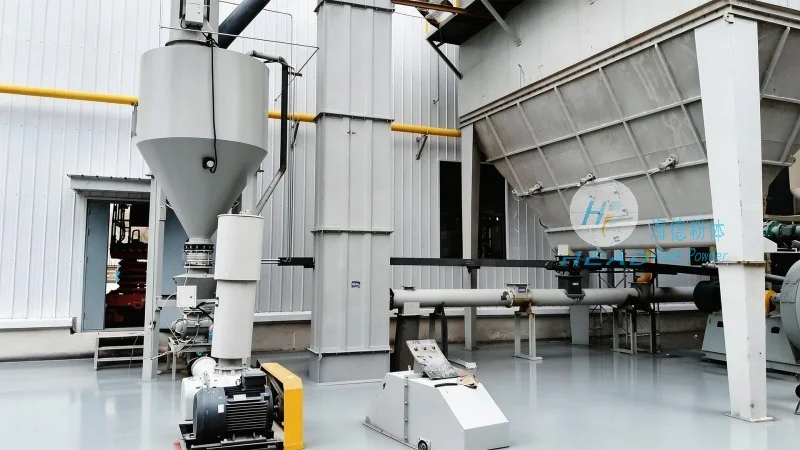
Operational efficiency is a core focus of the system's design. By automating material transfer, the system reduces manual handling, which in turn lowers labor costs and minimizes human error. The conveyor systems are equipped with variable speed drives, allowing precise control over material flow. This adaptability is crucial in dynamic production environments where demand fluctuates. Safety features are also integral, with emergency stop buttons, overload protection, and dust suppression measures built into the design. These elements ensure a secure working environment for personnel and protect the material from contamination. The system's modular design facilitates easy maintenance and component replacement, reducing downtime and extending the equipment's lifespan.
The calcium phosphate material handling system is widely used in industries that rely on calcium phosphate as a key ingredient. In the pharmaceutical sector, it supports the production of calcium supplements and other formulations where material purity is paramount. In food processing, the system ensures consistent mixing and distribution of calcium phosphate in products like dairy and baked goods. The chemical industry also benefits from the system's ability to handle calcium phosphate in bulk, supporting processes such as fertilizer production and industrial chemicals. The versatility of the system makes it suitable for various production scales, from small-scale laboratory applications to large-scale industrial operations.
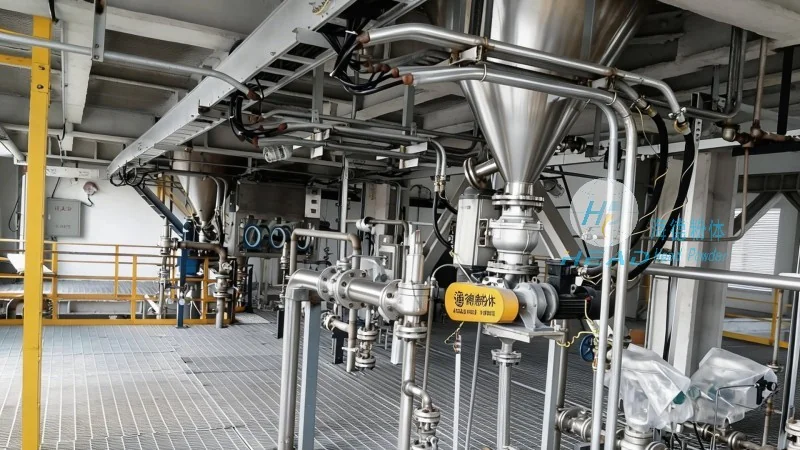
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer specializing in material handling solutions for the chemical and pharmaceutical industries. With a focus on innovation and quality, the company has developed advanced systems tailored to the unique needs of calcium phosphate processing. HeadPowder's expertise lies in designing equipment that balances efficiency, safety, and cost-effectiveness. The company's facilities are located in Shandong, China, where it leverages local resources and expertise to deliver high-performance material handling systems. By adhering to international standards and customer-specific requirements, HeadPowder ensures that its products meet the rigorous demands of modern industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top