With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Bulk material handling systems are essential in various industrial applications, particularly in sectors that deal with the storage and transportation of powders and granules. These systems, often referred to as bulk handling equipment, are designed to efficiently manage the flow of materials from storage silos or hoppers to processing units or packaging areas. The core components of such systems typically include hoppers, conveyors, and control mechanisms, all working in tandem to ensure smooth and reliable material movement.
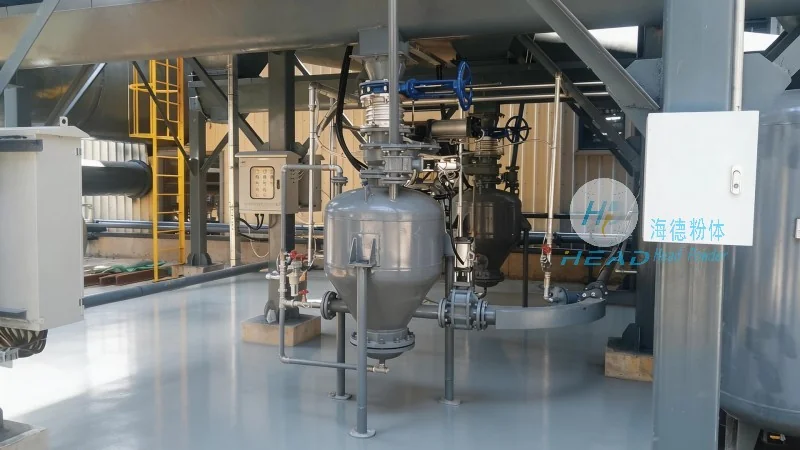
The functionality of a bulk material handling system is largely determined by its key components. The hopper, or storage silo, is the primary container where raw materials are stored. It is engineered to maintain material stability and prevent caking or segregation. The conveyor system, which may include screw conveyors, pneumatic conveyors, or belt conveyors, is responsible for transporting the material from the hopper to the next stage of processing. Control mechanisms, such as sensors and valves, regulate the flow rate and ensure that the system operates safely and efficiently. These components are carefully integrated to create a cohesive system that meets the specific needs of the industrial process.
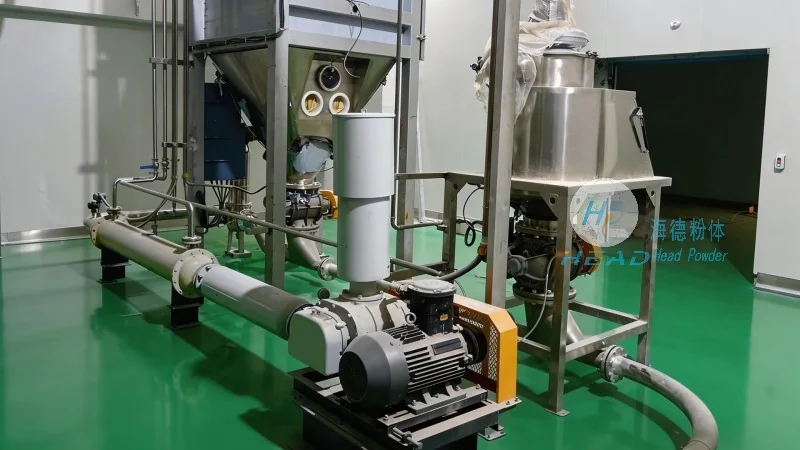
The design of a bulk material handling system is guided by several critical principles aimed at optimizing performance and reliability. One of the primary principles is the minimization of material degradation, which can occur due to friction, impact, or exposure to air. To achieve this, the system is designed with smooth surfaces and gentle material movement, reducing the risk of particle breakage. Another key principle is the prevention of material bridging and arching, which can block the flow of material. This is addressed through the use of hopper designs with appropriate angles and the incorporation of vibrators or air knives to break down any potential blockages. Additionally, the system is engineered for easy maintenance and cleaning, ensuring that it can be kept in optimal working condition with minimal downtime.
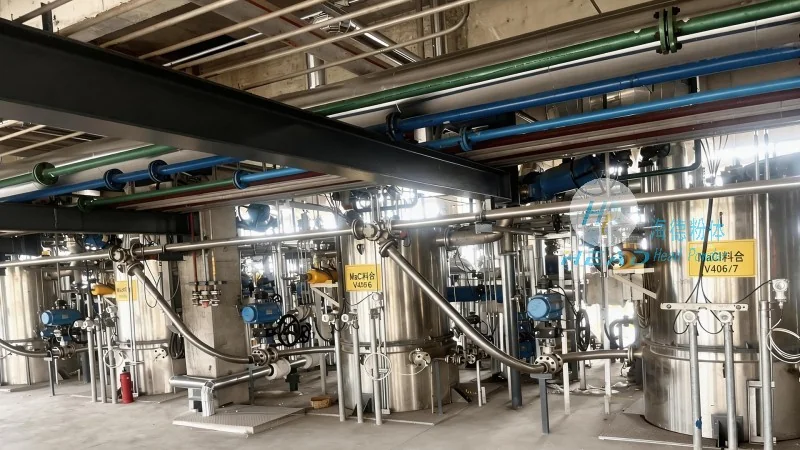
Bulk material handling systems are widely used across multiple industries, including food processing, pharmaceuticals, chemicals, and mining. In the food industry, for example, these systems are crucial for handling ingredients like flour, sugar, and spices, ensuring that they are transported safely and hygienically. In the pharmaceutical sector, the systems are designed to maintain strict contamination control, as even small amounts of impurities can affect product quality. The chemical industry relies on bulk handling systems to manage raw materials like powders and granules, which are often hazardous and require careful handling. Similarly, in the mining industry, these systems are used to transport ore and other bulk materials from storage to processing plants. The versatility of bulk material handling systems makes them indispensable in these and other sectors, where efficient material flow is critical to operational success.

Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of bulk material handling systems. With a strong presence in China, particularly in Shandong, the company specializes in designing and manufacturing equipment tailored to the specific needs of various industries. HeadPowder's commitment to quality and innovation has made it a trusted partner for businesses seeking reliable and efficient bulk handling solutions. The company's products are engineered to meet international standards and are backed by a team of experienced engineers and technicians who provide comprehensive support throughout the product lifecycle.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top