With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
When it comes to efficient material handling in industrial settings, the tonne bag discharge pneumatic conveying machine stands out as a crucial piece of equipment. This system is designed to handle bulk materials from tonne bags, facilitating their transfer with precision and reliability. The core function of this machine is to automate the process of unloading and conveying materials, which is essential for maintaining smooth operations in various industries such as food processing, pharmaceuticals, and chemical manufacturing.
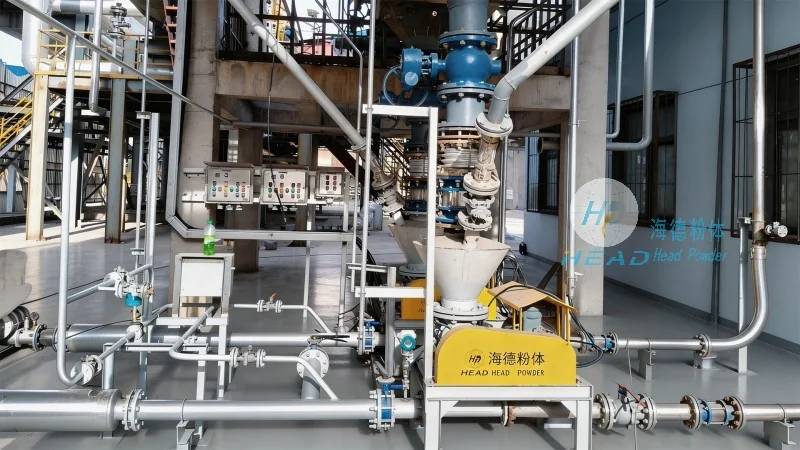
At Shandong HeadPowder Engineering Co., Ltd., we specialize in developing and manufacturing advanced material handling equipment. With our headquarters located in Shandong, China, we leverage years of industry experience to deliver high-quality solutions tailored to the needs of our clients. Our team of engineers and technicians is dedicated to ensuring that every product we produce meets the highest standards of performance and durability. By choosing HeadPowder, you are selecting a partner committed to excellence in material handling technology.
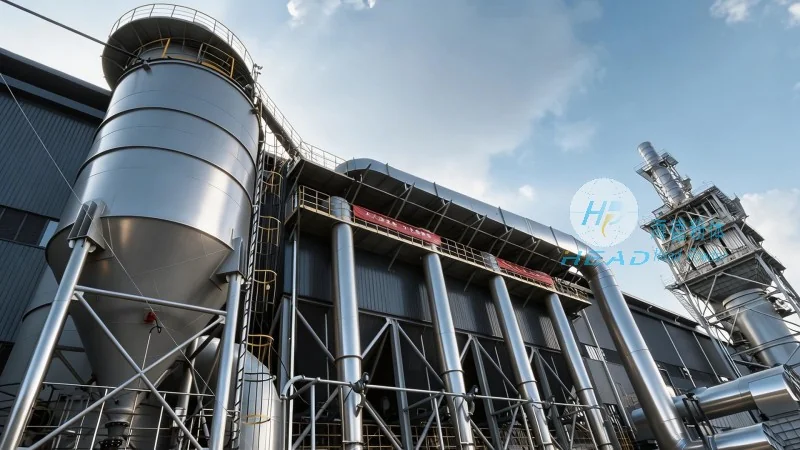
The design of a tonne bag discharge pneumatic conveying machine is built on the fundamental principles of pneumatic conveying technology. At its core, the system operates by using compressed air to create a flow that moves material from the tonne bag to the processing area. The key components include a discharge valve, a hopper, and a conveying line, all working in harmony to ensure efficient material transfer. The discharge valve is specifically engineered to open and release the material from the tonne bag under controlled conditions, preventing spillage and maintaining a clean operation. The hopper then collects the material and feeds it into the conveying line, where the compressed air propels the material through the system. This design minimizes the need for manual intervention, reducing labor costs and enhancing safety in the workplace.
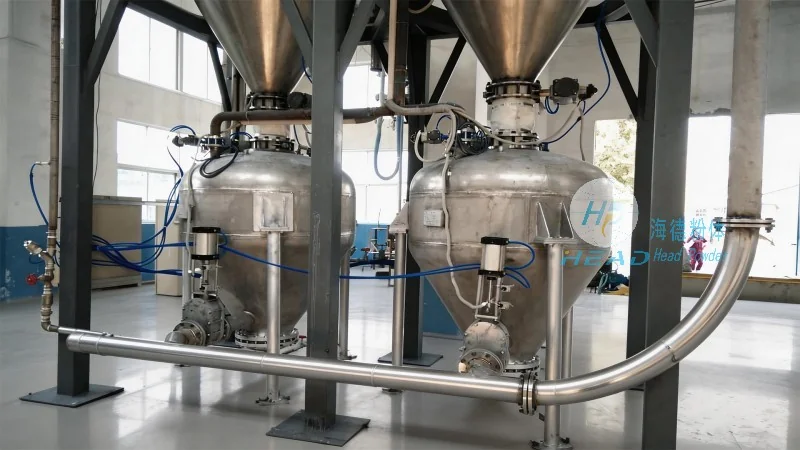
One of the primary advantages of the tonne bag discharge pneumatic conveying machine is its ability to handle a wide range of materials, from fine powders to bulk solids. The system is designed to be flexible, allowing for adjustments to accommodate different material properties and flow rates. Another key feature is its hygienic design, which is particularly important in industries such as food and pharmaceuticals where cleanliness is paramount. The machine's components are constructed from materials that are easy to clean and maintain, ensuring compliance with regulatory standards. Additionally, the system is energy-efficient, as it uses compressed air only when necessary, reducing operational costs over time. The compact design of the machine also makes it suitable for installations with limited space, making it a versatile solution for various industrial applications.
Understanding how the tonne bag discharge pneumatic conveying machine operates can help users maximize its benefits. The process begins with the tonne bag being placed in the discharge area. The discharge valve is then activated, allowing the material to flow into the hopper. Simultaneously, compressed air is introduced into the conveying line, creating a pressure differential that draws the material from the hopper into the line. The material is then transported to the desired destination, such as a silo or processing unit. The system is equipped with sensors and controls that monitor the flow rate and pressure, ensuring that the operation runs smoothly and safely. In case of any issues, such as blockages or low pressure, the system automatically shuts down to prevent damage and maintain the integrity of the material.
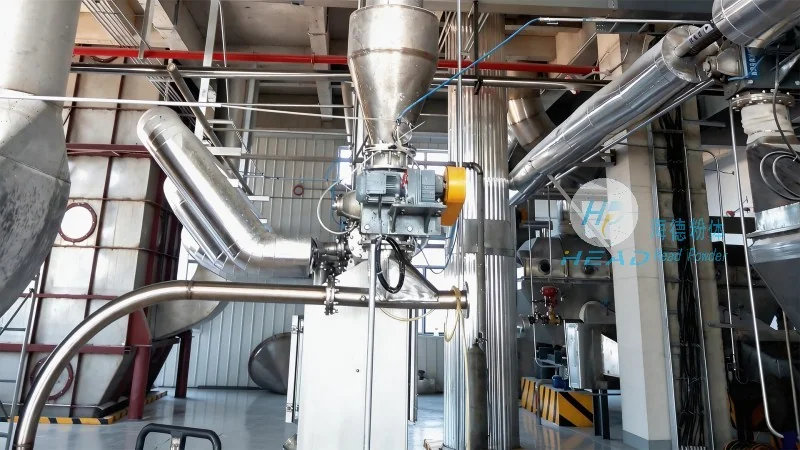
The tonne bag discharge pneumatic conveying machine is widely used across various industries due to its versatility and efficiency. In the food industry, it is used to handle ingredients like flour, sugar, and spices, ensuring that the material is transferred without contamination. In the pharmaceutical sector, the system is employed to transport raw materials and finished products, maintaining the high standards of cleanliness and safety required by regulatory bodies. The chemical industry also benefits from this technology, as it allows for the safe handling of hazardous materials, reducing the risk of accidents and exposure. Additionally, the machine is used in the agricultural sector to handle bulk commodities like grains and seeds, facilitating their storage and distribution. Overall, the system's ability to handle different materials and its adaptability make it a valuable asset in many industrial settings.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top