HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for fine sand and gravel applications. The company's expertise lies in delivering efficient and reliable solutions that meet the demanding requirements of various industrial sectors.
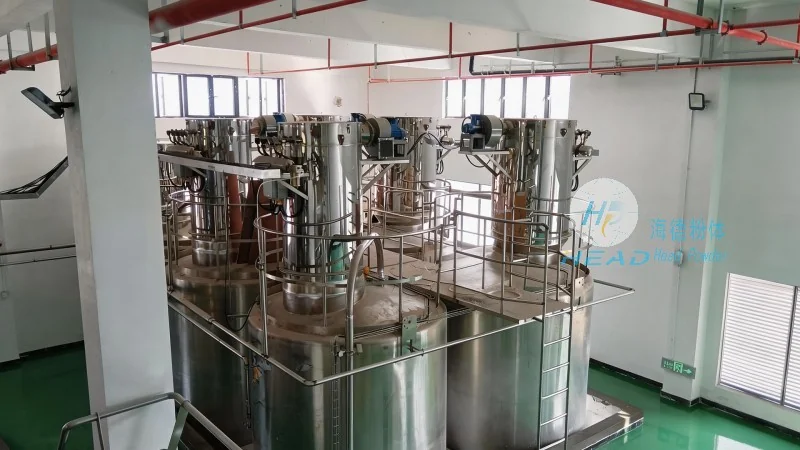
Overview of Fine Sand and Gravel Pneumatic Conveying Equipment
Fine sand and gravel pneumatic conveying equipment is a critical component in material handling processes, enabling the transport of granular materials like fine sand, gravel, and similar particulates through an air-driven system. This technology offers a flexible and efficient alternative to traditional mechanical conveying methods, such as belt conveyors or screw conveyors, by utilizing compressed air to move materials through a pipeline network.
The Working Principle of Pneumatic Conveying Systems
The core principle of pneumatic conveying for fine sand and gravel involves the creation of a low-pressure or high-pressure air stream within a sealed pipeline. The material to be conveyed is introduced into the system, typically at the inlet or by a feeder device, and is then entrained by the moving air. As the air flows through the pipeline, it carries the fine particles along, ensuring a continuous and controlled transport from the source to the destination. The system may operate under positive pressure (where air pushes the material) or negative pressure (where air pulls the material), depending on the specific application and system design.
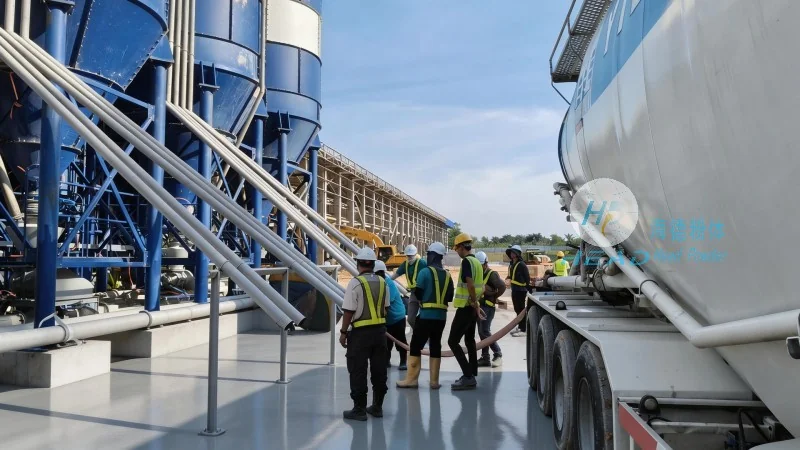
Key Components and Their Functions
Several key components work in tandem to ensure the smooth operation of fine sand and gravel pneumatic conveying equipment. These include:
- Feeder Unit: This component is responsible for introducing the fine sand or gravel into the conveying system. It ensures a consistent and controlled feed rate, preventing blockages and maintaining system efficiency.
- Conveying Pipeline: The pipeline serves as the main pathway for transporting the material and air. It is typically made of durable materials like stainless steel or PVC to withstand the abrasive nature of fine sand and gravel, ensuring long-term reliability.
- Compressor or Blower: This is the power source that generates the necessary air pressure to move the material through the pipeline. The choice between a compressor (for high-pressure systems) and a blower (for low-pressure systems) depends on the specific conveying requirements, such as distance, material characteristics, and system capacity.
- Control Valves and Regulators: These components are used to regulate the air pressure and flow rate within the system. They help maintain optimal conditions for material transport, preventing over-pressurization or under-pressurization that could lead to system inefficiencies or material degradation.
- Receiver or Discharge Unit: The receiver is where the conveyed material is collected after it is deposited from the air stream. It is designed to separate the material from the air and store it in a container or hopper, ensuring a clean and efficient discharge process.
Advantages of Fine Sand and Gravel Pneumatic Conveying Equipment
Compared to traditional mechanical conveying methods, fine sand and gravel pneumatic conveying equipment offers several distinct advantages:
- Flexibility and Versatility: The system can be easily reconfigured or expanded to accommodate changes in material flow rates or process requirements. It can handle various types of fine particulates, including sand, gravel, and other granular materials, making it suitable for diverse industrial applications.
- Reduced Maintenance and Downtime: Pneumatic conveying systems have fewer moving parts compared to mechanical conveyors, resulting in lower maintenance requirements and reduced downtime. This translates to lower operational costs and increased productivity.
- Improved Material Handling Efficiency: The air-driven system allows for a continuous and controlled transport of materials, minimizing the risk of material degradation or segregation. It can handle materials with high moisture content or abrasive properties without causing damage to the equipment.
- Space Efficiency: Pneumatic conveying systems can be installed in tight spaces or vertical configurations, making them ideal for facilities with limited floor space or where vertical transport is required.
Applications in Industrial Sectors
Fine sand and gravel pneumatic conveying equipment is widely used across various industrial sectors, including:
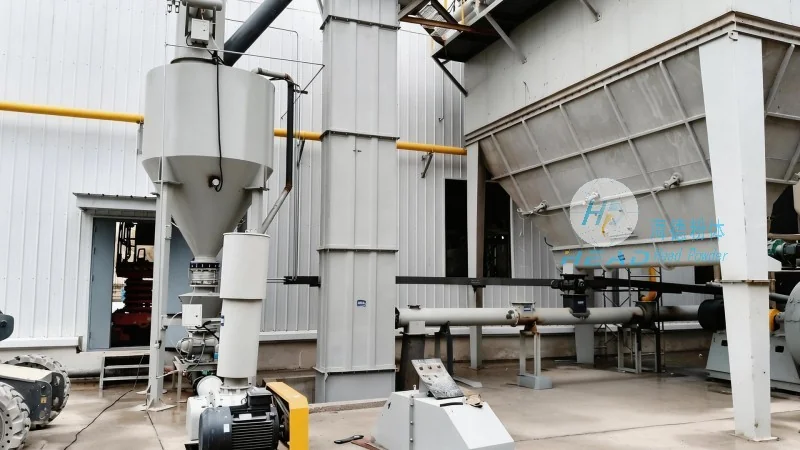
- Construction and Mining: In construction projects, the equipment is used to transport sand, gravel, and other aggregates from storage sites to construction sites. In mining operations, it helps in the transport of crushed ore and fine particles from processing plants to storage or further processing units.
- Food and Pharmaceutical Industries: Although less common for fine sand and gravel, pneumatic conveying systems are used in these sectors for handling dry powders and granules, such as flour, sugar, or pharmaceutical powders, where dust control and hygiene are critical.
- Chemical and Petrochemical Industries: The equipment is employed to transport fine powders and granules, such as chemicals, catalysts, and raw materials, in chemical processing plants. It ensures a safe and efficient transport of materials, minimizing the risk of contamination and material loss.
- Environmental and Waste Management: Pneumatic conveying systems are used in waste management facilities to transport fine waste materials, such as sludge or ash, from processing units to disposal or treatment sites. This helps in maintaining a clean and efficient waste handling process.
Customization and Integration with Existing Systems
HeadPowder understands that each industrial application has unique requirements. Therefore, the company offers customized pneumatic conveying solutions tailored to the specific needs of clients. The equipment can be integrated with existing systems, such as storage silos, processing units, or packaging lines, ensuring seamless operation and optimal performance.
By leveraging advanced engineering and manufacturing capabilities, HeadPowder ensures that its fine sand and gravel pneumatic conveying equipment meets the highest standards of quality, efficiency, and reliability. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking effective material handling solutions in the fine sand and gravel industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China
