With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Pneumatic conveying technology has emerged as a critical solution for efficient and reliable transport of bulk materials, particularly in the fertilizer industry. For potassium carbonate fertilizer, which is a vital component in modern agricultural practices, the design and implementation of effective transport systems are paramount to ensuring product integrity and operational efficiency. This article explores the application and optimization of pneumatic conveying technology in the context of potassium carbonate fertilizer transport, highlighting key considerations and best practices for successful implementation.
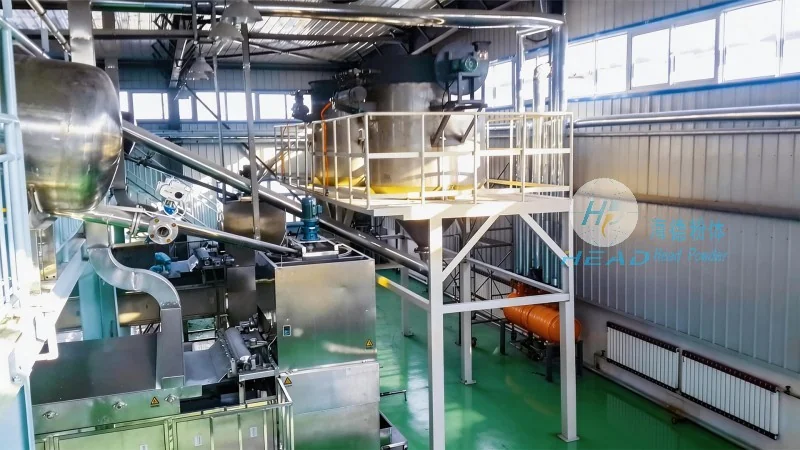
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of engineering solutions tailored to the needs of the fertilizer and bulk material handling sectors. With a strong focus on innovation and customer-centric design, HeadPowder specializes in developing customized pneumatic conveying systems that address the unique challenges of transporting potassium carbonate fertilizer. The company's team of experienced engineers leverages advanced technology and industry knowledge to deliver solutions that enhance productivity, reduce operational costs, and ensure compliance with safety and environmental standards.
The successful application of pneumatic conveying in potassium carbonate fertilizer transport relies on several key features that optimize performance and reliability. First, the system's design must accommodate the physical properties of potassium carbonate, such as its particle size, density, and flow characteristics. HeadPowder's engineers conduct thorough material analysis to determine the most suitable conveying method—whether it be dilute-phase or dense-phase pneumatic conveying—based on the specific requirements of the application. This ensures that the material is transported with minimal degradation and maximum efficiency.
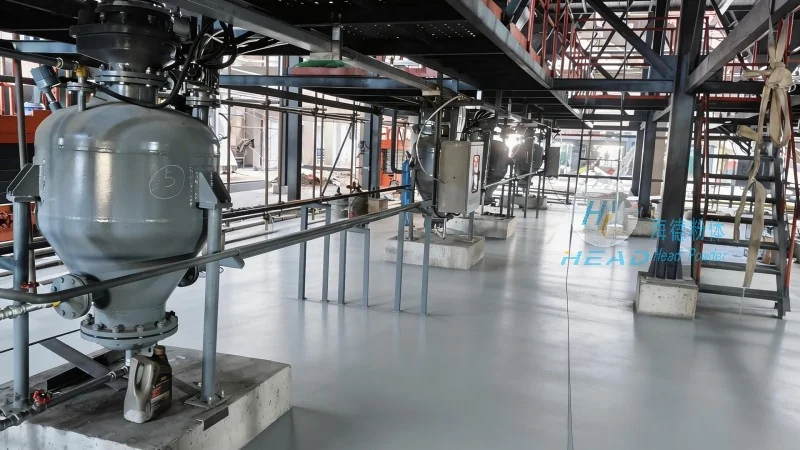
Second, the system must incorporate robust components that can withstand the corrosive nature of potassium carbonate and the abrasive conditions of bulk material handling. HeadPowder utilizes high-quality materials, including stainless steel and specialized coatings, to protect against wear and corrosion, thereby extending the lifespan of the equipment and reducing maintenance costs. Additionally, the system's control mechanisms are designed to provide precise regulation of air flow, pressure, and material feed rates, ensuring consistent and reliable operation.
To maximize the efficiency of pneumatic conveying systems for potassium carbonate fertilizer, several optimization strategies are employed. One key approach is the integration of advanced control systems that use real-time data to adjust operational parameters dynamically. This allows for optimal performance under varying load conditions, reducing energy consumption and improving overall system efficiency. HeadPowder's systems often incorporate sensors and monitoring tools that provide continuous feedback on key performance indicators, enabling proactive maintenance and troubleshooting.
Another critical optimization strategy is the design of the conveying line layout to minimize pressure drops and energy losses. By carefully planning the length, elevation changes, and number of bends in the system, engineers can reduce the energy required to move the material, leading to significant cost savings over time. HeadPowder's expertise in system design includes detailed hydraulic and pneumatic calculations to ensure that the system operates within optimal parameters, avoiding unnecessary energy expenditure.
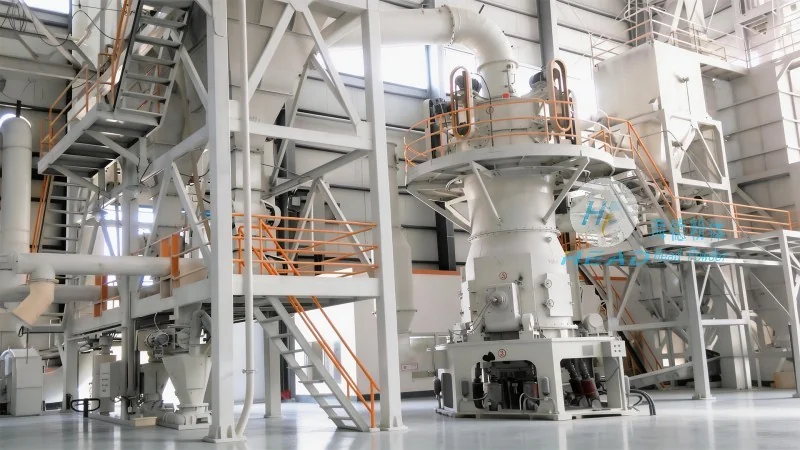
The adoption of pneumatic conveying technology for potassium carbonate fertilizer transport offers numerous benefits that enhance both operational performance and product quality. Firstly, the system provides a closed-loop transport process, which minimizes dust emissions and environmental impact, aligning with modern sustainability goals. This is particularly important for potassium carbonate, which can be a source of particulate matter if not handled properly. HeadPowder's systems are designed with dust control features, such as filtration and containment, to ensure compliance with environmental regulations and maintain a safe working environment.
Secondly, pneumatic conveying enables faster and more reliable material transport compared to traditional methods like belt conveyors or trucks. The ability to transport material over long distances without the need for intermediate storage or handling points reduces processing time and improves overall supply chain efficiency. This is especially valuable for fertilizer manufacturers who need to meet tight delivery schedules and maintain consistent product availability.
Thirdly, the system's flexibility allows for easy integration with existing production and storage facilities. HeadPowder's engineers work closely with clients to assess their current infrastructure and design a system that seamlessly integrates with their operations, minimizing disruption and maximizing return on investment. The modular nature of pneumatic conveying systems also facilitates future expansion or modifications as business needs evolve.
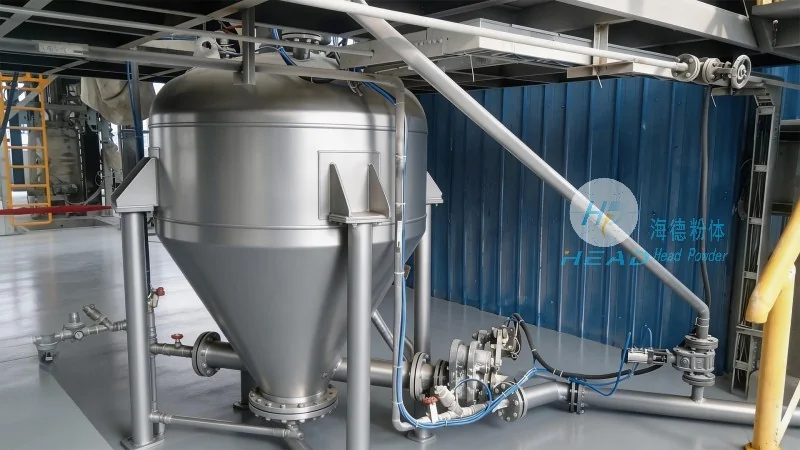
A recent project by HeadPowder involved the design and installation of a pneumatic conveying system for a potassium carbonate fertilizer plant in Shandong, China. The client required a solution to transport bulk material from storage silos to processing units over a distance of 500 meters, while maintaining product integrity and minimizing downtime. HeadPowder's team conducted a comprehensive analysis of the material properties and operational requirements, then designed a dilute-phase pneumatic conveying system with a stainless steel pipeline and advanced control panels. The system was installed and commissioned within a short timeframe, achieving the client's target of 95% material transfer efficiency and reducing energy consumption by 20% compared to traditional methods. The client reported significant improvements in operational efficiency and product quality, validating the effectiveness of HeadPowder's pneumatic conveying solution.
The application and optimization of pneumatic conveying technology in potassium carbonate fertilizer transport represent a significant advancement in bulk material handling. By leveraging advanced engineering, robust system design, and continuous optimization, companies like HeadPowder are enabling fertilizer manufacturers to enhance productivity, reduce costs, and improve product quality. As the demand for efficient and sustainable transport solutions continues to grow, pneumatic conveying will remain a key technology in the fertilizer industry. HeadPowder's commitment to innovation and customer satisfaction positions it as a trusted partner for businesses seeking to optimize their potassium carbonate fertilizer transport processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top