With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Wood ash, a byproduct of biomass combustion, presents unique challenges in handling and transportation due to its fine particle size, moisture content, and abrasive nature. Traditional methods like belt conveyors or bucket elevators often struggle with material buildup, blockages, and maintenance issues when dealing with such materials. Pneumatic conveying technology, which uses air to transport bulk materials through pipelines, has emerged as a highly effective solution for these challenges, offering advantages such as low maintenance, flexible system design, and the ability to handle dusty or corrosive materials. This article explores the application and optimization of pneumatic conveying systems specifically tailored for wood ash transport, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. (hereinafter referred to as HeadPowder) in designing efficient and reliable solutions for this industry.
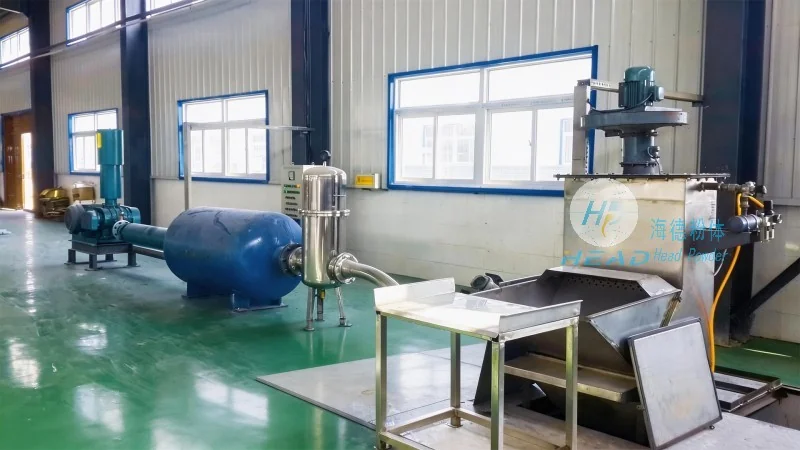
Wood ash, generated from the combustion of wood or other biomass sources, is characterized by its fine, powdery structure and high moisture absorption capacity. These properties make it prone to caking, agglomeration, and blockage in conventional conveying equipment. Additionally, the abrasive nature of ash particles can lead to accelerated wear on conveyor components, increasing maintenance costs and downtime. Traditional mechanical conveyors may also struggle with the dust generation during transport, posing health and safety risks to workers and requiring additional dust control measures. The need for a system that can handle these characteristics efficiently and reliably has driven the adoption of pneumatic conveying technology in the wood ash handling industry.
Pneumatic conveying systems operate by transporting bulk materials through a network of pipelines using compressed air or vacuum. There are two primary types: pressure and vacuum systems. Pressure systems use positive pressure to push material through the pipeline, while vacuum systems use negative pressure to draw material into the system. For wood ash, pressure systems are often preferred due to their ability to handle higher material loads and longer distances without significant pressure loss. Key advantages of pneumatic conveying for wood ash include: (1) Reduced risk of material degradation or contamination as the material remains enclosed within the pipeline; (2) Lower energy consumption compared to mechanical conveyors, especially over long distances; (3) Flexibility in system layout, allowing for multiple discharge points and integration with other processing equipment; (4) Minimal space requirements, as the system can be installed in existing facilities without extensive structural modifications. These benefits make pneumatic conveying an attractive option for wood ash transport, particularly in applications where material handling efficiency and system reliability are critical.
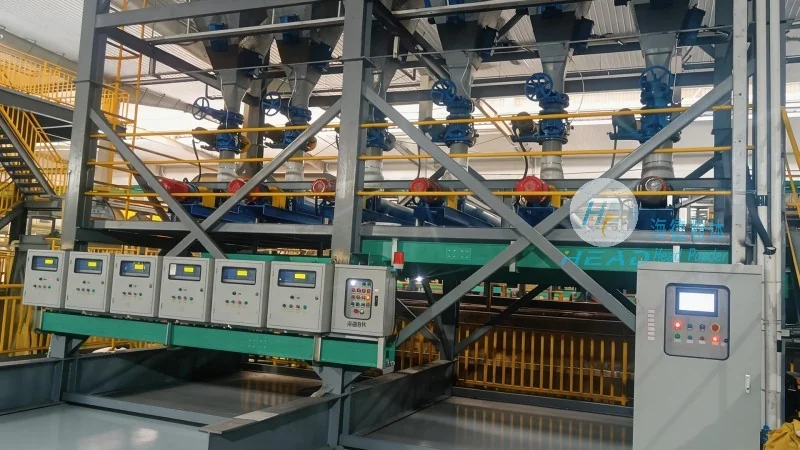
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and implementing pneumatic conveying systems tailored to the unique requirements of wood ash transport. The company's approach involves a comprehensive analysis of the client's operational needs, including the volume of ash to be handled, the distance of transport, the desired discharge points, and any environmental or safety constraints. HeadPowder's engineers work closely with clients to develop customized system designs that optimize performance while minimizing costs. A key aspect of their optimization strategy is the selection of appropriate equipment components, such as high-efficiency air blowers, durable pipeline materials (e.g., stainless steel or corrosion-resistant alloys), and specialized ash handling valves. The company also emphasizes the importance of system integration, ensuring that the conveying system works seamlessly with other processing equipment, such as storage silos, grinding mills, or pelletizing units. By focusing on these critical components and system integration, HeadPowder ensures that their pneumatic conveying solutions for wood ash are not only efficient but also durable and low-maintenance.
The success of a wood ash pneumatic conveying system depends on the careful selection and integration of several key components. The air compressor or blower is the heart of the system, responsible for generating the necessary pressure or vacuum to move the material. For wood ash, high-capacity, low-noise blowers are typically used to ensure consistent material flow without excessive energy consumption. The pipeline system is another critical component, as it must be constructed from materials that can withstand the abrasive nature of ash particles and potential moisture exposure. Stainless steel or coated steel pipelines are commonly used, with smooth internal surfaces to minimize friction and reduce the risk of material buildup. Ash handling valves, such as rotary airlock valves or slide gates, are used to control the flow of material at discharge points, preventing backflow and ensuring consistent discharge rates. These valves are designed with wear-resistant materials to extend their service life in abrasive environments. Additionally, dust collection and filtration systems are essential to maintain air quality and comply with environmental regulations. HeadPowder incorporates advanced filtration technologies, such as baghouse filters or cartridge filters, to capture fine ash particles and return clean air to the environment.
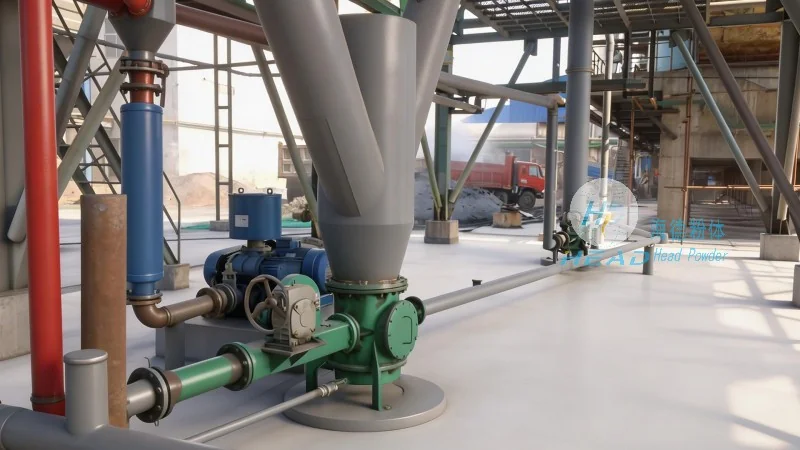
To illustrate the effectiveness of HeadPowder's optimization approach, consider a case study of a biomass power plant in China that was experiencing frequent blockages and high maintenance costs with its existing mechanical conveyor system. The plant needed to transport wood ash from the boiler to a storage silo over a distance of 200 meters, with multiple discharge points along the way. HeadPowder conducted a thorough analysis of the plant's operational data and conducted on-site inspections to identify the root causes of the problems. The existing system was found to have insufficient air pressure, leading to inadequate material transport, and worn-out pipeline components causing friction and buildup. HeadPowder designed a new pneumatic conveying system using high-efficiency pressure blowers and stainless steel pipelines with smooth internal surfaces. The system was equipped with rotary airlock valves at each discharge point to control the flow and prevent backflow. After implementation, the plant reported a significant reduction in blockages and maintenance downtime, with the new system achieving consistent material flow rates and lower energy consumption. The plant also noted improved safety due to the enclosed pipeline system, which reduced dust exposure for workers. This case study highlights how HeadPowder's optimization of pneumatic conveying technology can address the specific challenges of wood ash transport and deliver measurable benefits to clients.
Pneumatic conveying technology has proven to be a highly effective solution for the challenges associated with wood ash transport, offering advantages in efficiency, reliability, and safety. Shandong HeadPowder Engineering Co., Ltd. plays a crucial role in this field by providing customized, optimized systems that meet the unique needs of wood ash handling operations. By focusing on key components such as air blowers, pipeline materials, and ash handling valves, and by emphasizing system integration and maintenance, HeadPowder ensures that their pneumatic conveying solutions are durable, low-maintenance, and cost-effective. As the biomass industry continues to grow, the demand for efficient wood ash handling systems will remain high, and pneumatic conveying technology will continue to be a key component in meeting these needs. HeadPowder's expertise in designing and implementing these systems positions them as a trusted partner for companies seeking to optimize their wood ash transport processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top