With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the application and optimization of pneumatic conveying technology for mineral sand transport systems. This article explores the key aspects of integrating advanced pneumatic conveying solutions into mineral sand handling operations, highlighting the benefits and practical considerations for efficient material transport.
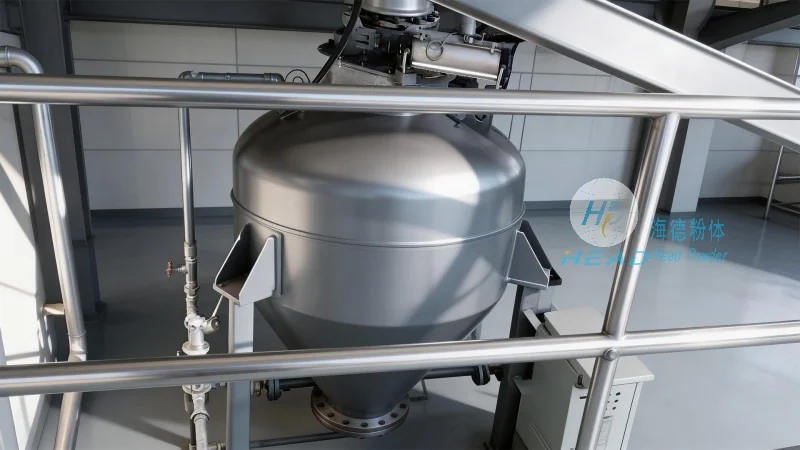
Pneumatic conveying systems utilize air or gas to transport bulk materials like mineral sands through pipelines. This technology offers a flexible and efficient alternative to traditional methods such as belt conveyors or bucket elevators. The core principle involves creating a pressure differential to move the material, which can be either positive pressure (where air pushes the material) or negative pressure (where air pulls the material). For mineral sand applications, the choice of system depends on factors like material characteristics, distance, and throughput requirements.
HeadPowder's expertise lies in designing customized pneumatic conveying solutions tailored to the unique demands of mineral sand processing. These systems are widely used in various stages of mineral sand handling, including:
1. Raw Material Transport: Moving raw mineral sands from storage silos or mining sites to processing facilities. Pneumatic conveyors can handle large volumes with minimal space requirements, making them ideal for industrial settings.
2. In-Plant Material Transfer: Transferring processed mineral sands between different processing units, such as from crushing and screening to drying or packaging. The flexibility of pneumatic systems allows for seamless integration into existing plant layouts.
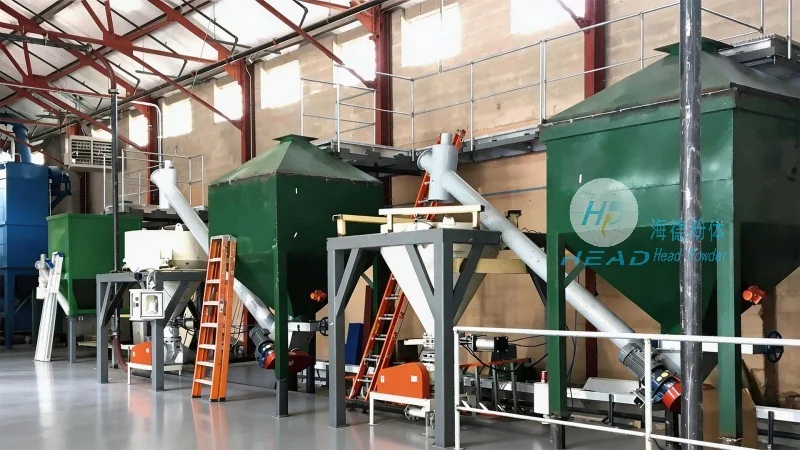
3. Product Distribution: Delivering finished mineral sand products to storage tanks or shipping containers. This stage requires precise control to ensure consistent product quality and minimize dust generation.
Optimizing pneumatic conveying systems for mineral sands involves several critical factors to ensure maximum efficiency and reliability. HeadPowder employs advanced engineering techniques to address these aspects:
1. Material Characterization: Thorough analysis of the mineral sand's properties, including particle size distribution, moisture content, and abrasiveness. This data is crucial for selecting the appropriate air velocity, pipeline diameter, and equipment materials to prevent blockages and wear.
2. System Sizing and Layout: Proper sizing of the conveying pipeline, air compressor, and associated components based on the required throughput and distance. The layout must consider the plant's spatial constraints and operational flow to minimize energy consumption and maintenance costs.
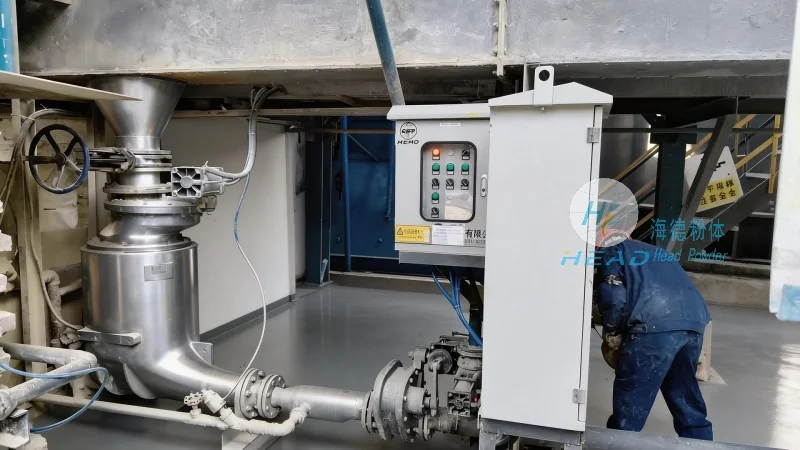
3. Control System Integration: Implementing advanced control systems to monitor and adjust the conveying process in real-time. These systems can regulate air pressure, flow rates, and material feed to maintain optimal performance and prevent system failures.
Adopting optimized pneumatic conveying technology for mineral sand transport offers numerous advantages for industrial operations:
1. Increased Efficiency: Pneumatic systems can transport large volumes of material at high speeds, reducing overall processing time and improving production throughput.
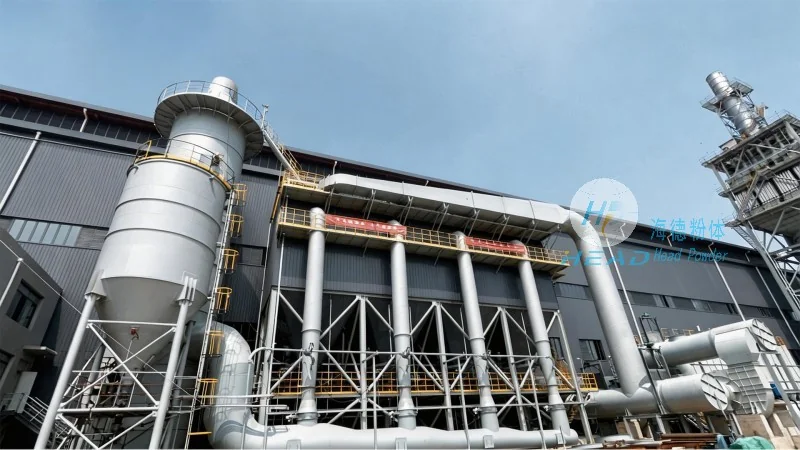
2. Space Savings: Unlike traditional conveyors, pneumatic systems require minimal floor space, allowing for more efficient plant layouts and easier integration into existing facilities.
3. Reduced Maintenance: With fewer moving parts and less mechanical wear, pneumatic systems experience lower maintenance requirements and longer service life.
4. Improved Safety: Enclosed pipelines and controlled air flow minimize dust exposure and reduce the risk of material spillage, enhancing workplace safety.
As a leading provider of engineering solutions, HeadPowder, Shandong HeadPowder Engineering Co., Ltd., is dedicated to delivering high-quality pneumatic conveying systems for mineral sand transport. With a strong presence in Shandong, China, the company leverages its expertise and local resources to offer tailored solutions that meet the specific needs of clients in the mineral processing industry. By focusing on innovation, reliability, and customer satisfaction, HeadPowder ensures that its clients achieve optimal performance and operational efficiency in their mineral sand handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top