With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Phosphate fertilizer is a crucial component in modern agriculture, providing essential nutrients for plant growth. The efficient and reliable transportation of phosphate fertilizer powder is a critical aspect of the supply chain, directly impacting production efficiency and product quality. This article provides an overview of phosphate fertilizer powder conveying systems, with a focus on the advantages of pneumatic conveying technology.
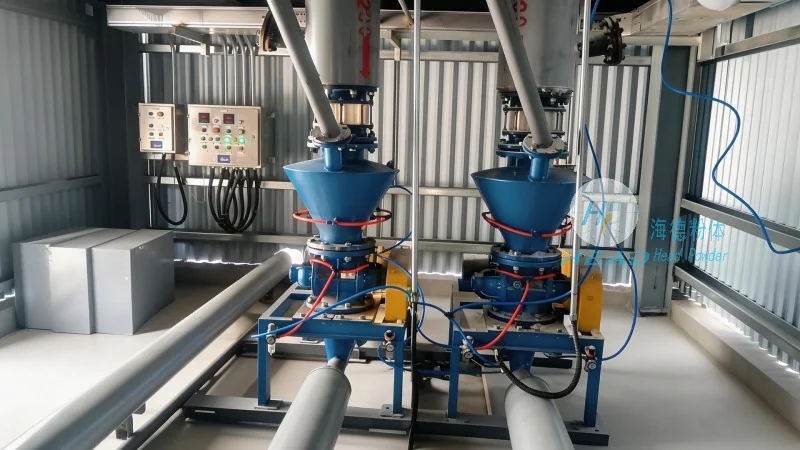
Phosphate fertilizer powder conveying systems are designed to transport bulk phosphate fertilizer from storage facilities to processing plants or distribution centers. These systems are engineered to handle the unique properties of phosphate fertilizer, such as its fine particle size, hygroscopic nature, and potential for dust generation. The primary goal of these systems is to ensure safe, efficient, and cost-effective movement of the material while minimizing operational risks and environmental impact.
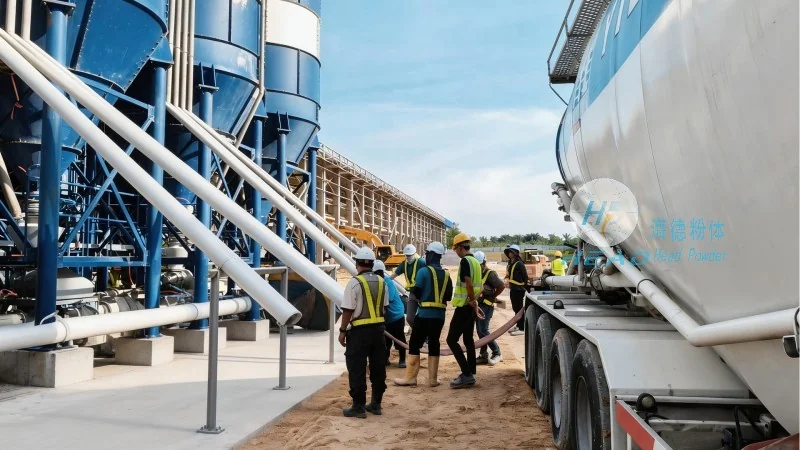
Pneumatic conveying, also known as air-pneumatic transport, is a widely adopted method for transporting phosphate fertilizer powder due to its numerous advantages over traditional mechanical conveying systems. One of the key benefits is the ability to handle fine and abrasive materials without causing excessive wear on equipment. Pneumatic systems can also provide a closed-loop operation, reducing dust emissions and improving workplace safety. Additionally, these systems offer flexibility in layout, allowing for vertical and horizontal transportation with minimal space requirements. The self-cleaning capabilities of pneumatic lines further enhance operational efficiency by preventing material buildup and blockages.
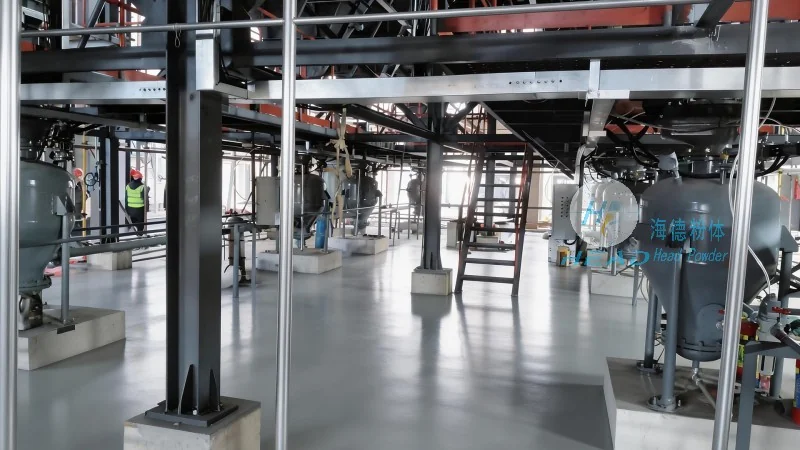
Modern pneumatic conveying systems for phosphate fertilizer powder incorporate several advanced features to optimize performance. These include high-pressure or low-pressure air systems, depending on the distance and material characteristics. The use of rotary air locks and check valves ensures proper material flow and prevents backflow. Additionally, the integration of dust collection and filtration systems maintains air quality and complies with environmental regulations. The modular design of these systems allows for easy expansion or modification to accommodate changing production needs.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading provider of advanced phosphate fertilizer powder conveying systems. With a strong presence in China, particularly in Shandong province, HeadPowder specializes in designing and manufacturing customized solutions tailored to the specific requirements of fertilizer manufacturers. The company's expertise lies in integrating pneumatic conveying technology with other processing equipment, ensuring seamless integration into existing production lines. HeadPowder's commitment to quality and innovation has made it a trusted partner for clients seeking reliable and efficient conveying solutions for phosphate fertilizer powder.
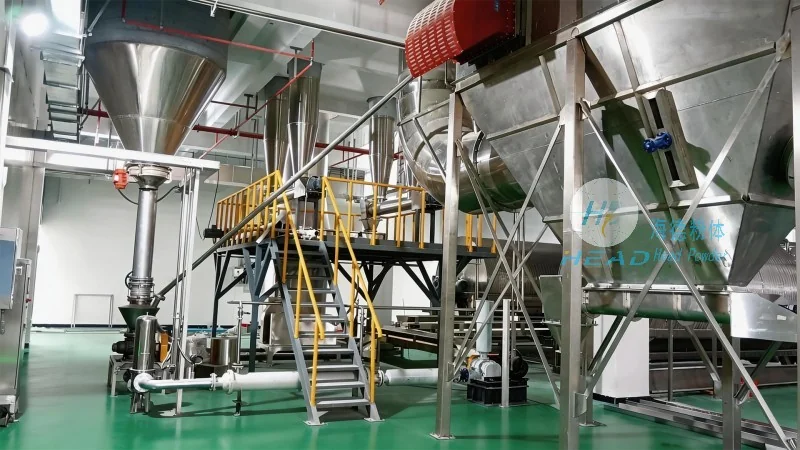
As the demand for phosphate fertilizer continues to grow, the importance of efficient conveying systems cannot be overstated. Pneumatic conveying technology offers a superior solution for transporting phosphate fertilizer powder, combining reliability, safety, and operational efficiency. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in advancing this technology, providing tailored systems that meet the evolving needs of the agricultural industry. By leveraging the advantages of pneumatic conveying, fertilizer manufacturers can enhance productivity, reduce costs, and ensure the consistent quality of their products.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top