With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider of dust handling solutions, specializes in the design, manufacturing, and installation of advanced dust transport systems. Based in Shandong, China, the company has established itself as a trusted partner for industries requiring efficient and reliable dust removal and transportation. This article provides an overview of dust transport systems, highlighting the key advantages of pneumatic conveying technology.
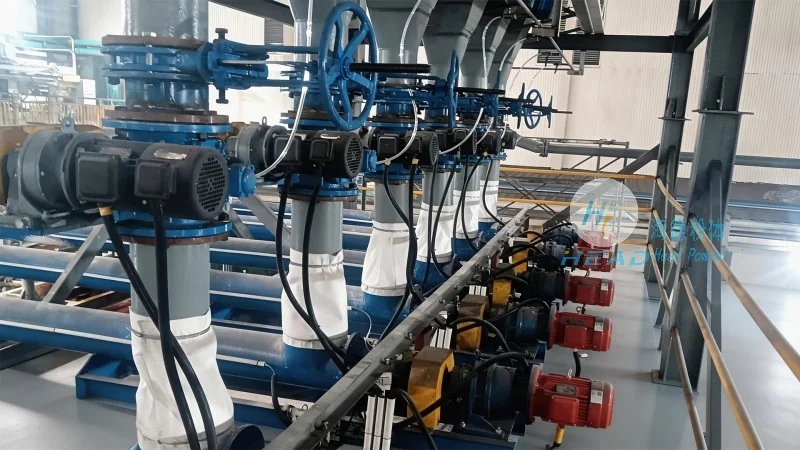
Dust transport systems are essential for managing airborne particles in various industrial applications. These systems are designed to collect, transport, and deposit dust or powders from one location to another, ensuring compliance with environmental regulations and maintaining operational efficiency. The primary goal is to minimize dust dispersion, improve workplace safety, and enhance overall process performance.
Pneumatic conveying, also known as air conveying, is a widely adopted method for dust transport due to its numerous benefits. Unlike traditional mechanical systems, pneumatic conveyors use air pressure to move materials, offering flexibility in system design and operation. Key advantages include:
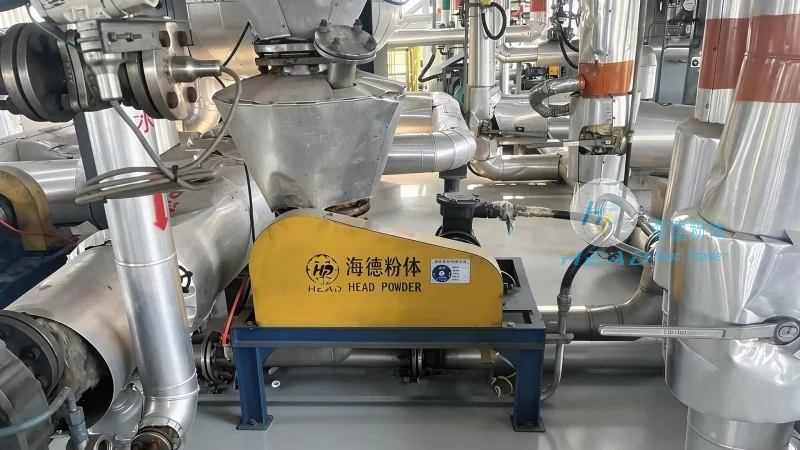
Shandong HeadPowder Engineering Co., Ltd. leverages decades of experience in the dust handling industry to deliver customized dust transport systems. The company's team of engineers and technicians works closely with clients to understand their specific needs, whether it's for new installations or system upgrades. HeadPowder's solutions are tailored to meet the unique requirements of each application, ensuring optimal performance and long-term durability.
A typical pneumatic dust transport system consists of several critical components that work together to ensure efficient operation. These include:
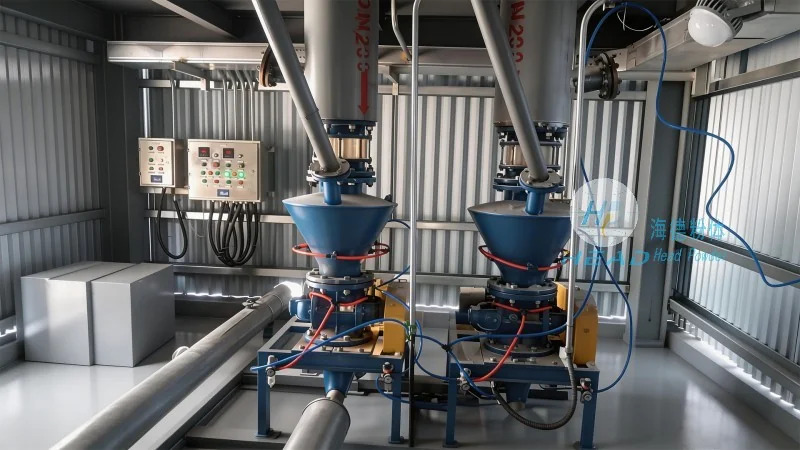
Dust transport systems are used in a variety of industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. In each of these sectors, the systems play a crucial role in maintaining operational efficiency and safety. For example, in pharmaceutical plants, dust transport systems help manage powders used in drug production, ensuring that the process remains sterile and compliant with regulatory standards. In food processing facilities, these systems are essential for handling ingredients and preventing contamination.
Efficient dust transport is a critical aspect of modern industrial operations. Pneumatic conveying offers a reliable and effective solution for moving dust and powders, with numerous advantages over traditional methods. Shandong HeadPowder Engineering Co., Ltd. is committed to providing high-quality dust transport systems that meet the evolving needs of industries worldwide. By leveraging advanced technology and expert engineering, HeadPowder ensures that clients receive systems that are not only efficient but also durable and environmentally responsible.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top