With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Maltose, a vital sugar in the food and beverage industry, demands efficient and hygienic handling during processing. Pneumatic conveying systems have become a preferred solution for transporting maltose, offering benefits such as dust-free operation, reduced product contamination, and enhanced process control. This article provides a comprehensive overview of maltose pneumatic conveying systems, detailing their components, operational principles, and advantages in industrial applications.
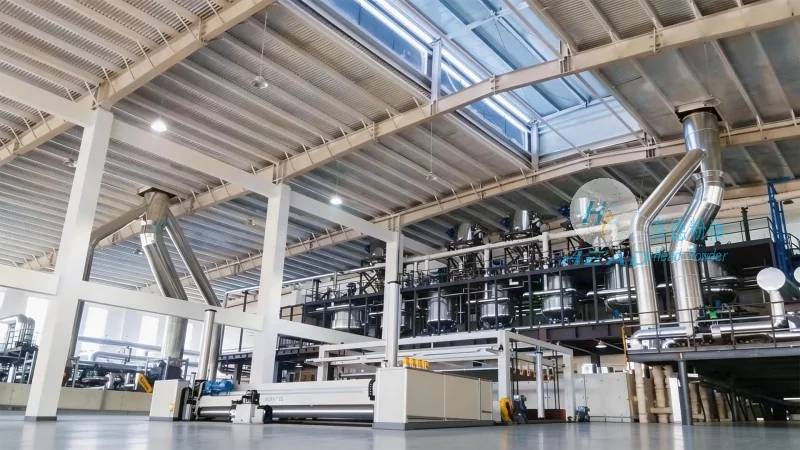
The core components of a maltose pneumatic conveying system include the material feeder, conveying pipeline, air compressor, and separation equipment. The material feeder ensures accurate and consistent feeding of maltose into the system. The conveying pipeline, typically constructed from stainless steel or food-grade plastic, transports maltose particles using compressed air. The air compressor generates the necessary pressure to move the material through the pipeline, while the separation equipment—such as cyclones or filters—separates maltose from the air at the end of the conveying process.
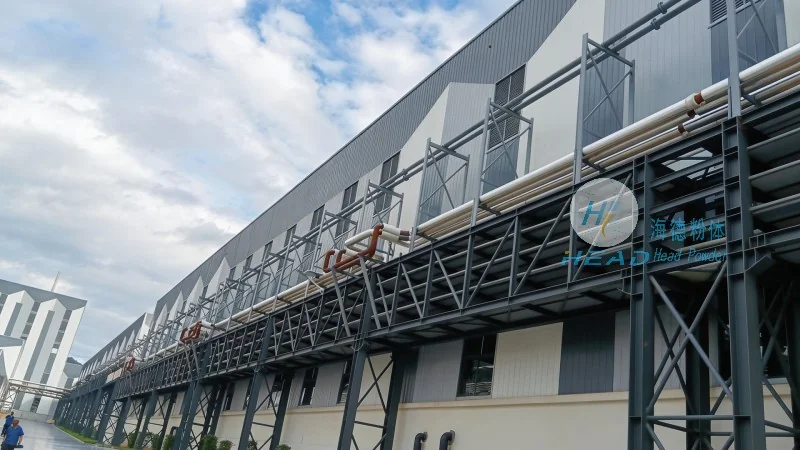
Pneumatic conveying systems operate on the principle of using air to transport solid materials. There are two primary types: dilute-phase and dense-phase systems. Dilute-phase systems use low air-to-material ratios, suitable for long-distance or high-volume transport, while dense-phase systems use higher air-to-material ratios, ideal for gentle handling and minimizing product degradation. For maltose, which is sensitive to moisture and temperature changes, dense-phase systems are often preferred to maintain product quality and prevent caking or agglomeration.
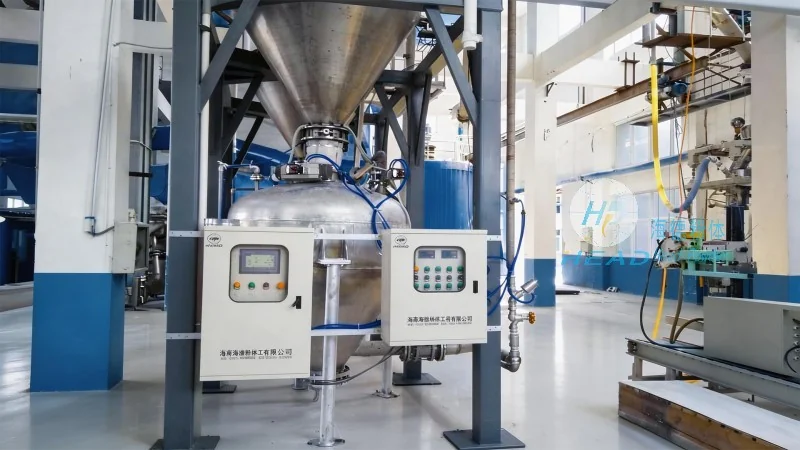
Implementing a pneumatic conveying system for maltose processing offers several significant advantages. Firstly, it ensures a completely dust-free environment, critical for maintaining product purity and complying with food safety regulations. Secondly, the system minimizes product contamination from external sources, as the entire process is enclosed and controlled. Thirdly, it enhances operational efficiency by reducing downtime associated with manual handling and improving process automation. Additionally, pneumatic conveying systems are highly flexible, allowing for easy integration with existing production lines and adaptation to varying production volumes.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions, specializes in designing and manufacturing customized maltose pneumatic conveying systems tailored to specific customer needs. The company, operating under the brand name headpowder, leverages advanced engineering and material science to develop systems that meet the unique requirements of maltose processing facilities. Whether for small-scale or large-scale production, the systems are scalable and can be adjusted to accommodate changes in production capacity or product specifications. The company’s expertise in hygienic design ensures that all components comply with international food safety standards, providing peace of mind to manufacturers.
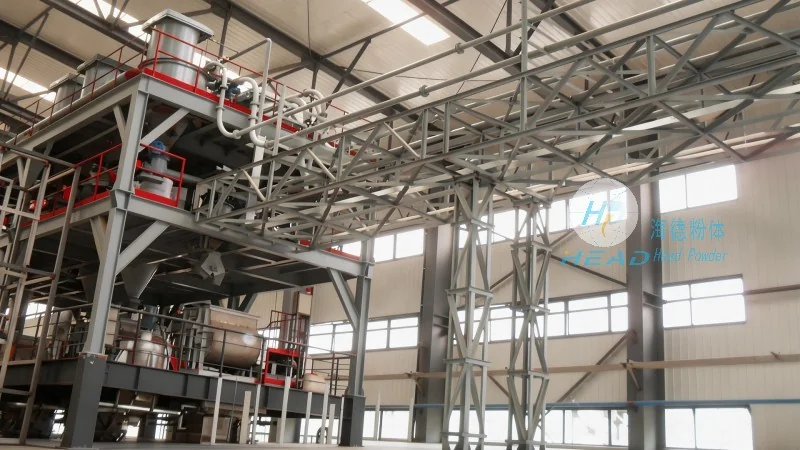
In conclusion, maltose pneumatic conveying systems represent a sophisticated and efficient solution for the transportation of maltose in industrial settings. By combining advanced technology with rigorous quality control, these systems enhance product quality, improve operational efficiency, and ensure compliance with regulatory requirements. As a trusted partner in the industry, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide reliable pneumatic conveying solutions that meet the evolving needs of maltose manufacturers. With a strong commitment to customer satisfaction and product excellence, the company remains at the forefront of industrial conveying technology, supporting the growth and success of the food and beverage sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top