With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
In the modern industrial landscape, the efficient management of chemical powders is critical for maintaining operational continuity and environmental compliance. Among these, the transfer of Sodium Bicarbonate for desulfurization processes stands out as a specialized requirement. The Sodium Bicarbonate Desulfurization Powder Pneumatic Conveying System serves as the backbone of these operations, ensuring that the chemical is transported from storage to the reaction point with minimal loss and maximum efficiency. This article provides a detailed overview of the technical aspects, design considerations, and the specialized services provided by industry leaders in this field.
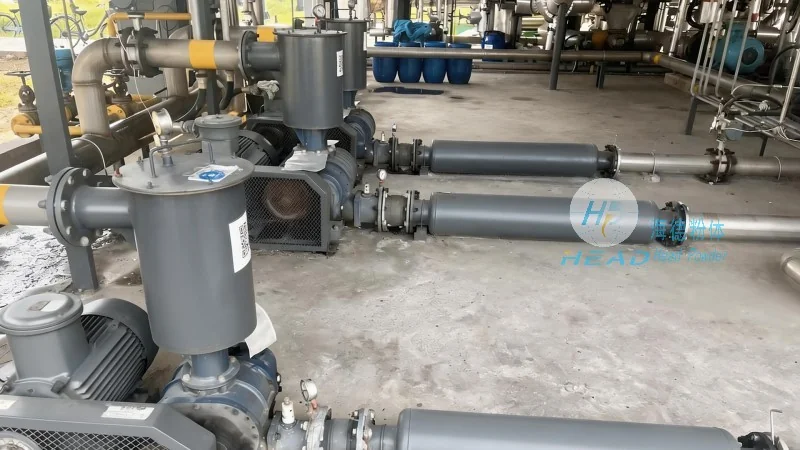
Sodium bicarbonate, known chemically as NaHCO3, is a widely utilized agent for flue gas desulfurization due to its high reactivity and purity. When applied to industrial flue gases, it effectively neutralizes sulfur dioxide (SO2) to form solid sodium sulfite and sulfate, which can then be easily removed. However, the effectiveness of this process relies heavily on the consistency and speed of the powder delivery. This is where the Sodium Bicarbonate Desulfurization Powder Pneumatic Conveying Solution becomes indispensable. By utilizing air pressure or vacuum to move the powder through enclosed pipelines, the system ensures that the chemical reaches the absorption tower or spray tower at the precise moment it is needed, preventing clumping and ensuring a uniform reaction rate.
Transitioning from mechanical screw conveyors to a Sodium Bicarbonate Desulfurization Powder Pneumatic Conveying System offers numerous operational benefits. The primary advantage is the fully enclosed nature of the transport, which significantly reduces dust emissions. In an industrial setting, where airborne particulates can be hazardous to workers and equipment, this containment is vital. Furthermore, pneumatic conveying allows for longer distances and higher elevations compared to traditional mechanical methods. The system is also highly automated, reducing the need for manual intervention and lowering labor costs. By maintaining a constant flow rate, the system helps stabilize the pH levels in the scrubber, leading to better overall desulfurization efficiency and compliance with environmental regulations.
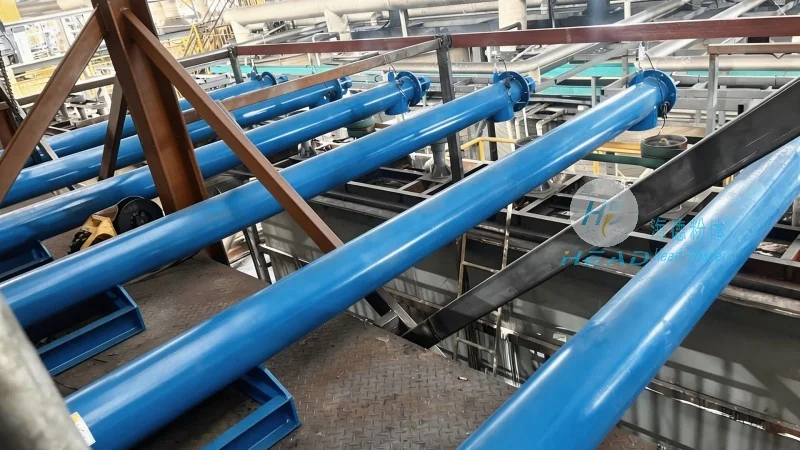
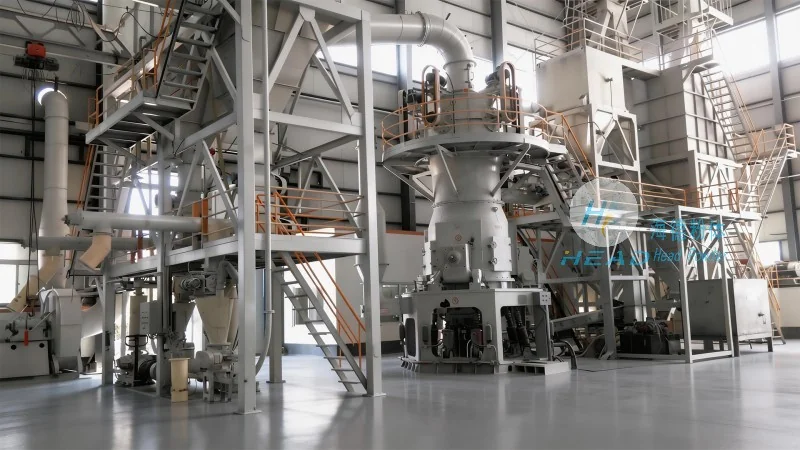
Every industrial plant has unique spatial constraints, flow requirements, and chemical properties. Therefore, a one-size-fits-all approach is rarely effective. A professional Sodium Bicarbonate Desulfurization Powder Pneumatic Conveying Manufacturer will emphasize the importance of customization. The Sodium Bicarbonate Desulfurization Powder Pneumatic Conveying Solution must be tailored to the specific layout of the plant, including the distance between the silo and the scrubber, the number of bends in the pipeline, and the required throughput capacity. Whether the facility requires a positive pressure system to push the powder over long distances or a negative pressure system to pull powder into a vacuum zone, the design must be precise. Customization also involves selecting the appropriate pipe diameter and air-to-material ratio to prevent pipe blockages and ensure smooth flow.
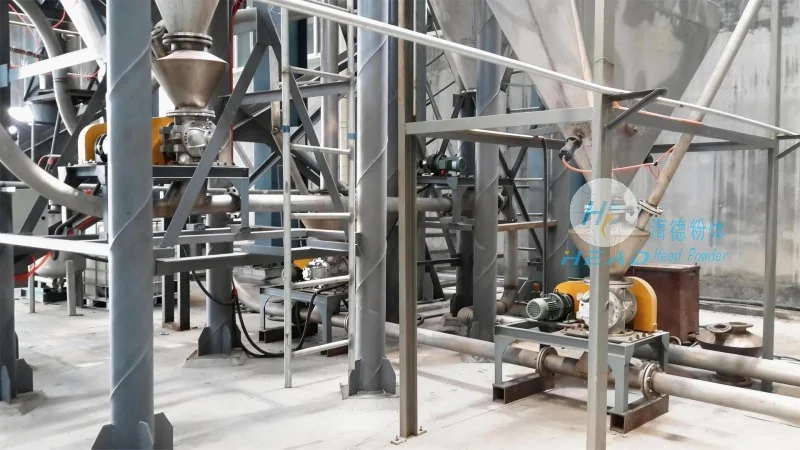
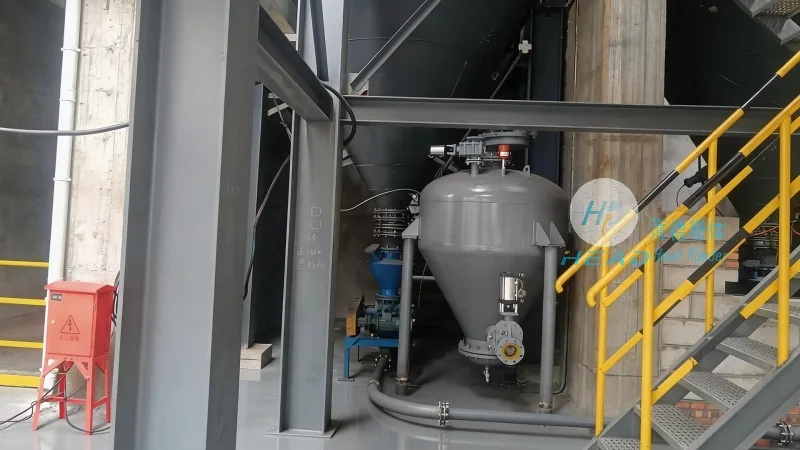
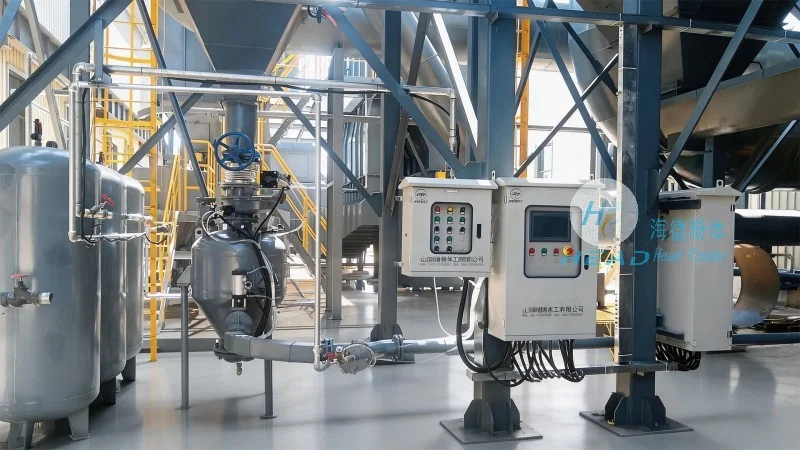
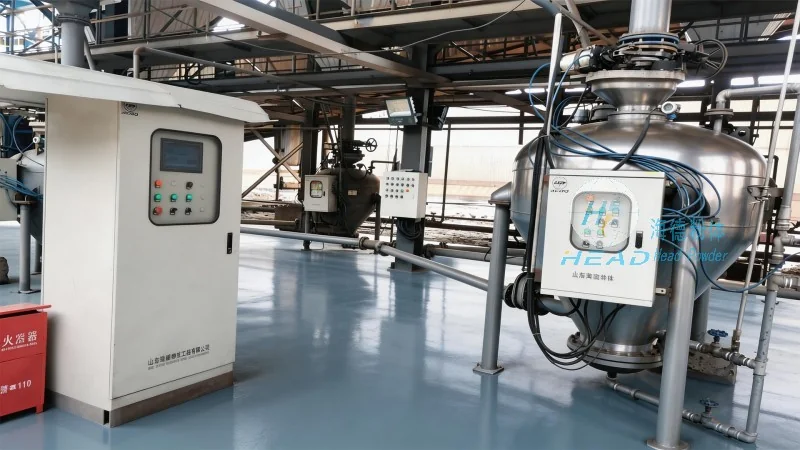
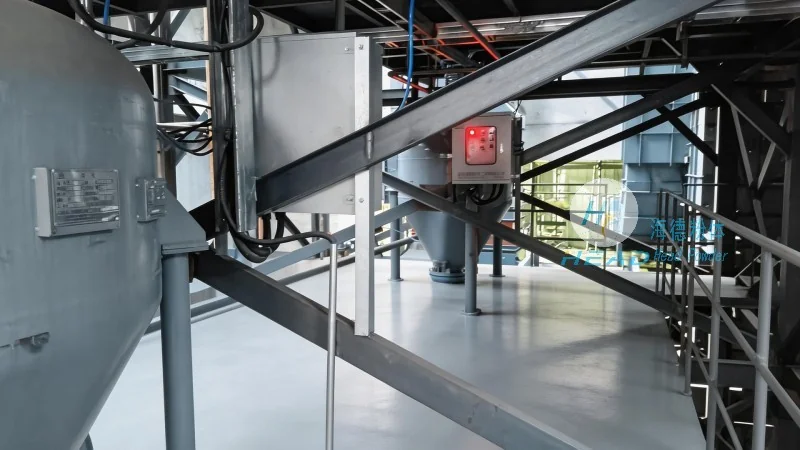
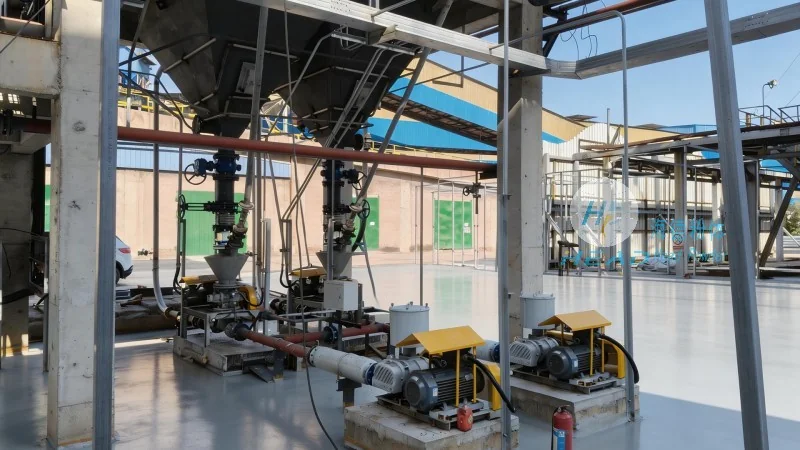
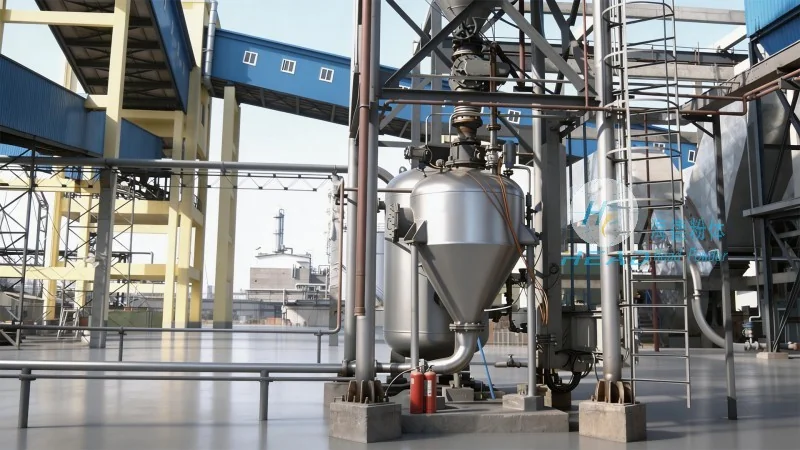
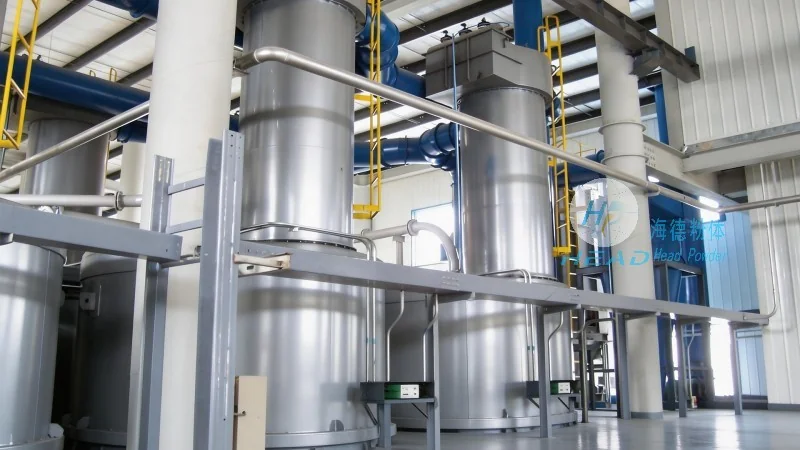
A high-quality Sodium Bicarbonate Desulfurization Powder Pneumatic Conveying System comprises several critical components working in unison. The process typically begins with a bulk storage silo equipped with level sensors to monitor inventory. From the silo, a rotary valve or a screw feeder meters the powder into the conveying line. The heart of the system is the pneumatic conveying pump, which utilizes compressed air to fluidize the powder and transport it through the pipeline. Along the path, specialized dust collectors and filters ensure that the air is cleaned before it is released back into the atmosphere. Additionally, the system is equipped with safety valves and pressure relief devices to handle potential surges in pressure. These components are engineered to withstand the abrasive nature of the powder, ensuring longevity and reliability.
When selecting a partner for such a critical infrastructure project, expertise and reliability are paramount. Shandong Headpowder Engineering Co., Ltd. stands out as a premier provider in the industry. As a dedicated Sodium Bicarbonate Desulfurization Powder Pneumatic Conveying Manufacturer, the company combines advanced engineering principles with practical field experience. Their team understands the nuances of handling fine powders and the specific challenges of desulfurization processes. By choosing Headpowder, clients gain access to comprehensive design services, from initial feasibility studies to final installation and commissioning. The company's commitment to quality ensures that every Sodium Bicarbonate Desulfurization Powder Pneumatic Conveying System delivered meets international standards for performance and safety.
For companies looking to upgrade their desulfurization infrastructure or require a new installation, direct communication with the engineering team is essential. Shandong Headpowder Engineering Co., Ltd. is strategically located in Shandong, China, serving clients both locally and internationally. To discuss your specific requirements and obtain a tailored Sodium Bicarbonate Desulfurization Powder Pneumatic Conveying Solution, please contact Mr. Zhang, the contact person at the company. You may reach him via WeChat at 15662777102. The team at Headpowder is ready to provide the technical support and professional service needed to optimize your powder handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top