With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Welcome to the world of efficient sugar powder handling, where the seamless transport of granular sweeteners is crucial for industrial processes. This article provides a comprehensive overview of sugar powder conveying systems, focusing on the structural design and operational principles that enable reliable material movement. As a key component in the food processing and bulk material handling industries, these systems are engineered to meet the demands of high-volume production while ensuring product integrity and operational efficiency.
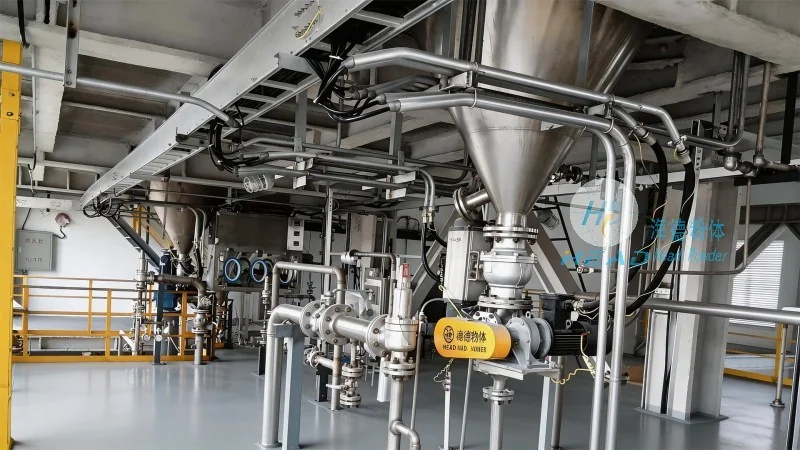
At the heart of advanced sugar powder conveying solutions is Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in bulk material handling equipment. With a strong presence in China, particularly in Shandong province, HeadPowder has established itself as a trusted provider of innovative conveying systems tailored to the unique challenges of sugar and other fine powders. The company's commitment to quality, reliability, and customer satisfaction drives its development of cutting-edge technologies that enhance the performance of industrial conveying operations.
Sugar powder conveying systems are designed to transport granular or powdered sugar from storage silos to processing lines, packaging units, or other destinations within a facility. These systems must address several critical factors, including the prevention of material degradation, the minimization of dust generation, and the maintenance of consistent flow rates. The structural design of these systems plays a pivotal role in achieving these objectives, as it directly impacts the efficiency and safety of the conveying process.
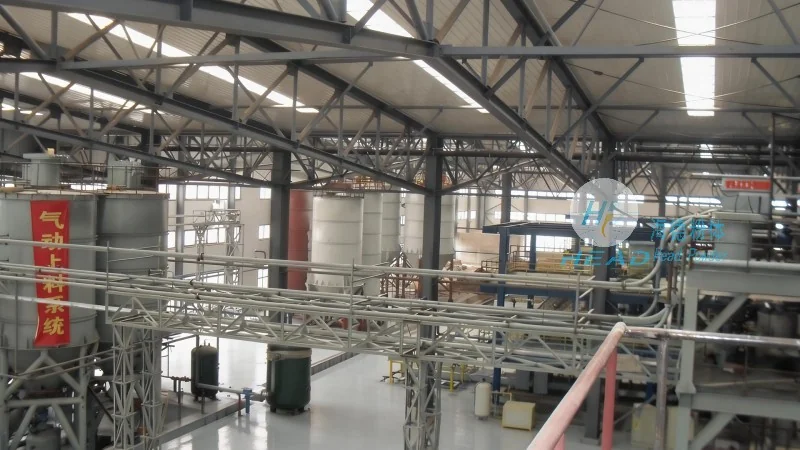
The core components of a typical sugar powder conveying system include the hopper, conveyor, and control mechanisms. The hopper, often equipped with a feeder or gate, serves as the initial storage and feeding unit, ensuring a steady supply of material to the conveyor. The conveyor itself, which may be a screw conveyor, pneumatic conveyor, or belt conveyor, is responsible for the actual movement of the sugar powder. Each component is engineered to handle the specific characteristics of sugar, such as its fine particle size and potential for caking or bridging, thereby preventing blockages and ensuring smooth operation.
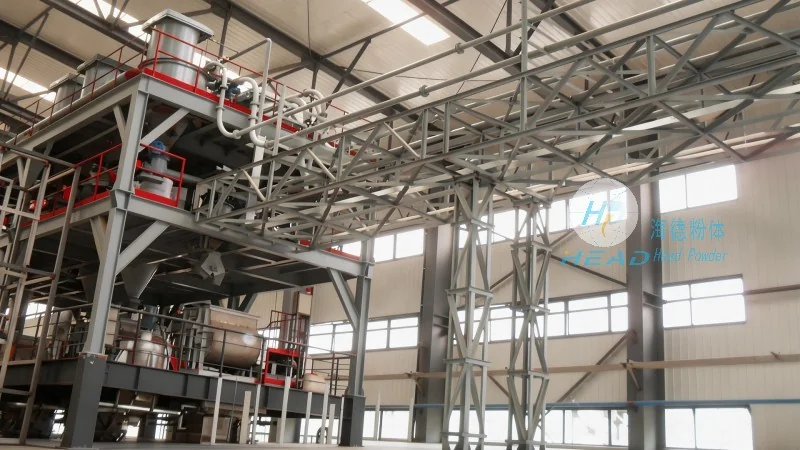
The operational principle of sugar powder conveying systems revolves around the controlled movement of material through the system. For example, a screw conveyor uses rotating screws to push material forward, while a pneumatic conveyor utilizes air pressure to transport the powder in a sealed pipeline. The choice of conveying method depends on factors such as the required flow rate, the distance to be covered, and the need to maintain product purity. In all cases, the system is designed to minimize friction and abrasion, which could affect the quality of the sugar powder. Additionally, features like dust collection and air filtration are integrated to ensure a clean and safe working environment.
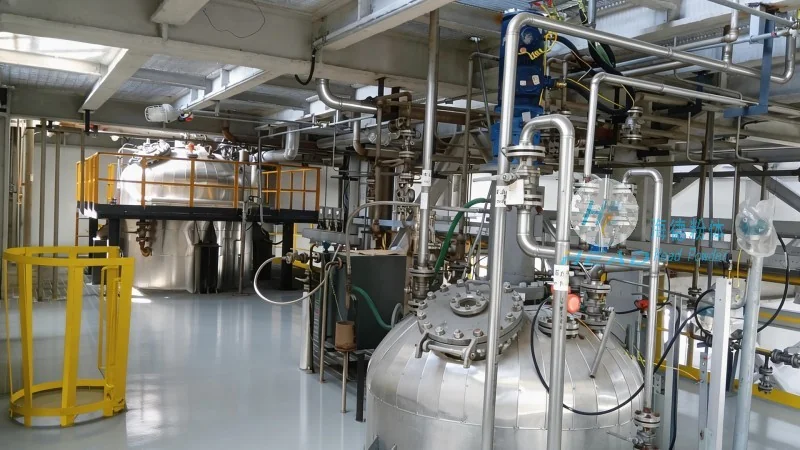
Implementing an efficient sugar powder conveying system offers numerous benefits for industrial operations. These include improved productivity through reduced downtime and increased throughput, enhanced product quality by preventing contamination and degradation, and operational cost savings from lower maintenance requirements and energy consumption. The reliability of modern conveying systems also contributes to better inventory management and supply chain efficiency, making them indispensable in the sugar processing industry.
As the demand for high-quality sugar products continues to grow, the importance of reliable sugar powder conveying systems cannot be overstated. Shandong HeadPowder Engineering Co., Ltd. remains dedicated to advancing the technology and design of these systems, ensuring that clients receive solutions that are tailored to their specific needs. By focusing on structural integrity, operational efficiency, and customer satisfaction, HeadPowder provides the foundation for successful bulk material handling in the sugar industry and beyond.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top