With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications in the fertilizer sector, efficient and reliable material handling is crucial. The fertilizer pneumatic conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., offers a sophisticated solution to transport bulk fertilizers with precision and minimal operational costs. This equipment is designed to meet the demanding requirements of modern fertilizer production and distribution, ensuring smooth material flow from storage to processing or packaging stages. The system's design integrates advanced engineering principles to optimize performance, durability, and energy efficiency, making it a preferred choice for companies operating in the fertilizer industry.
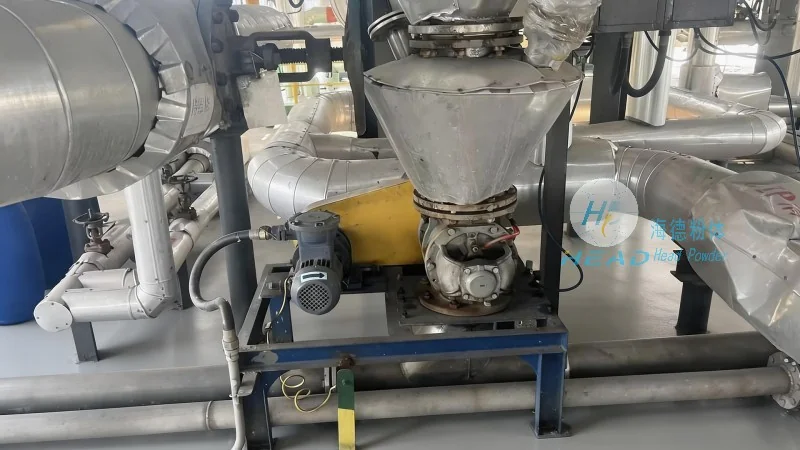
The fertilizer pneumatic conveying system consists of several key components that work in tandem to achieve effective material transport. The primary components include the hopper, feeder, air compressor, conveying pipeline, and receiver. The hopper is responsible for storing the bulk fertilizer, providing a consistent feed to the feeder. The feeder, often a rotary valve or screw feeder, regulates the flow of fertilizer into the conveying line, ensuring a controlled and steady supply. The air compressor generates the necessary air pressure to create a flow of air through the pipeline, which carries the fertilizer particles. The conveying pipeline, typically made of stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of fertilizer and maintain air tightness. The receiver collects the conveyed fertilizer at the destination point, such as a processing plant or storage silo. The system may also include additional components like filters, silencers, and pressure regulators to enhance performance and safety.
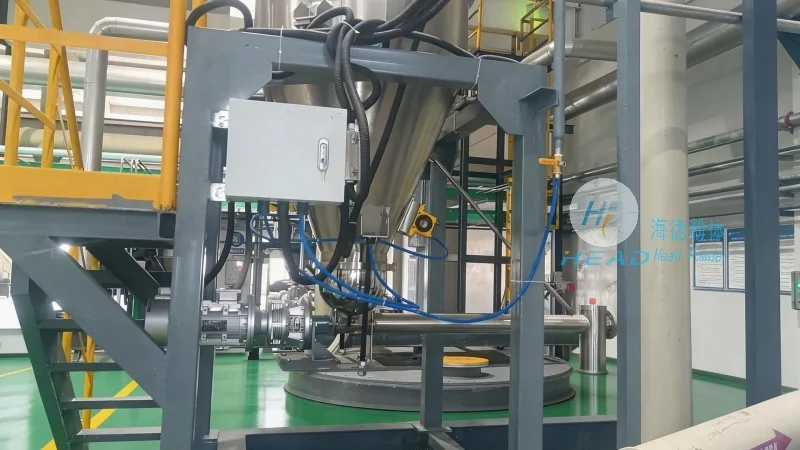
The working principle of the system is based on the principle of pneumatic transport, where air is used as the medium to move solid particles. When the feeder introduces fertilizer into the pipeline, the air compressor supplies high-pressure air. This air creates a flow that entrains the fertilizer particles, forming a dense phase or dilute phase flow depending on the system design. The system can operate in either positive pressure or negative pressure modes. In positive pressure systems, air is forced into the pipeline, pushing the fertilizer forward. In negative pressure systems, air is drawn out of the pipeline, pulling the fertilizer along. The choice between these modes depends on the specific application and the distance of material transport. The system's efficiency is optimized by controlling the air flow rate and pressure, ensuring that the fertilizer particles are transported without excessive wear on the equipment or degradation of the material. The control system monitors parameters such as pressure, flow rate, and particle concentration, adjusting the air supply to maintain optimal transport conditions.
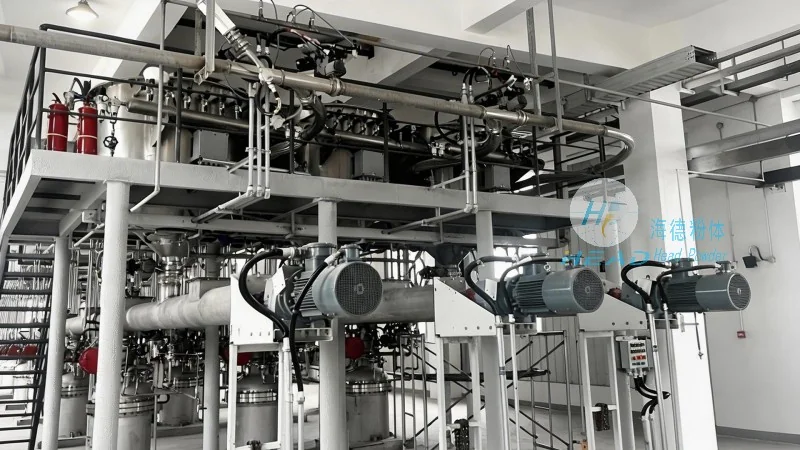
Shandong HeadPowder Engineering Co., Ltd.'s fertilizer pneumatic conveying system equipment is equipped with several features that enhance its performance and reliability. One of the key advantages is the ability to handle a wide range of fertilizer types, including granular, powdered, and even wet or sticky materials, with minimal maintenance. The system's design minimizes product degradation and contamination, preserving the quality of the fertilizer during transport. The use of stainless steel components ensures durability and resistance to corrosion, which is essential for long-term operation in harsh industrial environments. Additionally, the system is designed for easy integration into existing production lines, with modular components that allow for flexible configuration and expansion as production needs change. The control system is user-friendly, with intuitive interfaces that enable operators to monitor and adjust the system parameters in real-time, ensuring optimal performance and energy efficiency. The system also includes safety features such as pressure relief valves and overcurrent protection to prevent accidents and equipment damage.
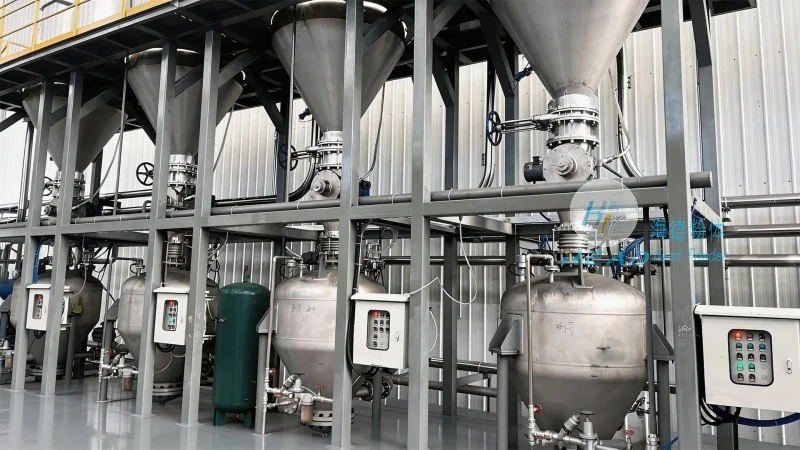
The fertilizer pneumatic conveying system is widely used in various stages of fertilizer production and handling. It is commonly employed in the transfer of raw materials from storage silos to processing units, in the movement of finished products from the production line to packaging facilities, and in the distribution of bulk fertilizer to storage or shipping locations. The system's ability to handle large volumes of material efficiently reduces labor costs and improves overall production throughput. By eliminating the need for manual handling or traditional conveyor systems, the pneumatic conveying system minimizes the risk of product spillage and contamination, enhancing safety and hygiene in the workplace. The system also contributes to energy savings by optimizing air usage and reducing the need for additional mechanical equipment. Overall, the fertilizer pneumatic conveying system provides a cost-effective and sustainable solution for material handling in the fertilizer industry, supporting the efficient operation of modern fertilizer plants. The system's adaptability allows it to be used in both new plant installations and as upgrades to existing facilities, making it a versatile choice for companies looking to enhance their material handling capabilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top