With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for coffee bean powder processing. This article provides a detailed overview of the operation process and working principles of such systems, highlighting their efficiency and reliability in handling coffee bean powders.
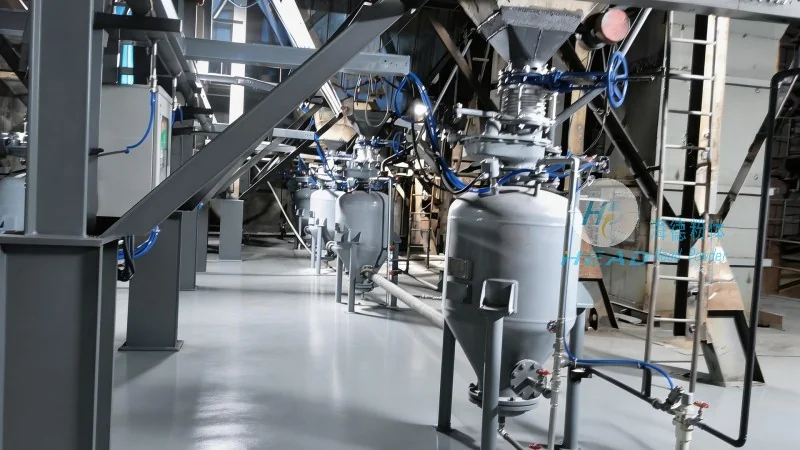
The coffee bean powder pneumatic conveying system consists of several critical components that work in tandem to ensure smooth material transport. These include the hopper for material storage, the air compressor or blower that generates the conveying air, the pipeline network for transporting the powder, and the control system that regulates the flow. Each component plays a vital role in maintaining the system's performance and safety.
The core working principle of the coffee bean powder pneumatic conveying system is based on the use of air pressure to move the powder particles through a pipeline. When the system is activated, the air compressor or blower creates a high-pressure air stream. This air stream is then introduced into the hopper, where it lifts the coffee bean powder particles and carries them through the pipeline to the destination point, such as a storage silo or processing unit. The system relies on the principle of fluidization, where the air flow creates a suspended state of the powder particles, allowing them to be transported without the need for mechanical conveyors.
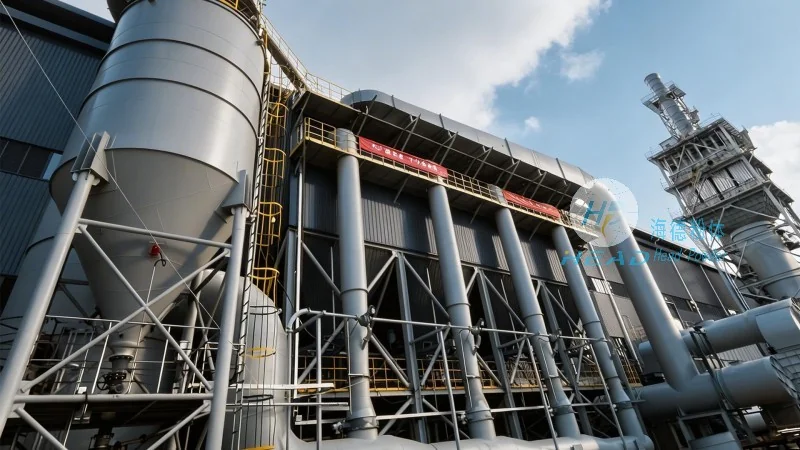
The operation process of the coffee bean powder pneumatic conveying system involves several key steps to ensure efficient and safe material handling. First, the coffee bean powder is loaded into the hopper, which is equipped with a feeding mechanism to control the flow rate. Next, the air compressor is started, and the air pressure is adjusted to the appropriate level for the specific powder characteristics. The system then begins to transport the powder through the pipeline, with the control system monitoring the flow rate and pressure to maintain optimal performance. Finally, the powder is discharged at the destination point, where it is collected and prepared for further processing or storage.
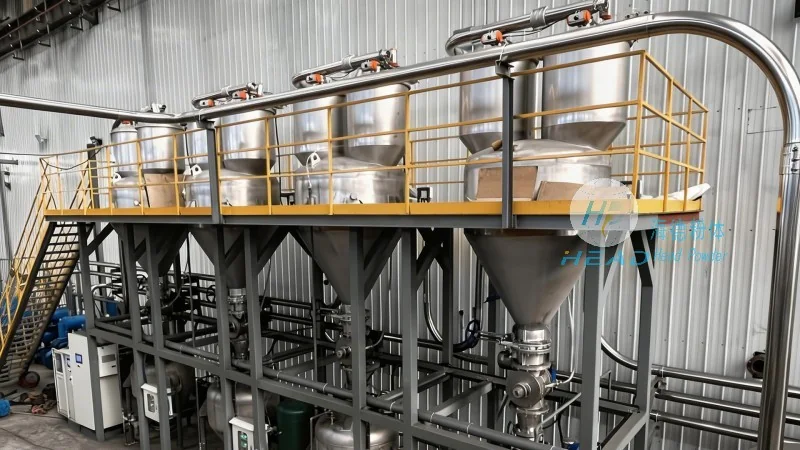
Compared to traditional mechanical conveyors, the coffee bean powder pneumatic conveying system offers several advantages. These include reduced product contamination due to the enclosed pipeline system, lower maintenance requirements as there are no moving parts in contact with the powder, and improved energy efficiency through optimized air flow management. Additionally, the system can handle a wide range of powder characteristics, including varying particle sizes and moisture content, making it suitable for diverse coffee processing applications.
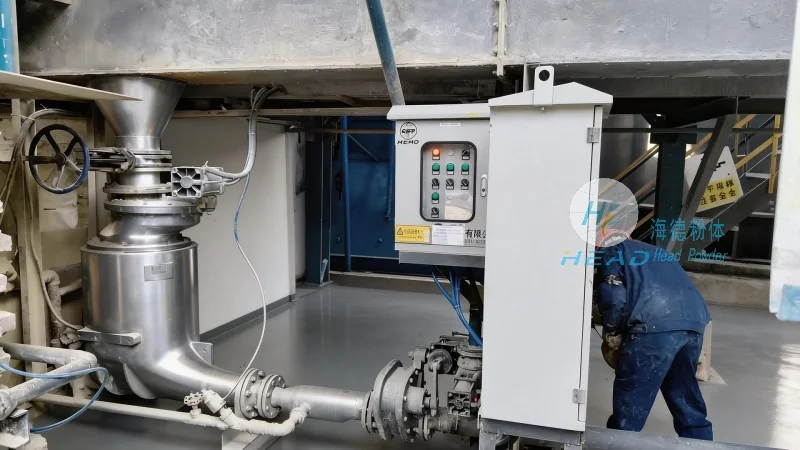
The coffee bean powder pneumatic conveying system is widely used in various stages of coffee processing, from raw bean handling to final product packaging. In the initial stages, the system can transport coffee beans from storage silos to grinding units, ensuring a consistent flow of raw material. During the grinding process, the system can convey the ground coffee powder to blending and packaging equipment, maintaining the quality and integrity of the product. Furthermore, the system is used in quality control processes, where it can transport samples of the powder for testing and analysis, ensuring that the final product meets the required standards.
To ensure the long-term performance and safety of the coffee bean powder pneumatic conveying system, regular maintenance and adherence to safety protocols are essential. Regular cleaning of the hopper and pipeline is necessary to prevent the accumulation of powder residue, which can affect the system's efficiency and cause blockages. The air compressor and blower should be inspected regularly for wear and tear, and the control system should be checked for proper functionality. Safety considerations include ensuring that the system is properly grounded to prevent electrical hazards and that all personnel are trained on the safe operation of the equipment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top