With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider of industrial material handling solutions, specializes in systems designed to ensure the safe and efficient transport of materials under nitrogen protection. This article explores the operation process and working principles of such systems, highlighting the critical role they play in maintaining product integrity and operational safety.
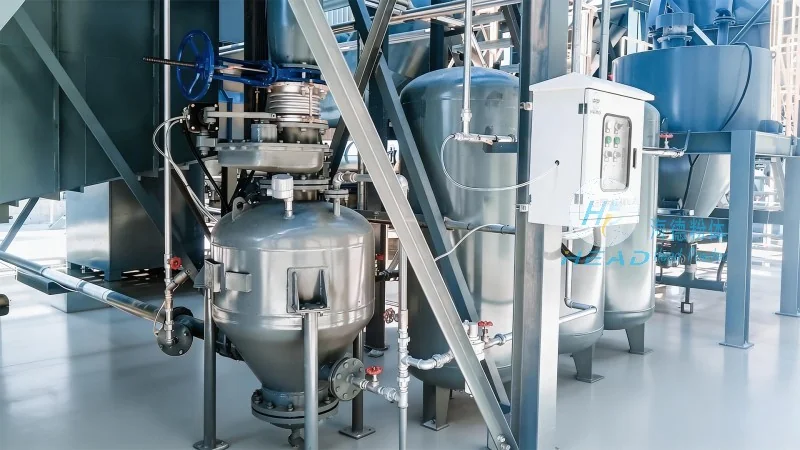
In many industrial applications, especially those involving sensitive materials like pharmaceuticals, food products, or chemicals that are prone to oxidation or contamination, maintaining an inert atmosphere during material transport is essential. Nitrogen protection systems are engineered to achieve this by displacing oxygen and other atmospheric gases with nitrogen, a gas that is inert and non-reactive. The process involves several key components and steps that work in concert to create a controlled environment for material conveyance.
The effectiveness of nitrogen protection in material conveying relies on a well-designed system comprising several critical components. These typically include nitrogen gas sources, such as high-purity nitrogen generators or cylinders, pressure regulators to control gas flow, and a network of pipes and ducts that distribute the nitrogen evenly throughout the conveying line. Additionally, the system may incorporate sensors and control panels to monitor and adjust nitrogen levels in real-time, ensuring consistent protection. The material handling equipment itself, such as pneumatic conveyors, screw conveyors, or bucket elevators, is integrated into this network to facilitate the transport of materials while maintaining the inert atmosphere.
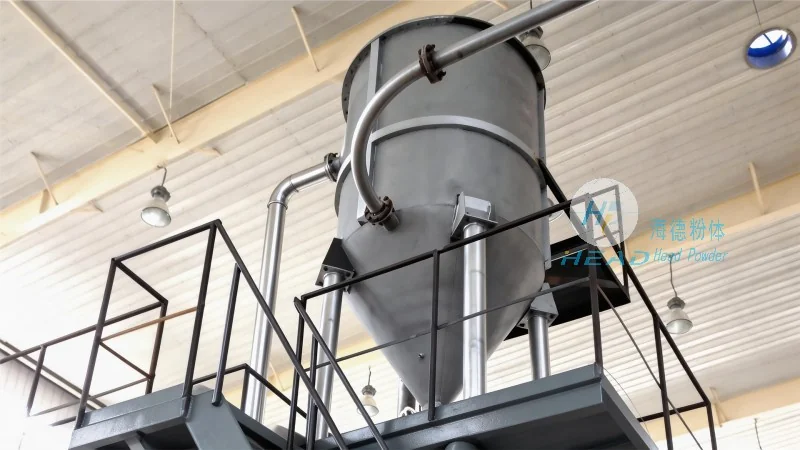
The operation process of a nitrogen-protected material conveying system begins with the preparation of the nitrogen supply. High-purity nitrogen is typically generated on-site or delivered from external sources and stored in tanks. The system then activates the nitrogen flow, which is regulated by pressure regulators to maintain a consistent pressure within the conveying line. As the nitrogen is introduced, it displaces the ambient air, creating a low-oxygen environment. The material to be conveyed is then introduced into the system, either manually or through automated feeding mechanisms. The conveying equipment, powered by the nitrogen flow, transports the material through the system. Throughout the process, sensors continuously monitor the nitrogen concentration and pressure, ensuring that the protective atmosphere is maintained at all times. Any deviations are immediately detected and corrected by the control system, preventing potential contamination or oxidation of the materials.
The working principle of nitrogen protection in material conveying is based on the concept of inert gas displacement. By introducing nitrogen, a non-reactive gas, into the conveying system, the oxygen content is reduced to a level that is insufficient to support combustion or chemical reactions that could degrade the material. This is achieved through a combination of gas flow control, pressure management, and continuous monitoring. The nitrogen acts as a barrier, preventing the entry of atmospheric contaminants and maintaining the purity of the conveyed materials. The system's design ensures that the nitrogen remains within the conveying line, minimizing the risk of leaks or exposure to external air. This principle is crucial for industries where product quality and safety are paramount, as any exposure to oxygen or moisture could lead to spoilage, corrosion, or other undesirable changes in the material.
Implementing nitrogen protection in material conveying offers several significant benefits. Firstly, it enhances product quality by preventing oxidation, moisture absorption, or contamination, which are common issues in traditional conveying methods. This is particularly important for sensitive materials like pharmaceuticals, where product integrity directly impacts efficacy and safety. Secondly, the system improves operational safety by reducing the risk of fire or explosion in environments where flammable materials are handled. The inert atmosphere created by nitrogen eliminates the presence of oxygen, which is a key component in combustion reactions. Thirdly, nitrogen protection systems can extend the lifespan of equipment by protecting it from corrosion and wear caused by moisture or chemical reactions. Finally, these systems contribute to cost savings by reducing the need for post-processing steps to remove contaminants or by minimizing material waste due to spoilage.
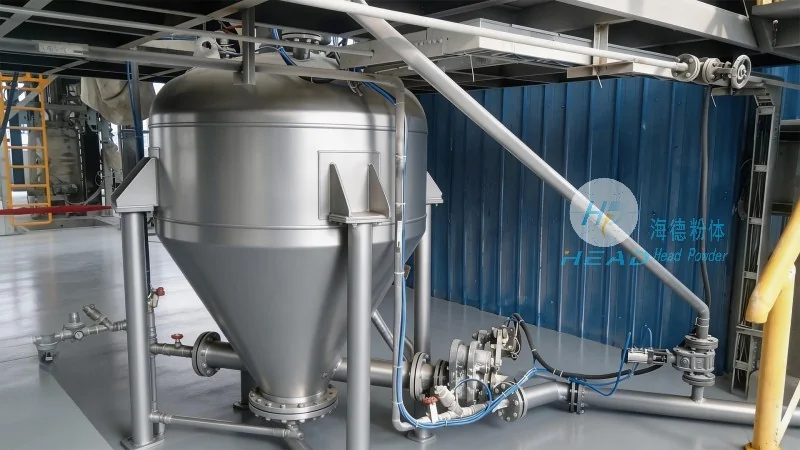
Nitrogen protection material conveying systems are widely used across various industries. In the pharmaceutical industry, they are essential for transporting active pharmaceutical ingredients (APIs) and finished dosage forms, ensuring that the products remain stable and free from contamination. In the food industry, such systems are used for conveying ingredients like powders, spices, and seasonings, maintaining the freshness and quality of the food products. The chemical industry also relies on nitrogen protection for handling reactive chemicals, preventing unwanted reactions and ensuring the safety of workers and equipment. Additionally, in the electronics manufacturing sector, nitrogen-protected conveyors are used to transport sensitive components, protecting them from moisture and dust that could affect their performance.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of advanced material handling solutions that incorporate nitrogen protection technology. The company's expertise lies in designing and manufacturing systems that meet the stringent requirements of various industries, ensuring reliable and safe material transport. By understanding the operation process and working principles of nitrogen protection in material conveying, industries can enhance their operational efficiency, product quality, and safety standards. HeadPowder continues to innovate and provide tailored solutions to meet the evolving needs of its clients, solidifying its position as a leader in the field of industrial material handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top