

Operation Process and Working Principle of PFA Powder Conveying System Equipment
The PFA powder conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is a specialized device designed for the efficient and reliable transportation of polytetrafluoroethylene (PFA) powder. As a leading manufacturer in the field, HeadPowder focuses on providing high-quality solutions tailored to the unique properties of PFA, which is known for its excellent chemical resistance, thermal stability, and non-stick characteristics. This system is engineered to handle PFA powder with precision, ensuring minimal loss and contamination during the conveying process.
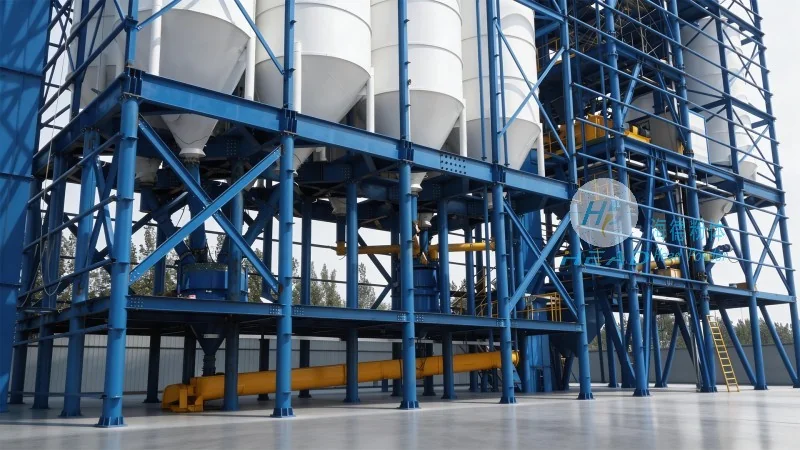
Key Components and Structure of the Conveying System
The PFA powder conveying system typically consists of several core components that work in tandem to achieve optimal performance. The main parts include a hopper for material storage, a rotary valve or feeder for controlled discharge, a conveyor (such as a pneumatic or mechanical conveyor), and a control system for monitoring and adjusting the conveying parameters. The hopper is designed with a smooth interior to prevent material buildup and ensure consistent flow. The rotary valve, often equipped with a variable speed drive, regulates the amount of powder released into the conveyor, preventing overloading and maintaining a steady feed rate. The conveyor itself may use air pressure (pneumatic) or mechanical means (like screw or belt conveyors) to transport the PFA powder from the hopper to the destination point. The control system integrates sensors and a user interface to monitor pressure, flow rate, and other critical parameters, allowing operators to adjust settings in real-time for optimal operation.
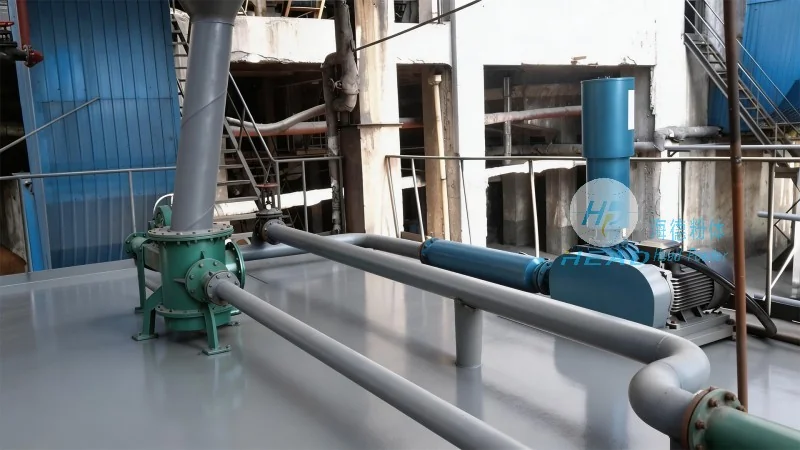
Operation Process of the PFA Powder Conveying System
The operation of the PFA powder conveying system follows a systematic process to ensure efficient material handling. First, the PFA powder is loaded into the hopper. The control system then activates the rotary valve, which opens to allow a controlled amount of powder to enter the conveyor. The conveyor, driven by compressed air or mechanical power, transports the powder through the system. The speed of the conveyor and the rotation speed of the rotary valve are adjusted based on the required flow rate and the characteristics of the PFA powder. During the conveying process, the system continuously monitors pressure and flow to prevent blockages or overloading. If any issues are detected, the control system automatically adjusts the settings or stops the system to prevent damage. The powder is then discharged at the end of the conveyor into the target container or processing equipment. This process is repeated as needed, with the system maintaining a consistent and reliable flow of PFA powder throughout the operation.
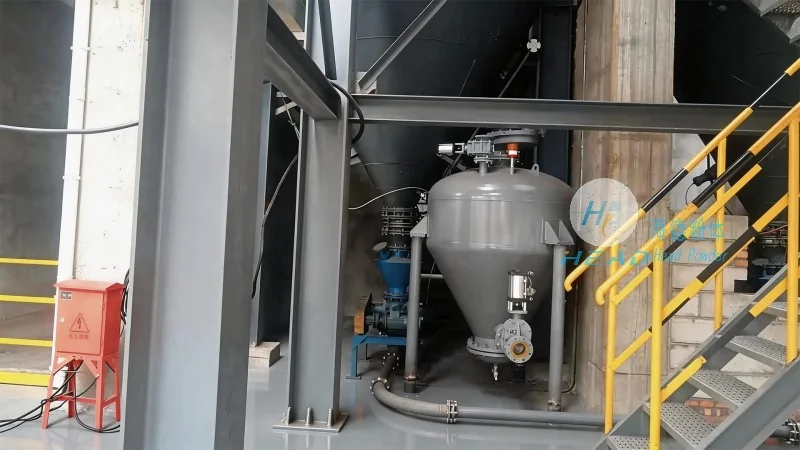
Working Principle of the PFA Powder Conveying System
The working principle of the PFA powder conveying system is based on the principles of fluidization and pneumatic transport. The system uses compressed air to create a flow of air and powder mixture, which allows the PFA powder to be transported through the system. The rotary valve acts as a metering device, controlling the amount of powder that enters the conveyor. The conveyor then transports the powder using the air flow, ensuring that the powder remains suspended and moves smoothly. The control system plays a crucial role in maintaining the balance between air and powder, ensuring that the powder is not over-diluted or under-diluted. This balance is essential for preventing blockages and ensuring efficient transport. The system also incorporates safety features, such as pressure relief valves and emergency stop buttons, to protect the equipment and operators from potential hazards. Overall, the working principle combines mechanical and pneumatic elements to achieve a reliable and efficient conveying process for PFA powder.
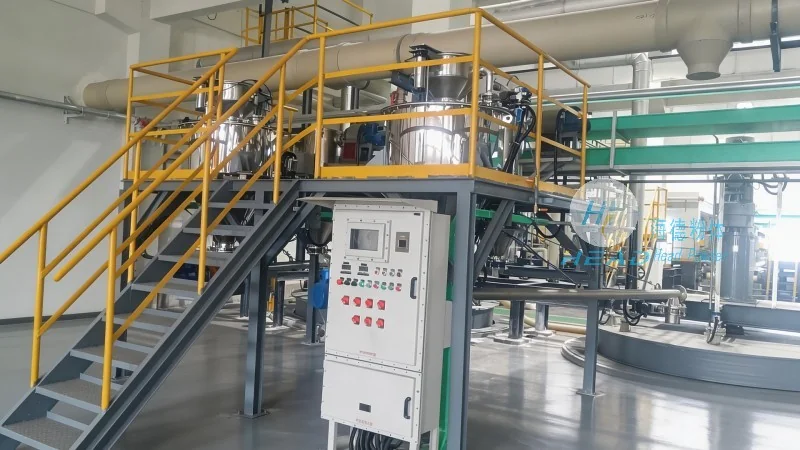
Advantages and Applications of the PFA Powder Conveying System
The PFA powder conveying system offers several advantages that make it suitable for various industrial applications. One of the key advantages is its ability to handle PFA powder with minimal contamination and loss, which is critical for maintaining the quality of the material. The system is also designed to be energy-efficient, with adjustable speed controls that optimize power usage. Additionally, the system is easy to maintain and clean, with smooth surfaces that prevent material buildup. The PFA powder conveying system is widely used in industries such as electronics, chemical processing, and aerospace, where PFA powder is used for applications like coating, molding, and insulation. The system's reliability and efficiency make it an essential component in these industries, ensuring consistent and high-quality production.