With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design, manufacturing, and implementation of advanced dilute phase powder conveying systems. These systems are engineered to efficiently transport bulk powders over long distances with minimal pressure drop and high reliability. The company’s headquarters is located in Shandong, China, where a team of experienced engineers and technicians develops cutting-edge solutions tailored to diverse industrial applications.
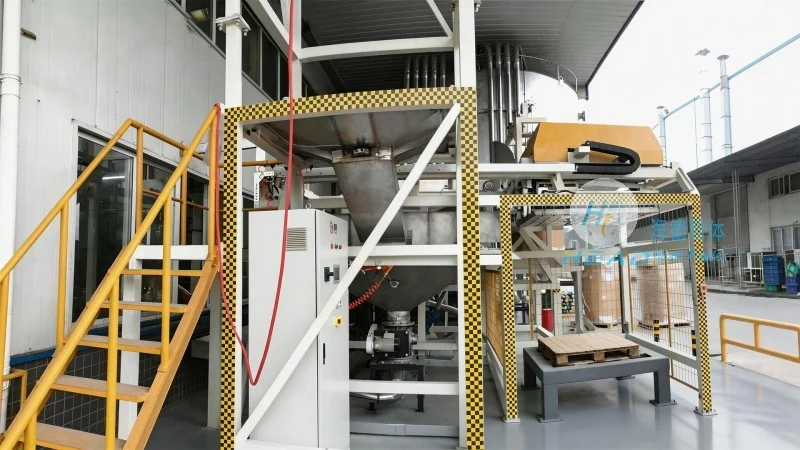
A dilute phase powder conveying system typically consists of several core components that work in tandem to ensure smooth material transport. The primary elements include a high-pressure blower or compressor, a hopper for powder storage, a pipeline network, and a control system. The blower generates the necessary airflow to suspend the powder particles, while the hopper provides a controlled feed of material. The pipeline, often made of corrosion-resistant materials such as stainless steel or PVC, ensures the material is conveyed efficiently without clogging. The control system monitors and adjusts the airflow and pressure to maintain optimal conveying conditions.
The operation of a dilute phase powder conveying system follows a systematic process that begins with the preparation of the powder feed. The material is first loaded into the hopper, where it is stored until needed. The control system then activates the blower, which draws air from the surrounding environment and compresses it to a high pressure. This pressurized air is then introduced into the pipeline, creating a flow that carries the powder particles in a suspended state. As the air travels through the pipeline, it transports the powder to the destination point, such as a silo, storage tank, or processing unit. The system maintains a consistent flow rate by regulating the blower speed and pressure, ensuring that the powder is delivered without loss or degradation.
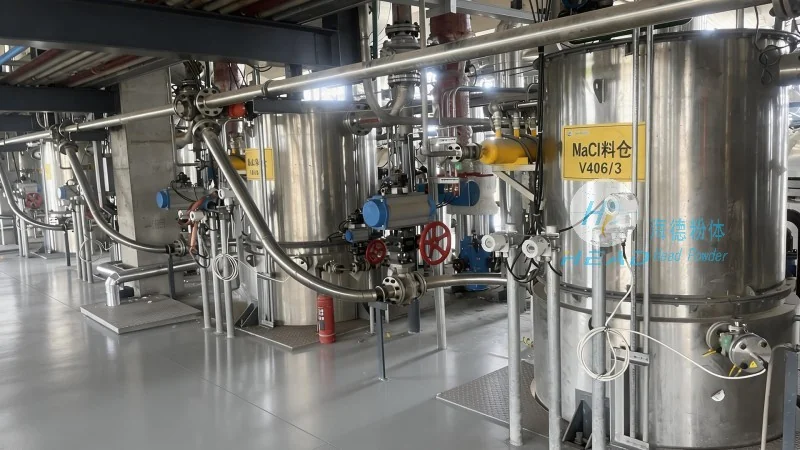
The fundamental working principle of a dilute phase powder conveying system is based on the concept of air suspension. When the air velocity within the pipeline exceeds the terminal velocity of the powder particles, the particles are lifted and carried by the airflow. This suspension prevents the powder from settling or clogging the pipeline, which is a common issue in dense phase conveying systems. The pressure drop across the system is a critical factor, as it determines the energy required to transport the material. By optimizing the pipeline diameter, length, and material properties, the system minimizes pressure drop while maintaining efficient conveying. The control system continuously monitors the pressure and adjusts the blower output to maintain a stable pressure drop, ensuring consistent performance.
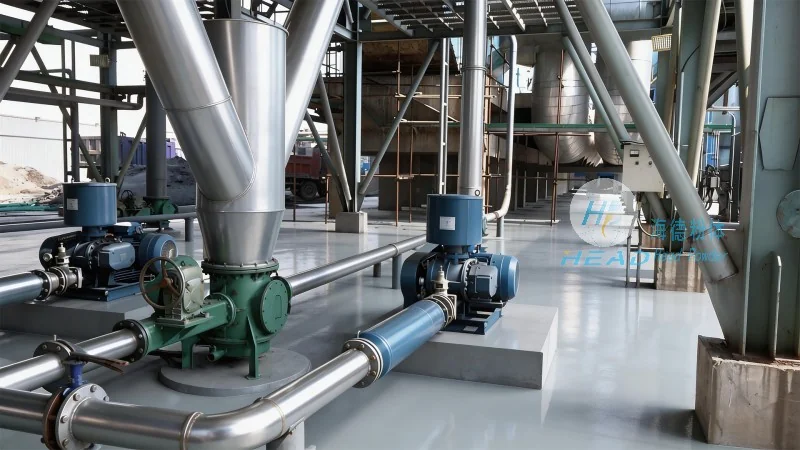
Compared to other powder conveying methods, dilute phase systems offer several advantages that make them suitable for a wide range of applications. One of the key benefits is the ability to transport powders over long distances with minimal equipment. The system requires less maintenance and has lower operational costs due to its simple design and fewer moving parts. Additionally, dilute phase conveying is suitable for a variety of powder types, including fine powders, granules, and bulk materials, without causing degradation or segregation. The system also allows for easy integration with other processing equipment, such as mixers or classifiers, enabling seamless material handling in industrial processes.
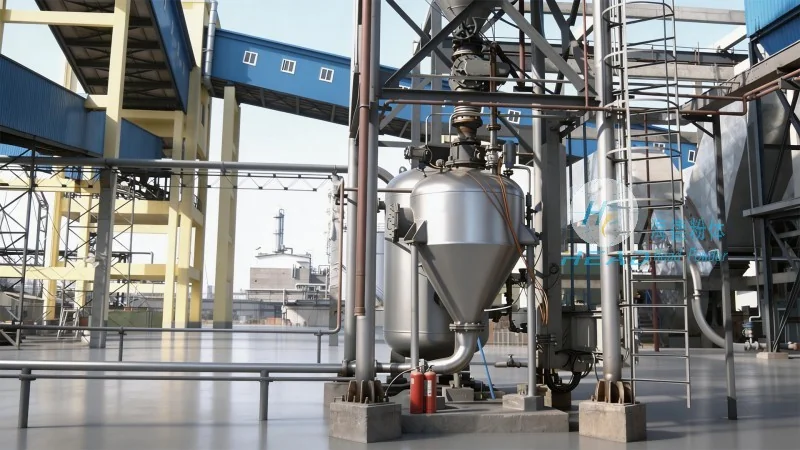
Dilute phase powder conveying systems are widely used in various industrial sectors, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, these systems are used to transport raw materials and finished products with high precision and minimal contamination. The food processing sector utilizes dilute phase conveying for transporting ingredients like flour, sugar, and spices, ensuring hygiene and product quality. Chemical manufacturers rely on these systems to handle reactive powders and hazardous materials safely. In the mining industry, dilute phase conveying is used to transport ore and other bulk materials from mines to processing facilities, improving efficiency and reducing transportation costs.
Shandong HeadPowder Engineering Co., Ltd. remains committed to providing innovative and reliable dilute phase powder conveying solutions to meet the evolving needs of industrial clients. By leveraging advanced engineering and customer-focused design, the company ensures that its systems deliver optimal performance, efficiency, and durability. With a strong presence in Shandong, China, headpowder continues to be a leader in the field of bulk material handling, offering tailored solutions that enhance productivity and safety in various industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top