With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Gravity dust removal powder pneumatic conveying equipment is a specialized system designed to handle fine particulate materials efficiently while ensuring effective dust control. This equipment plays a crucial role in various industrial applications where the transportation of powders and dust removal are critical. The following sections will explore the fundamental principles behind this technology and the specific working scenarios where it excels.
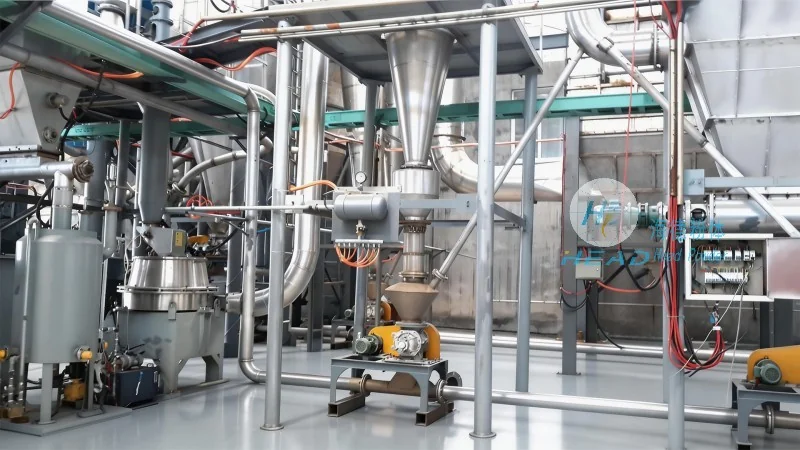
At the core of gravity dust removal powder pneumatic conveying equipment is the integration of gravity-based separation and pneumatic transport mechanisms. The system typically consists of a dust collection unit, a conveying pipeline, and a material discharge point. The primary function is to capture airborne dust particles and simultaneously transport the target powder material from one location to another. This dual functionality makes it particularly valuable in industries such as cement, chemical processing, and food production, where both material handling and air quality management are paramount.
The operation of gravity dust removal powder pneumatic conveying equipment relies on the principles of fluid dynamics and particle separation. The system operates by creating a pressure differential within the conveying pipeline. Air is introduced into the system, often at a controlled velocity, to move the powder particles through the pipeline. Simultaneously, the gravity dust removal component uses a series of chambers or filters to capture larger dust particles that are heavier or have different aerodynamic properties than the target powder. This separation process ensures that only the desired powder is transported while minimizing the release of contaminants into the environment.
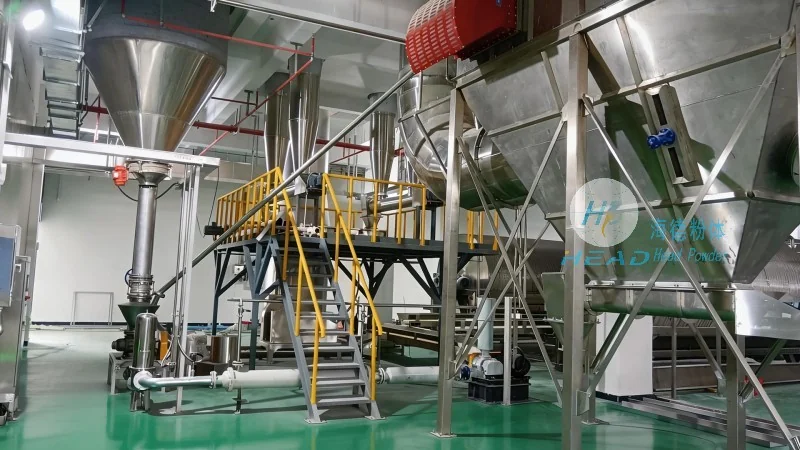
Several critical components work in tandem to ensure the efficient operation of the gravity dust removal powder pneumatic conveying system. The dust collector, often equipped with a hopper and a filter, is responsible for capturing and retaining dust particles. The conveying pipeline, which may include bends, valves, and expansion joints, facilitates the movement of the powder under pressure. The material discharge unit, such as a rotary valve or a surge bin, controls the release of the processed powder to the next stage of the production process. Each component is designed to withstand the specific demands of the material being handled, ensuring durability and reliability in industrial settings.
The effectiveness of gravity dust removal powder pneumatic conveying equipment is highly dependent on the specific working scenarios in which it is deployed. These systems are commonly used in environments where the material to be conveyed is fine and potentially hazardous, such as in cement plants, where the transportation of raw materials and finished products requires both efficiency and safety. In chemical processing facilities, the equipment helps maintain air quality by preventing the release of toxic dust particles while transporting chemicals. Additionally, in food processing industries, the system ensures that powders like flour or sugar are handled hygienically and without contamination, adhering to strict regulatory standards.
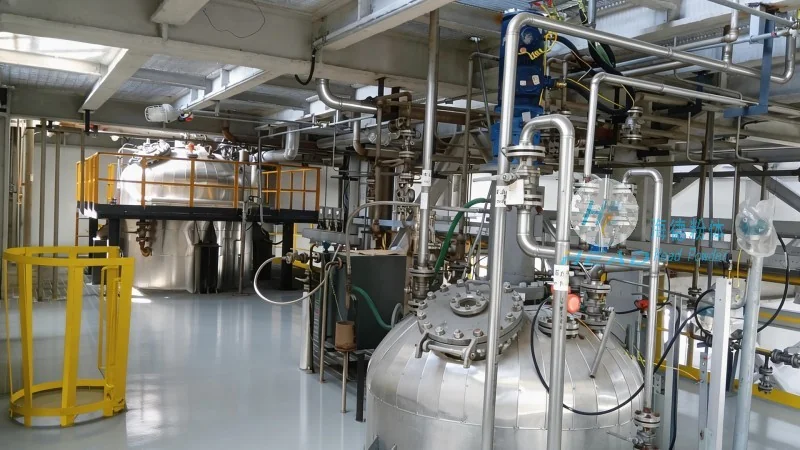
Implementing gravity dust removal powder pneumatic conveying equipment offers several advantages that make it a preferred choice for many industries. One of the key benefits is the ability to handle fine powders without the need for mechanical agitation or high-pressure pumps, which can cause particle degradation or agglomeration. The system also provides excellent dust control, reducing the risk of occupational health hazards and environmental pollution. Furthermore, the modular design of these systems allows for easy integration into existing production lines, minimizing downtime during installation and maintenance. The energy efficiency of pneumatic conveying, when compared to other methods like belt conveyors or bucket elevators, is another significant advantage, contributing to lower operational costs over time.
HeadPowder, the manufacturer of gravity dust removal powder pneumatic conveying equipment, is a leading company based in Shandong, China. With a strong commitment to innovation and quality, HeadPowder specializes in designing and manufacturing advanced material handling solutions tailored to the needs of various industries. The company's products are engineered to meet international standards while providing cost-effective solutions that enhance operational efficiency and safety. HeadPowder's team of experts works closely with clients to understand their specific requirements and develop customized systems that optimize material flow and dust control. The company's headquarters and manufacturing facilities are located in Shandong, providing a solid foundation for delivering reliable and durable equipment to global markets.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top