With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider of industrial conveying solutions, specializes in mineral granular material conveying systems. These systems are engineered to efficiently transport bulk materials such as minerals, ores, and other granular substances in various industrial applications. The equipment is designed with precision to meet the demands of different operational environments, ensuring reliable and consistent material handling.
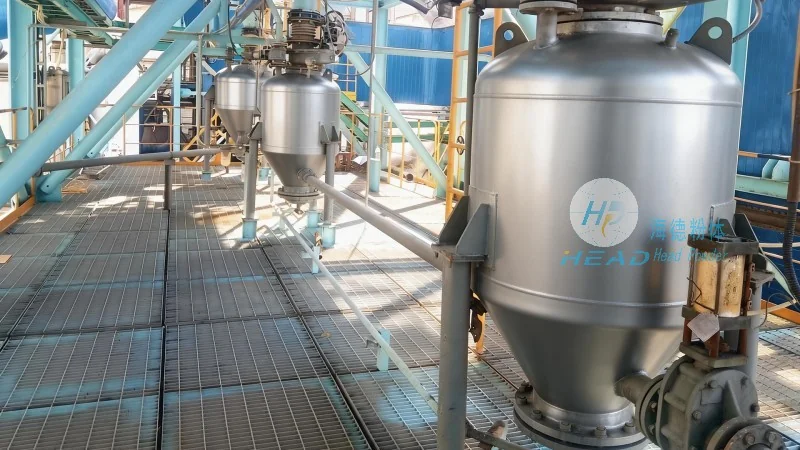
The core principle of mineral granular material conveying systems revolves around the mechanical transfer of bulk materials from one location to another. These systems typically utilize mechanisms like screw conveyors, belt conveyors, or pneumatic conveyors, depending on the specific material characteristics and operational requirements. The design of the equipment ensures that the material is moved with minimal degradation, maintaining its quality and integrity throughout the conveying process. For instance, screw conveyors use rotating screws to push material forward, while belt conveyors rely on friction between the material and the conveyor belt to facilitate movement. Pneumatic conveyors, on the other hand, utilize air pressure to transport materials through pipelines, offering flexibility in layout and material handling.
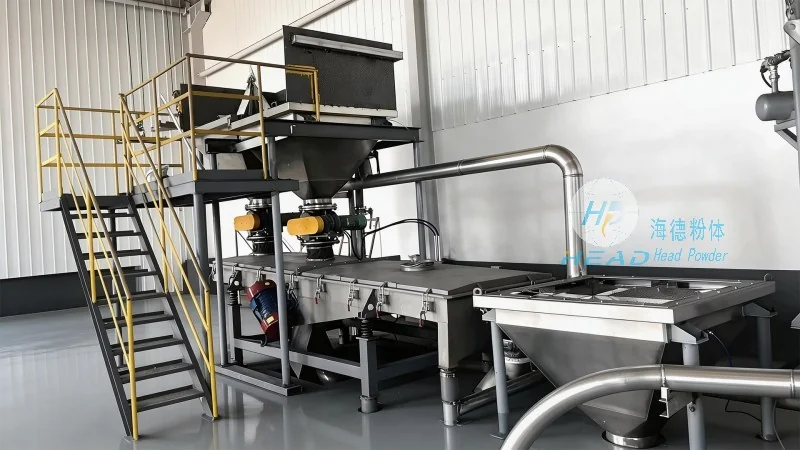
The working scene characteristics of mineral granular material conveying systems are tailored to specific industrial environments. These systems are commonly used in mining, construction, and manufacturing industries where bulk material handling is essential. The equipment is designed to operate in harsh conditions, such as high temperatures, dust, and moisture, ensuring durability and longevity. In mining operations, for example, these systems are crucial for transporting ore from extraction sites to processing facilities. In construction sites, they help in moving sand, gravel, and other aggregates to different work areas. The versatility of these systems allows them to adapt to various operational needs, making them indispensable in modern industrial settings.
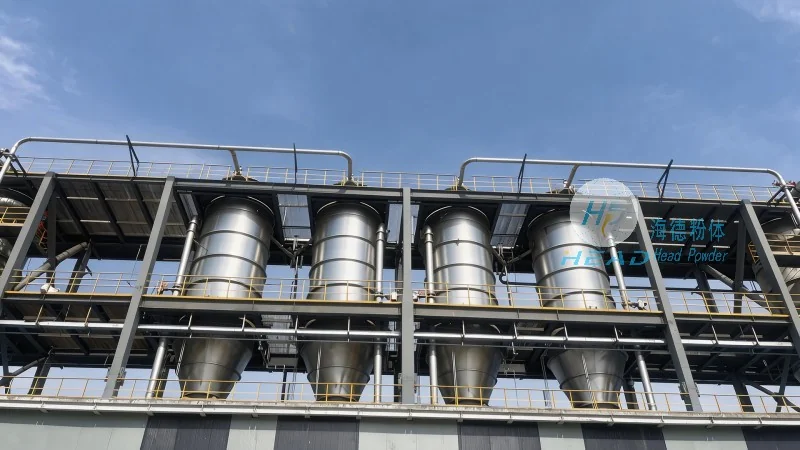
Mineral granular material conveying systems offer several technical advantages that enhance operational efficiency. The use of advanced materials and engineering designs minimizes energy consumption while maximizing material throughput. The systems are equipped with features like variable speed controls, which allow for precise adjustment of conveying rates based on the material flow requirements. Additionally, the integration of sensors and monitoring systems enables real-time tracking of material levels and system performance, facilitating proactive maintenance and reducing downtime. The compact design of many modern conveying systems also optimizes space utilization, making them suitable for both large-scale and small-scale industrial applications.
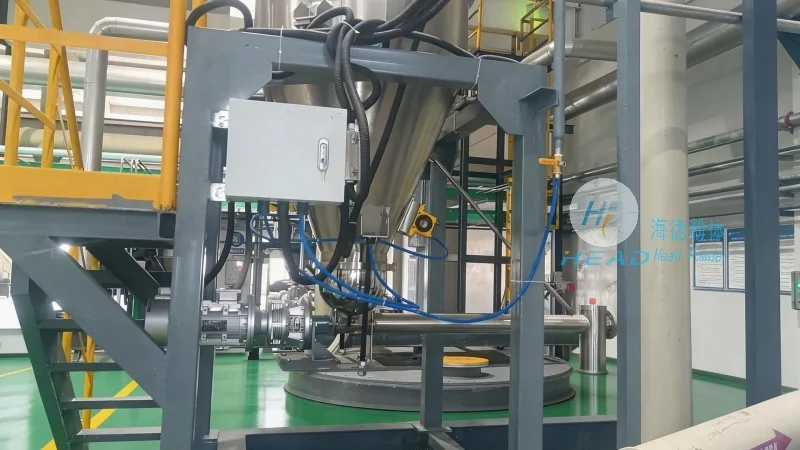
HeadPowder's mineral granular material conveying systems have been successfully implemented in a wide range of applications. In the mining industry, these systems have improved the efficiency of ore transportation, reducing the time and cost associated with material handling. In the construction sector, they have streamlined the supply chain by ensuring a consistent flow of aggregates to building sites. The systems also play a vital role in the chemical and food processing industries, where the handling of granular materials requires strict adherence to hygiene and safety standards. By providing reliable and efficient conveying solutions, HeadPowder contributes to the overall productivity and sustainability of industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top